DrSharpe Health
Explore our certified medical-grade face masks, respirators, and specialty healthcare protective solutions, manufactured to the highest global biological barrier standards.
In modern healthcare systems, biosafety is of paramount importance. Medical gloves (guantes médicos) and advanced respiratory protection stand as the primary physical barriers shielding clinical personnel and patients from cross-contamination, blood-borne pathogens, and dangerous chemical agents. As a premier global supplier, Zhejiang DrSharpe Health Co., Ltd. delivers robust, end-to-end protective solutions designed for hospitals, surgical units, laboratory settings, and specialized industrial sectors worldwide.
This industry analysis is designed to provide procurement officers, hospital networks, and pharmaceutical operations with practical, verifiable facts concerning raw material extraction, manufacturing technology, international regulatory benchmarks, and automated supply chains. True compliance is not merely about holding a certificate; it is about guaranteeing zero defect rates at scale.
Ensuring an Acceptable Quality Level (AQL) of 1.5 or lower for examination-grade gloves and 0.65 for surgical-grade requirements, preventing micro-perforations.
Advancing clean-compounded nitrile and latex-free medical formulations that eliminate Type I allergic reactions while retaining high tensile strength.
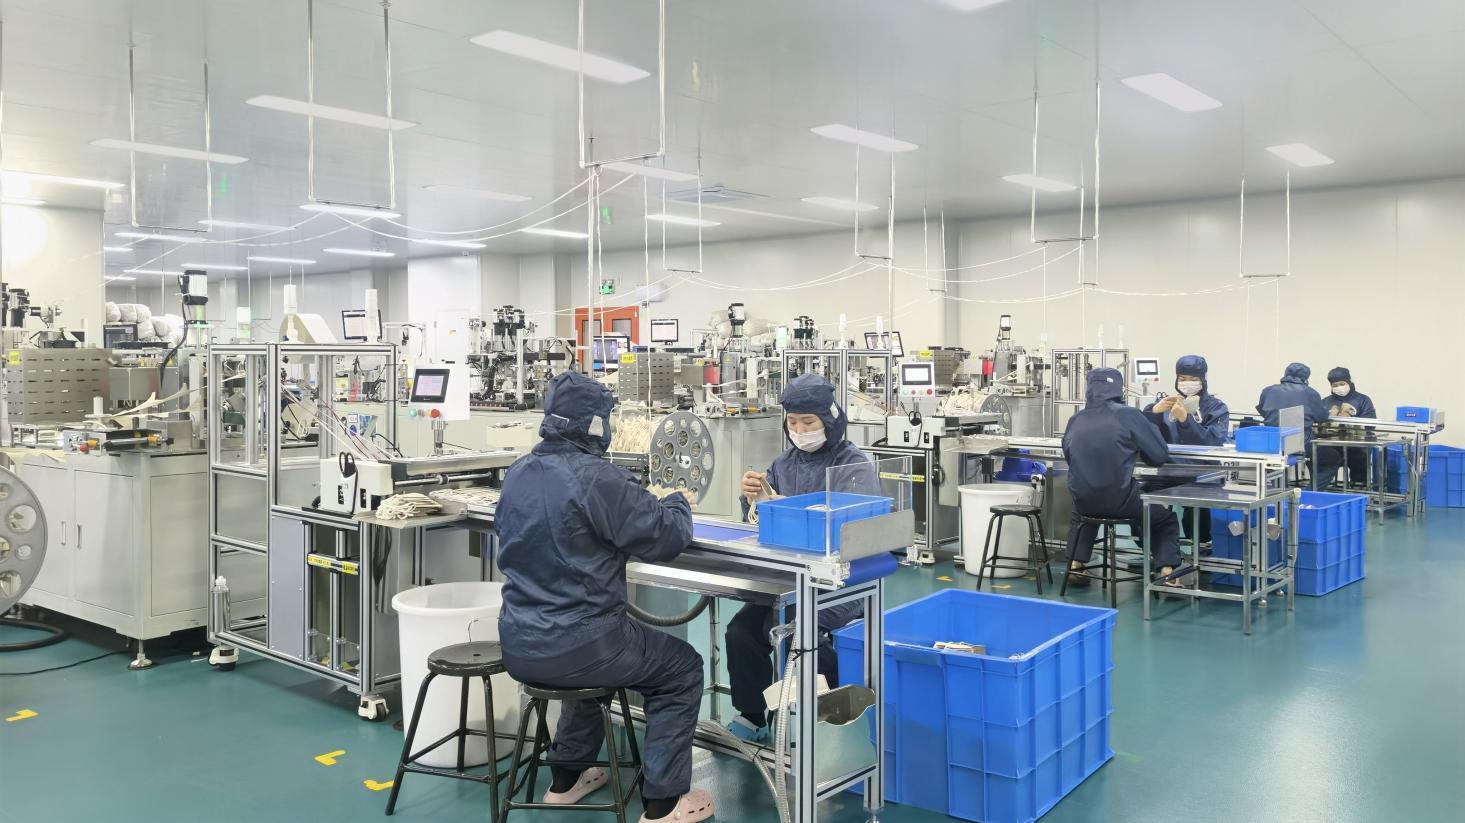
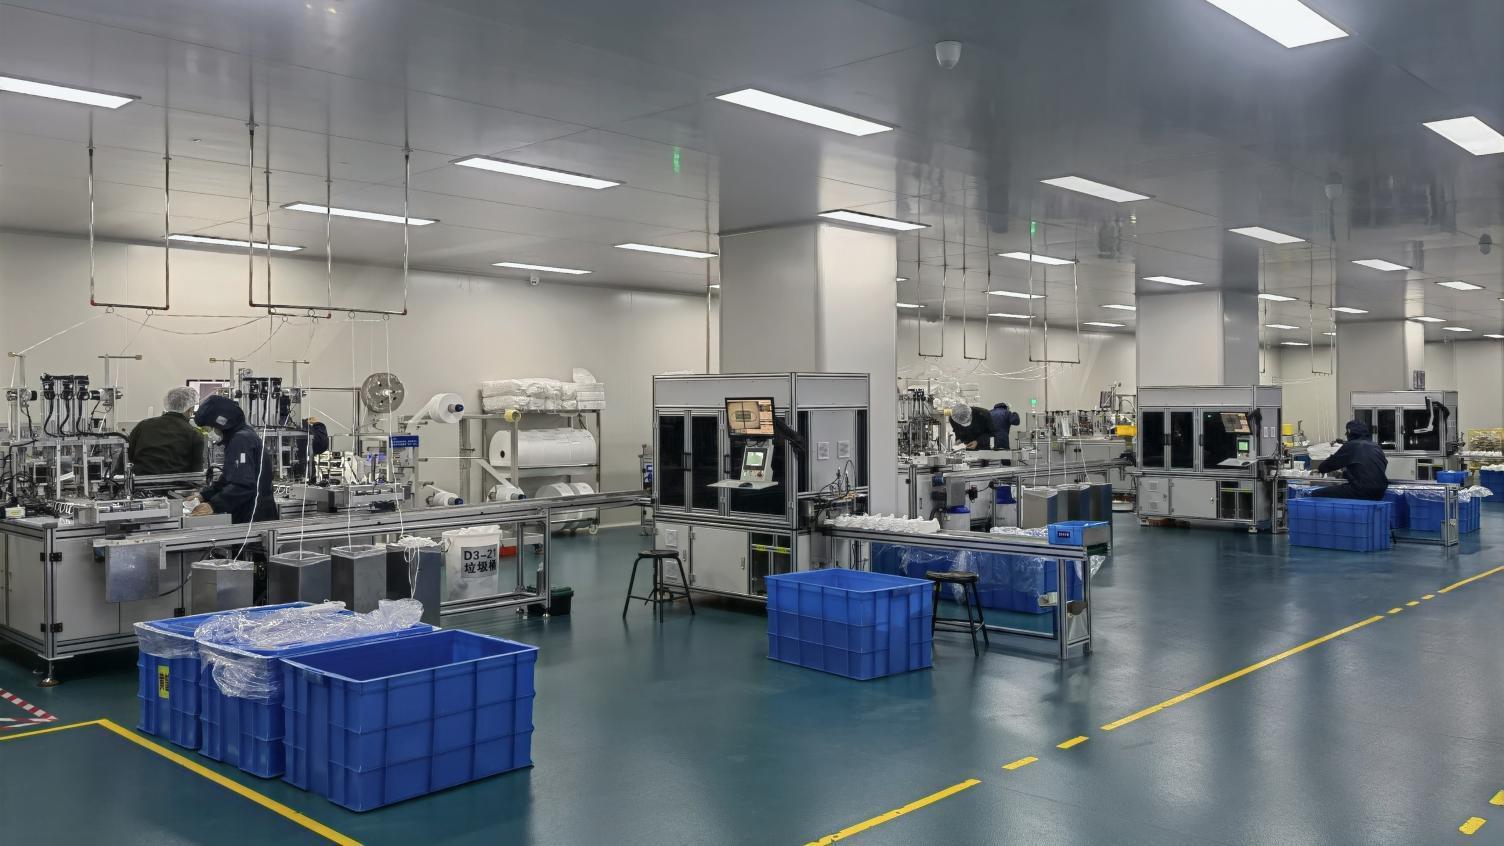
Zhejiang-based high-speed production plants minimizing manual touchpoints and maximizing precision, ensuring stable monthly delivery targets.
China's Yangtze River Delta region, particularly Zhejiang Province, has evolved into the world's most advanced manufacturing corridor for medical devices, non-woven materials, and personal protective equipment. This success is rooted in structural efficiencies that benefit global B2B buyers:
| Manufacturing Dimension | Technical Feature | Strategic Advantage for Global Buyers |
|---|---|---|
| Supply Chain Integration | Proximity to raw polymer facilities, non-woven meltblown plants, and automated packaging manufacturers. | Shortened lead times, reduced shipping-in-transit expenses, and minimized supply disruption risks. |
| Next-Gen Automation | Continuous dipping lines, AI inspection systems, and fully automatic mask and packaging systems. | Exceptional consistency, reduction in physical human contamination, and lowering of baseline per-unit manufacturing costs. |
| Regulatory Readiness | Pre-validated QA systems conforming to FDA 510(k), CE EN 455, EN 14683 Type IIR, and US EUA protocols. | Smooth customs clearance and fast-track acceptance in critical healthcare, dental, and laboratory networks. |
Furthermore, local energy stability and robust ocean-freight hubs in Ningbo and Shanghai guarantee that volume contract shipments are dispatched reliably. Global distributors and healthcare networks benefit from a partner that is insulated from regional material shortages and unpredictable pricing spikes.
The global demand for high-tier medical gloves and facial protection continues to expand beyond conventional clinical environments. Driven by post-pandemic awareness and rising biosafety protocols in emerging markets, several technological trends are shaping the future of safety materials:
Nitrile examination gloves continue to gain market share over natural rubber latex. Medical organizations prefer nitrile because it offers superior chemical resistance to chemotherapy drugs and solvent compounds, alongside eliminating the risk of type I latex hypersensitivity.
Modern dipping lines produce gloves with thin-wall technology that matches the tactile sensitivity and tensile properties of latex. This is critical for surgeons and dental specialists who require tactile feedback during precision procedures.
Top suppliers use advanced machine-vision systems to inspect gloves and masks on the production line, scanning for pinholes, visual defects, or packaging seals to guarantee that every batch meets EN 455 and EN 14683 criteria.
Biological and chemical hazards differ significantly depending on the target environment. Selecting the correct personal protective equipment ensures both regulatory compliance and staff safety. Below are the key applications where our high-performance gloves, masks, and respiratory canisters are deployed:
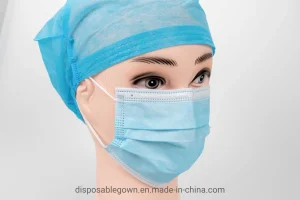
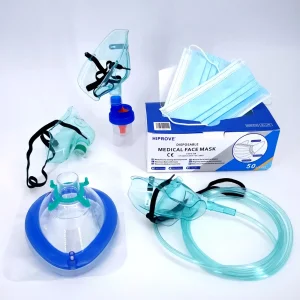
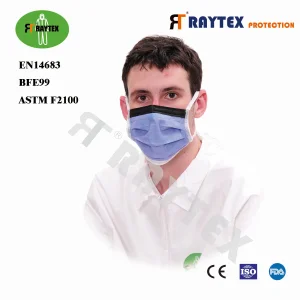
Hospitals and surgical theaters require top-tier sterility, high resistance to blood-borne pathogens, and reliable tear strength. Our EN14683 Type IIR surgical masks and high-barrier surgical gloves provide the necessary protection during intensive surgeries and high-exposure ward duties.
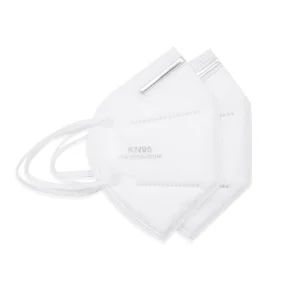
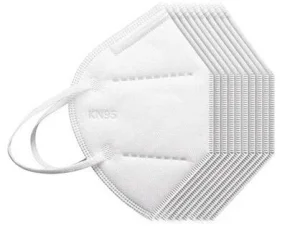
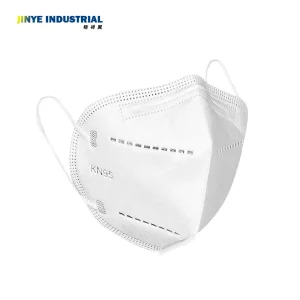
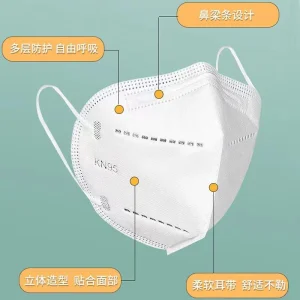
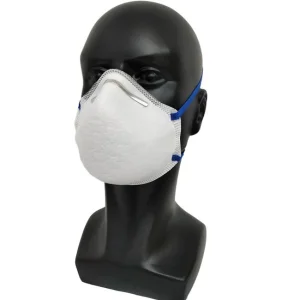
Dental professionals face continuous exposure to aerosolized pathogens, saliva, and fine abrasive dust. Our 3D fold face masks (KN95/N95) combined with comfortable, texturized medical-grade nitrile gloves offer the puncture resistance and seal protection needed for close-proximity work.
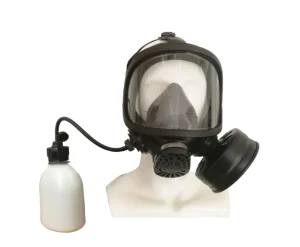
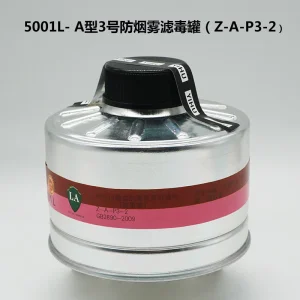
Handling hazardous chemicals, toxic gases, and sensitive biological compounds requires heavy-duty protection. Products like our Full-Face Gas Mask Respirators equipped with activated carbon canisters protect technicians, while clean-packed nitrile gloves protect against chemical splashes.
We are a professional manufacturer and global supplier specializing in disposable medical and healthcare products, offering high-quality face masks, protective solutions, and medical consumables.
With strong manufacturing capabilities, advanced production technology, and strict quality management, Zhejiang DrSharpe Health Co., Ltd. is committed to providing safe, reliable, and comfortable healthcare products for customers worldwide. From raw material selection to final packaging, we strictly control every production process to ensure stable quality and reliable supply. Our products are widely exported to international markets, including the United States, Europe, Japan, Mexico, Germany, and the United Kingdom.
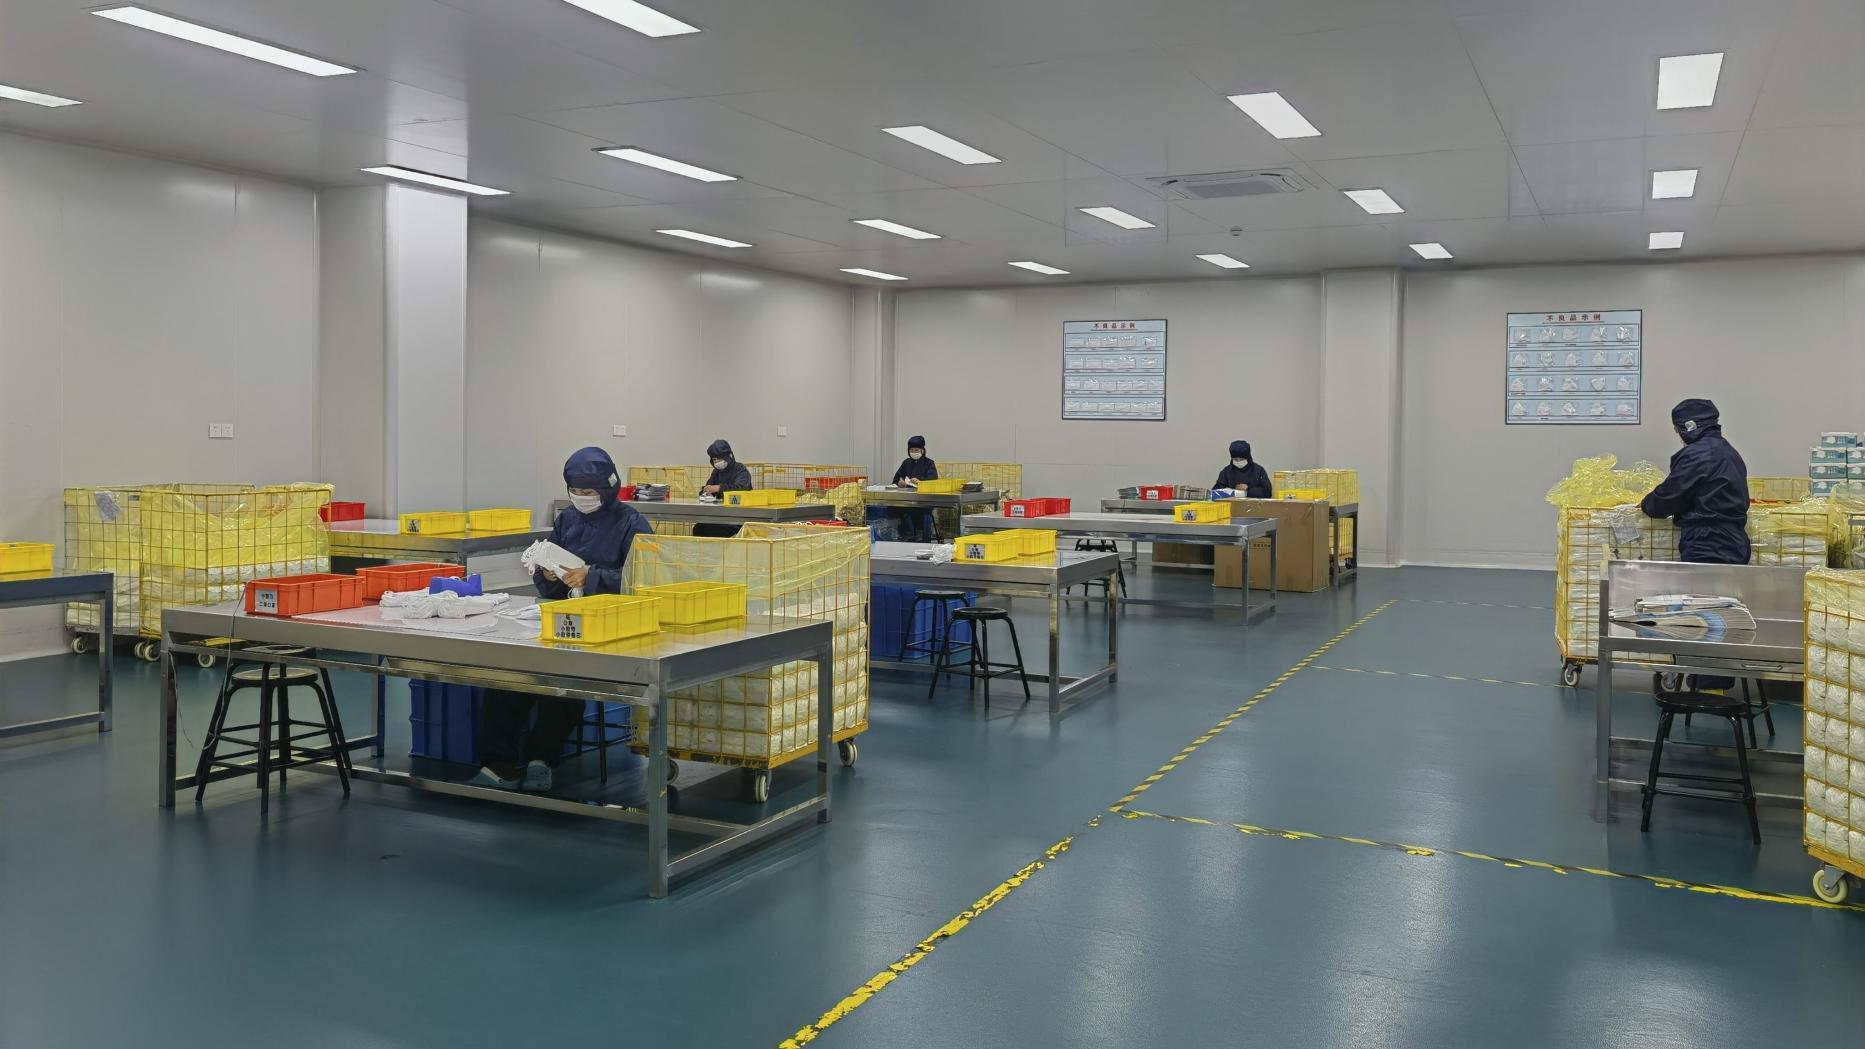
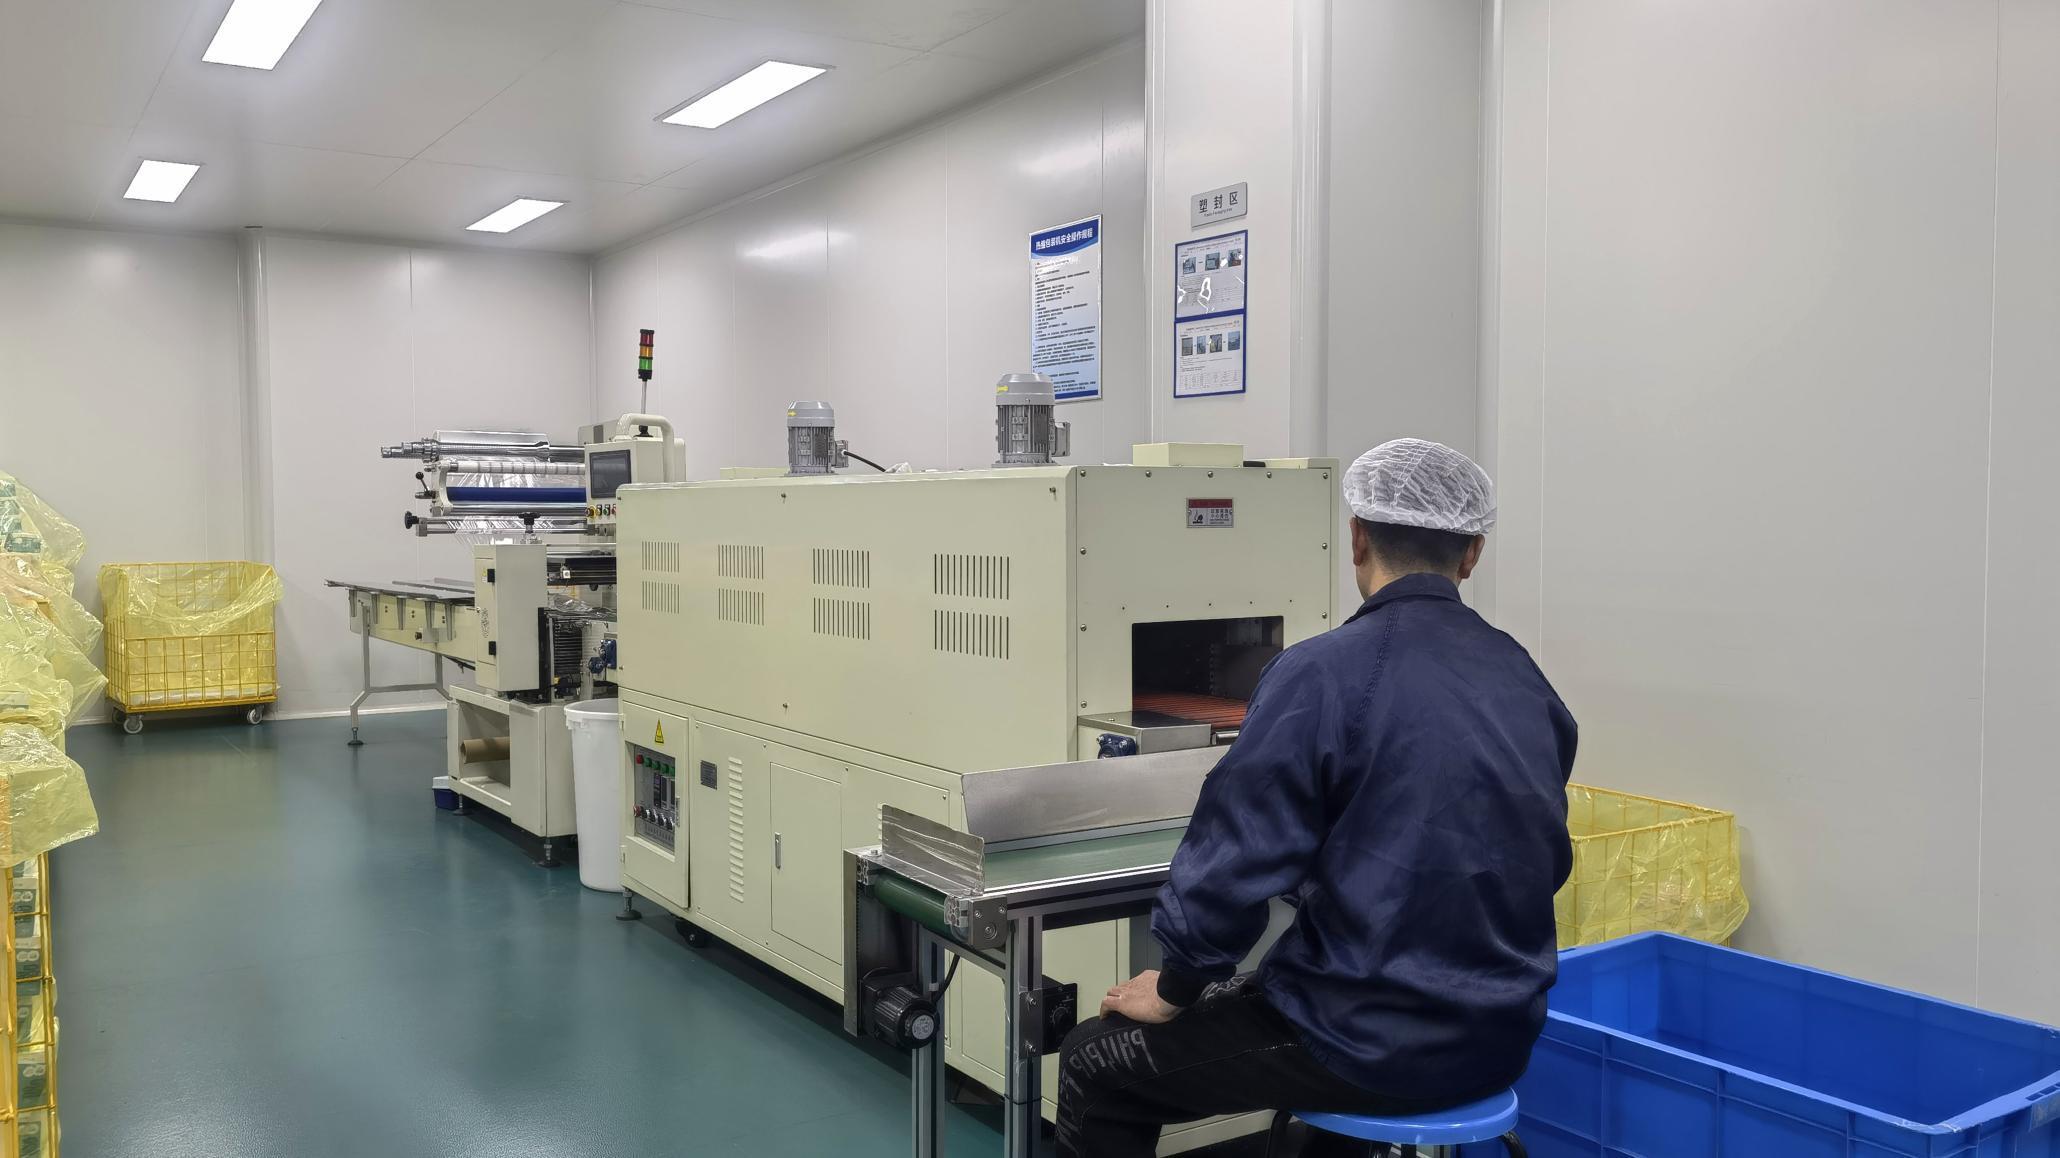
We deploy advanced automated machinery and clean-room packaging infrastructure to ensure medical-grade precision across all product runs.
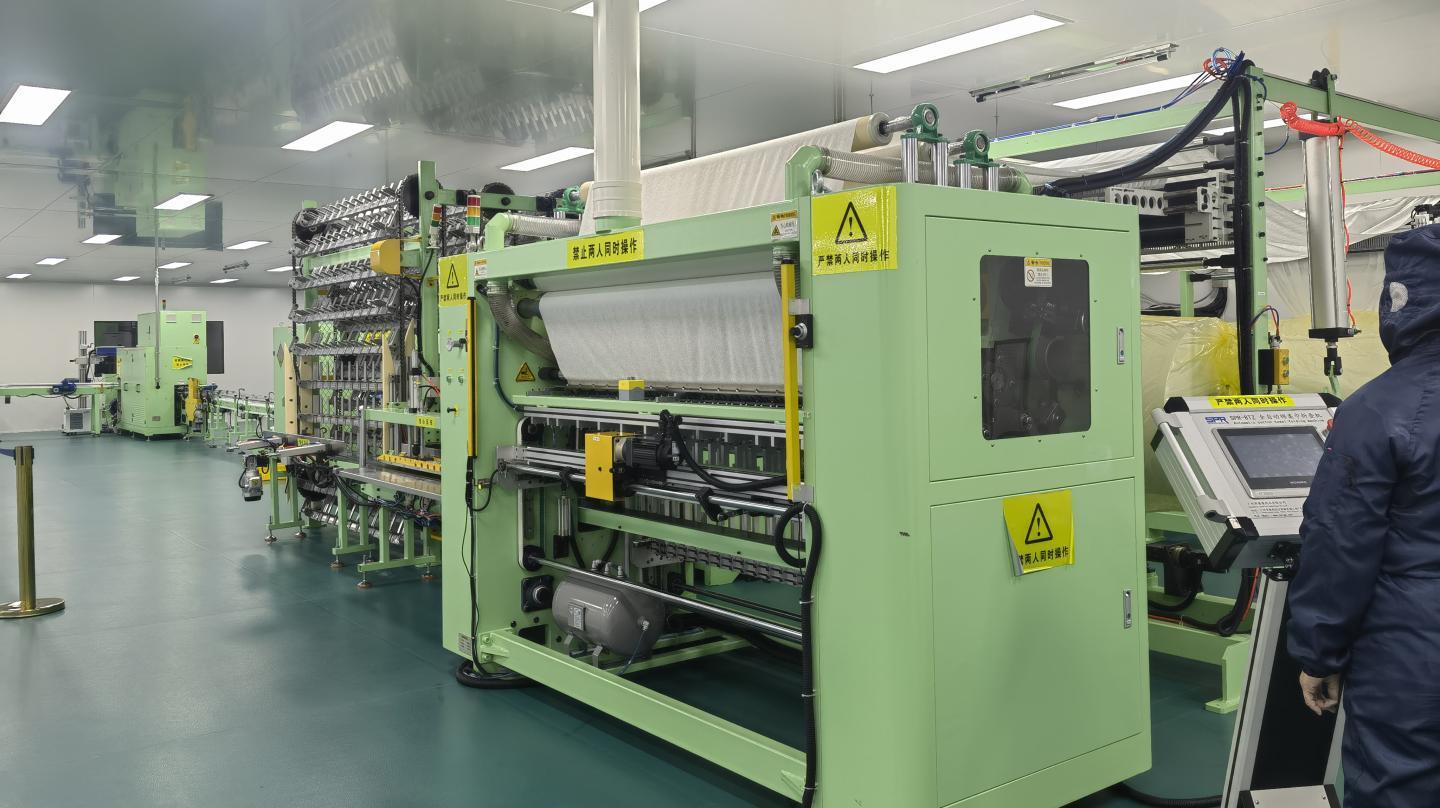
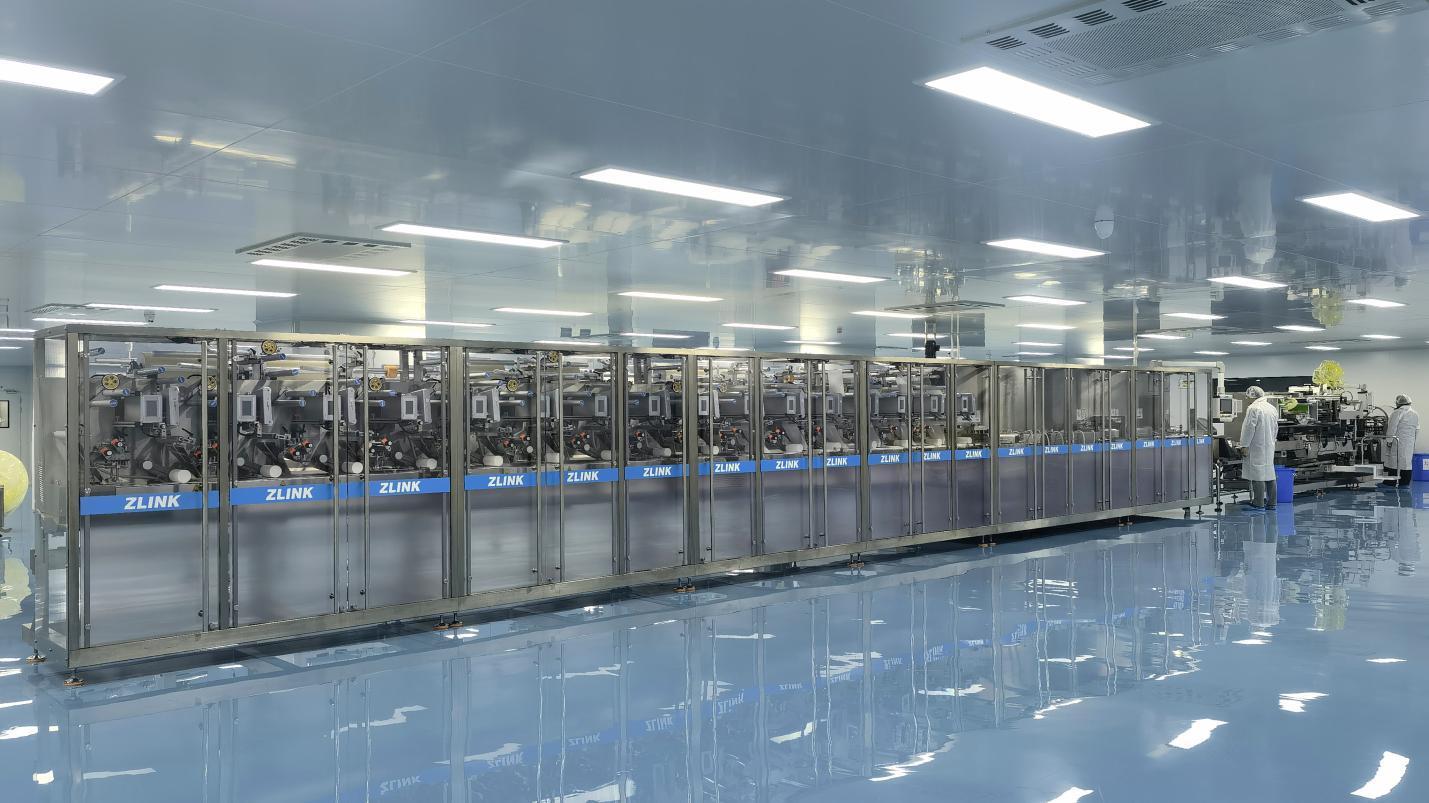
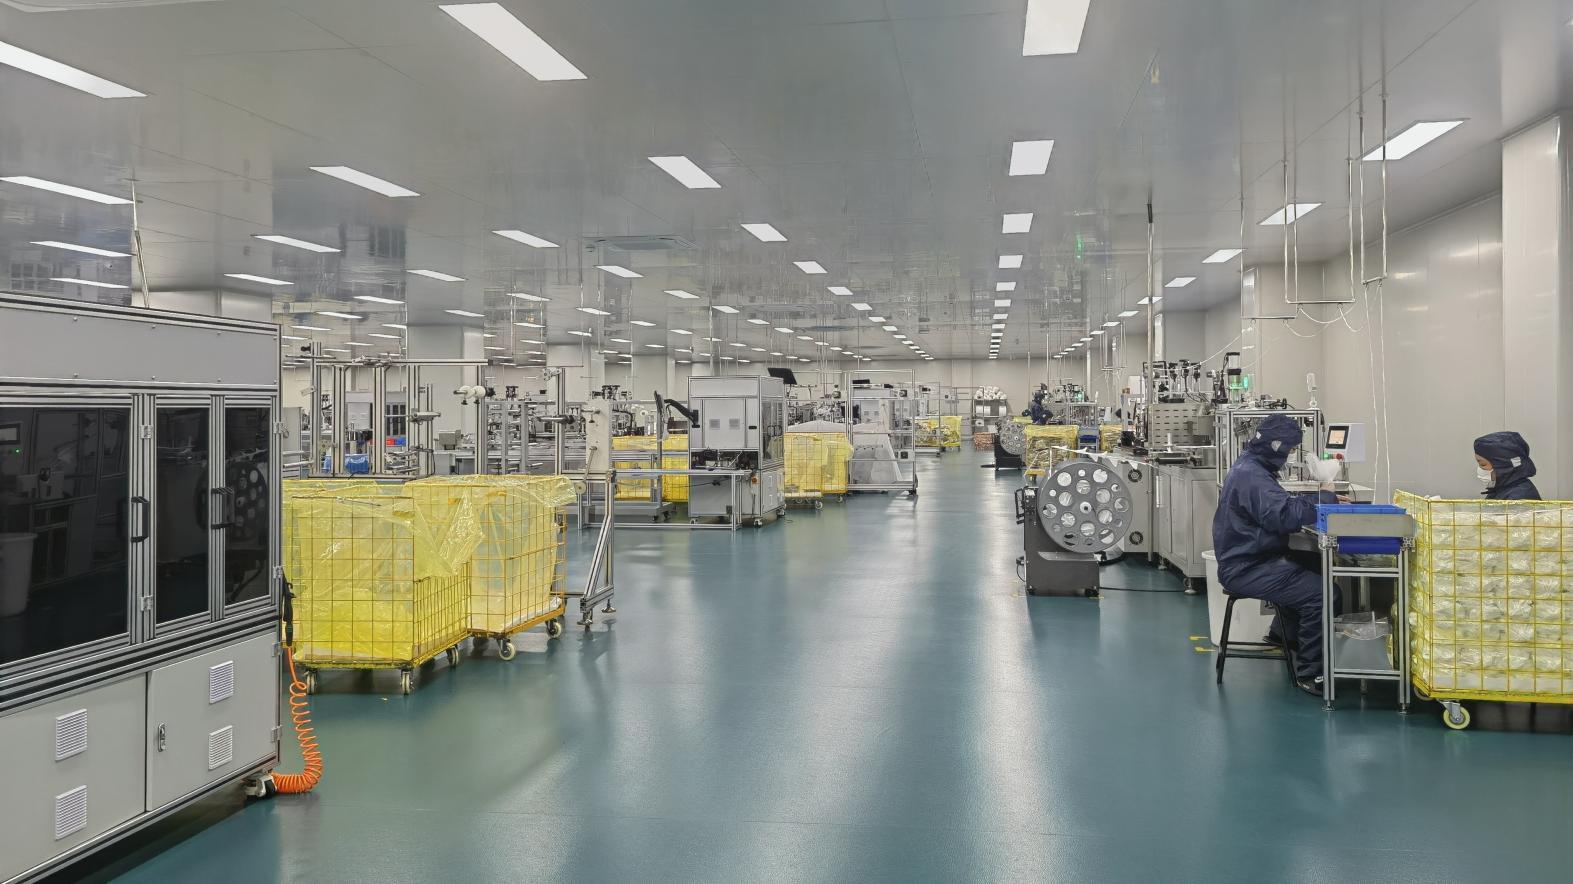
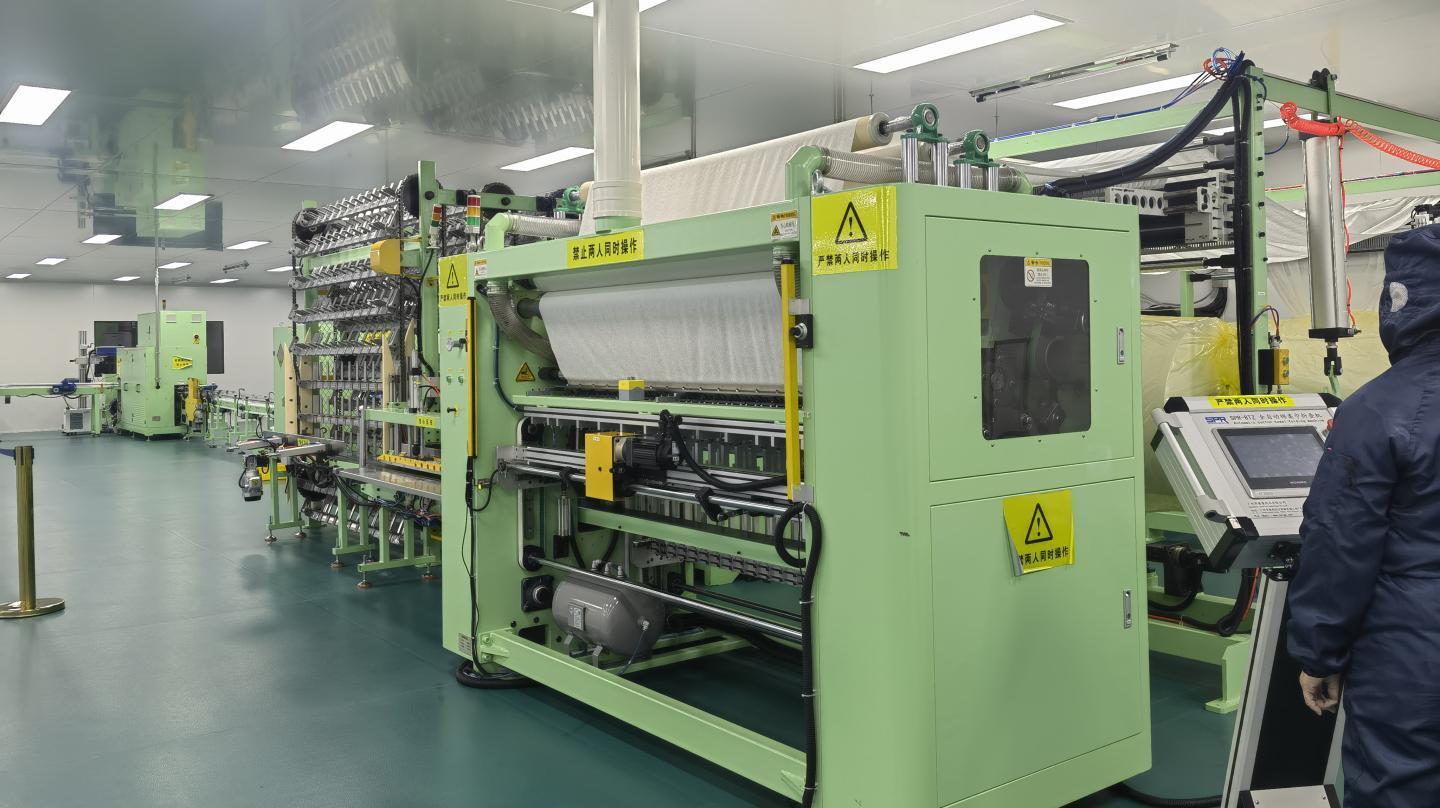
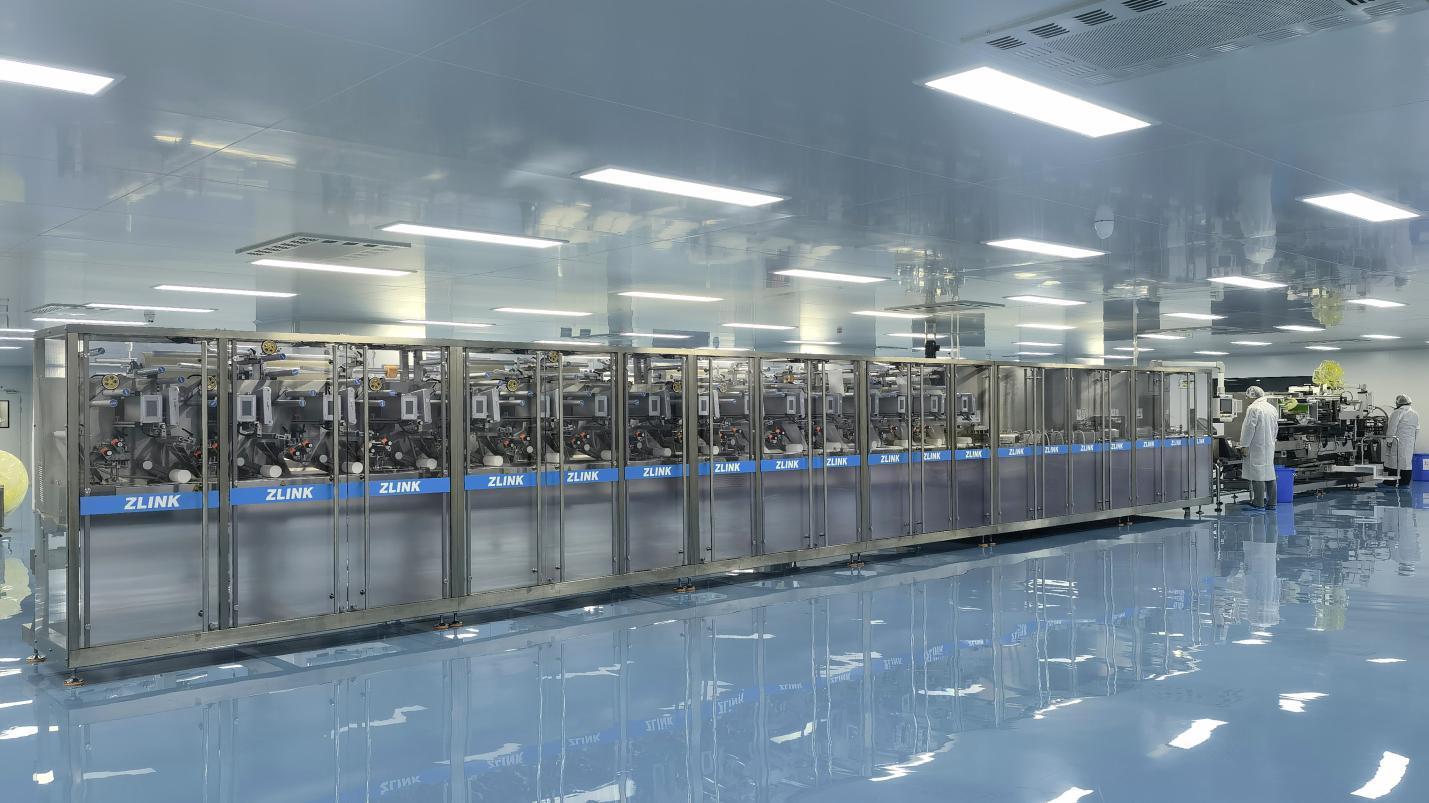
For procurement officers in medical, governmental, and pharmaceutical entities, sourcing protective gear is a complex process. DrSharpe offers custom solutions to help streamline the process and maintain reliable supply chains:
We work with long-term procurement partners to lock in raw material prices. This buffers your operating budget against changes in polypropylene, rubber, and chemical costs, keeping your expenses predictable.
We provide tailormade box and packaging configurations, private labeling options, and custom pack counts (e.g., 50-count retail, 100-count hospital boxes) to fit your market and distribution channels.
We handle documentation, quality certificates, customs clearances, and shipping logistics. Our cargo partners ensure smooth transit to key hubs globally, keeping shipments moving without delay.
Every batch of raw materials is tested for tensile strength, elongation, and filtration efficiency (BFE/PFE ≥ 99%) before entering the assembly floor. Our finished items go through pressure-differential tests, water-penetration tests, and structural inspection to ensure they meet international standards before shipping.
Get authoritative answers on medical glove compositions, compliance, and international safety standards.
Explore our complete catalog of certified masks, respirators, and clinical face covers designed for healthcare settings and industrial applications.