DrSharpe Health
Explore our certifiably manufactured sanitary, respiratory, and safety solutions engineered to maintain operational integrity in professional environments.
Understanding the critical demand for food-grade contact and non-contact thermal tracking systems across international supply chains.
In modern industrial and commercial culinary operations, temperature measurement is no longer a matter of subjective assessment or consumer convenience. It represents a strict regulatory boundary defined by global HACCP (Hazard Analysis Critical Control Point) frameworks, designed to prevent biological hazards and cross-contamination. Consequently, the global procurement of high-accuracy Termómetro de Cocina (kitchen thermometers) has transitioned from standard homeware sourcing to rigorous enterprise-grade engineering contracts.
Today's food service chains, industrial processing plants, and cold-chain logistics operations require massive pipelines of food probes capable of surviving high-humidity, high-heat sanitization cycles while retaining ±0.5°C accuracy over thousands of duty cycles. Leading suppliers have responded by merging medical-grade sanitary materials (such as anti-microbial ABS plastic and surgical SUS304/SUS316 stainless steel) with precision electronic sensors. This crossover highlights a deep synergy between professional personal protective equipment (PPE) manufacturing and precise culinary measurement infrastructure. Both industries share the common goal of protecting public health, preventing bacterial spread, and assuring clean, sterile operational environments.
From a macroeconomic perspective, the market for digital and wireless kitchen thermometers is experiencing rapid growth, driven by tightening food safety regulations in North America, Western Europe, and East Asia. Sourcing agents are shifting away from low-cost, uncertified consumer suppliers to partner with high-capacity B2B manufacturers. These factories must possess certified cleanrooms, robust automated assembly operations, and internationally recognized QA credentials (such as ISO 9001, CE, and FDA compliance). Our capability to deliver both premium food measurement tools and high-efficiency PPE allows industrial partners to consolidate their hygiene and safety procurement under one reliable manufacturer.
For commercial kitchens, documenting internal thermal hold values is legally required. Digital probes provide automatic logging capability to prove systemic elimination of food-borne pathogens (like Salmonella and E. coli).
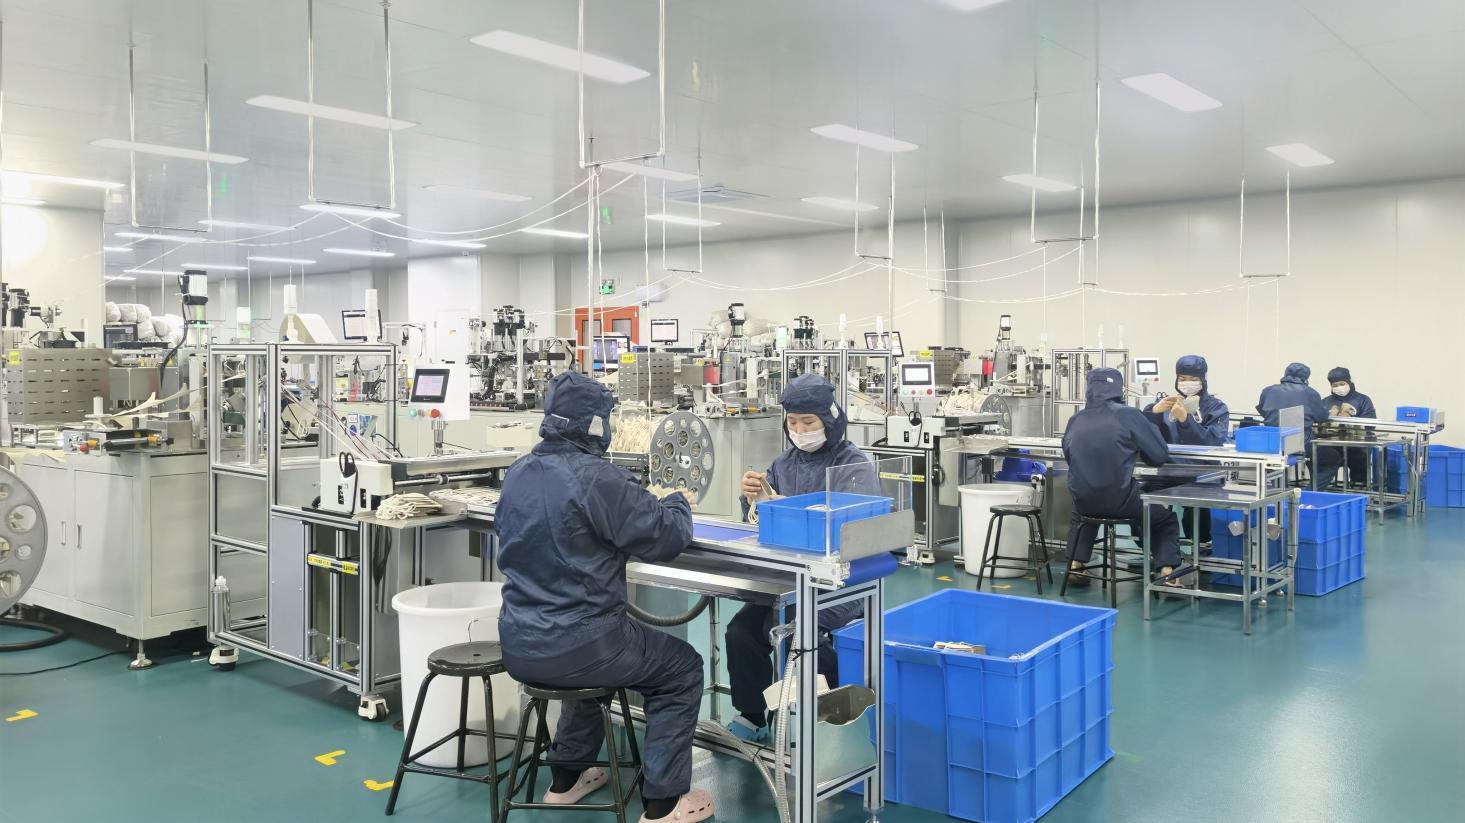
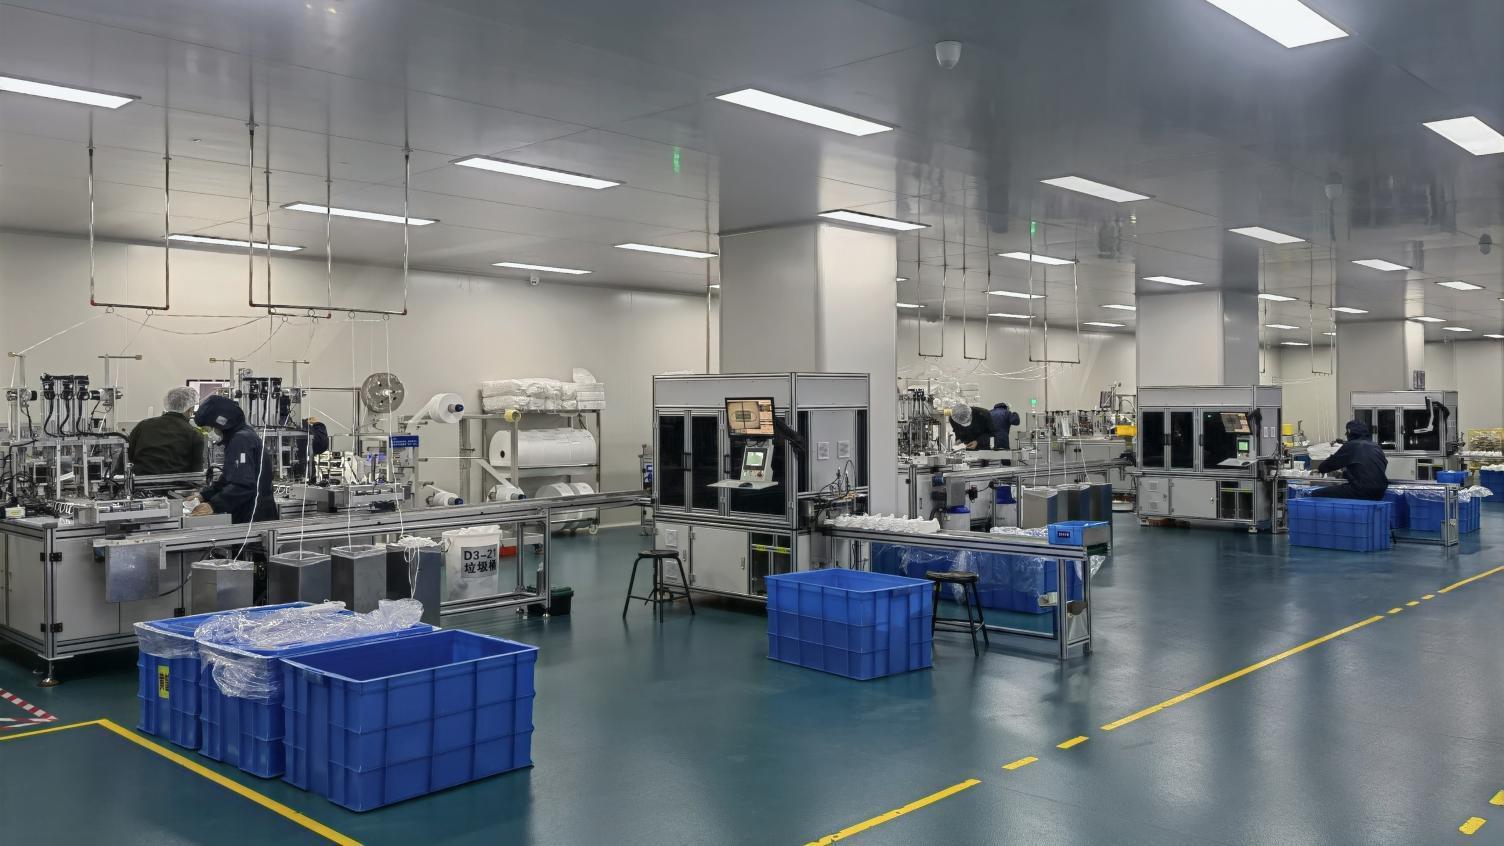
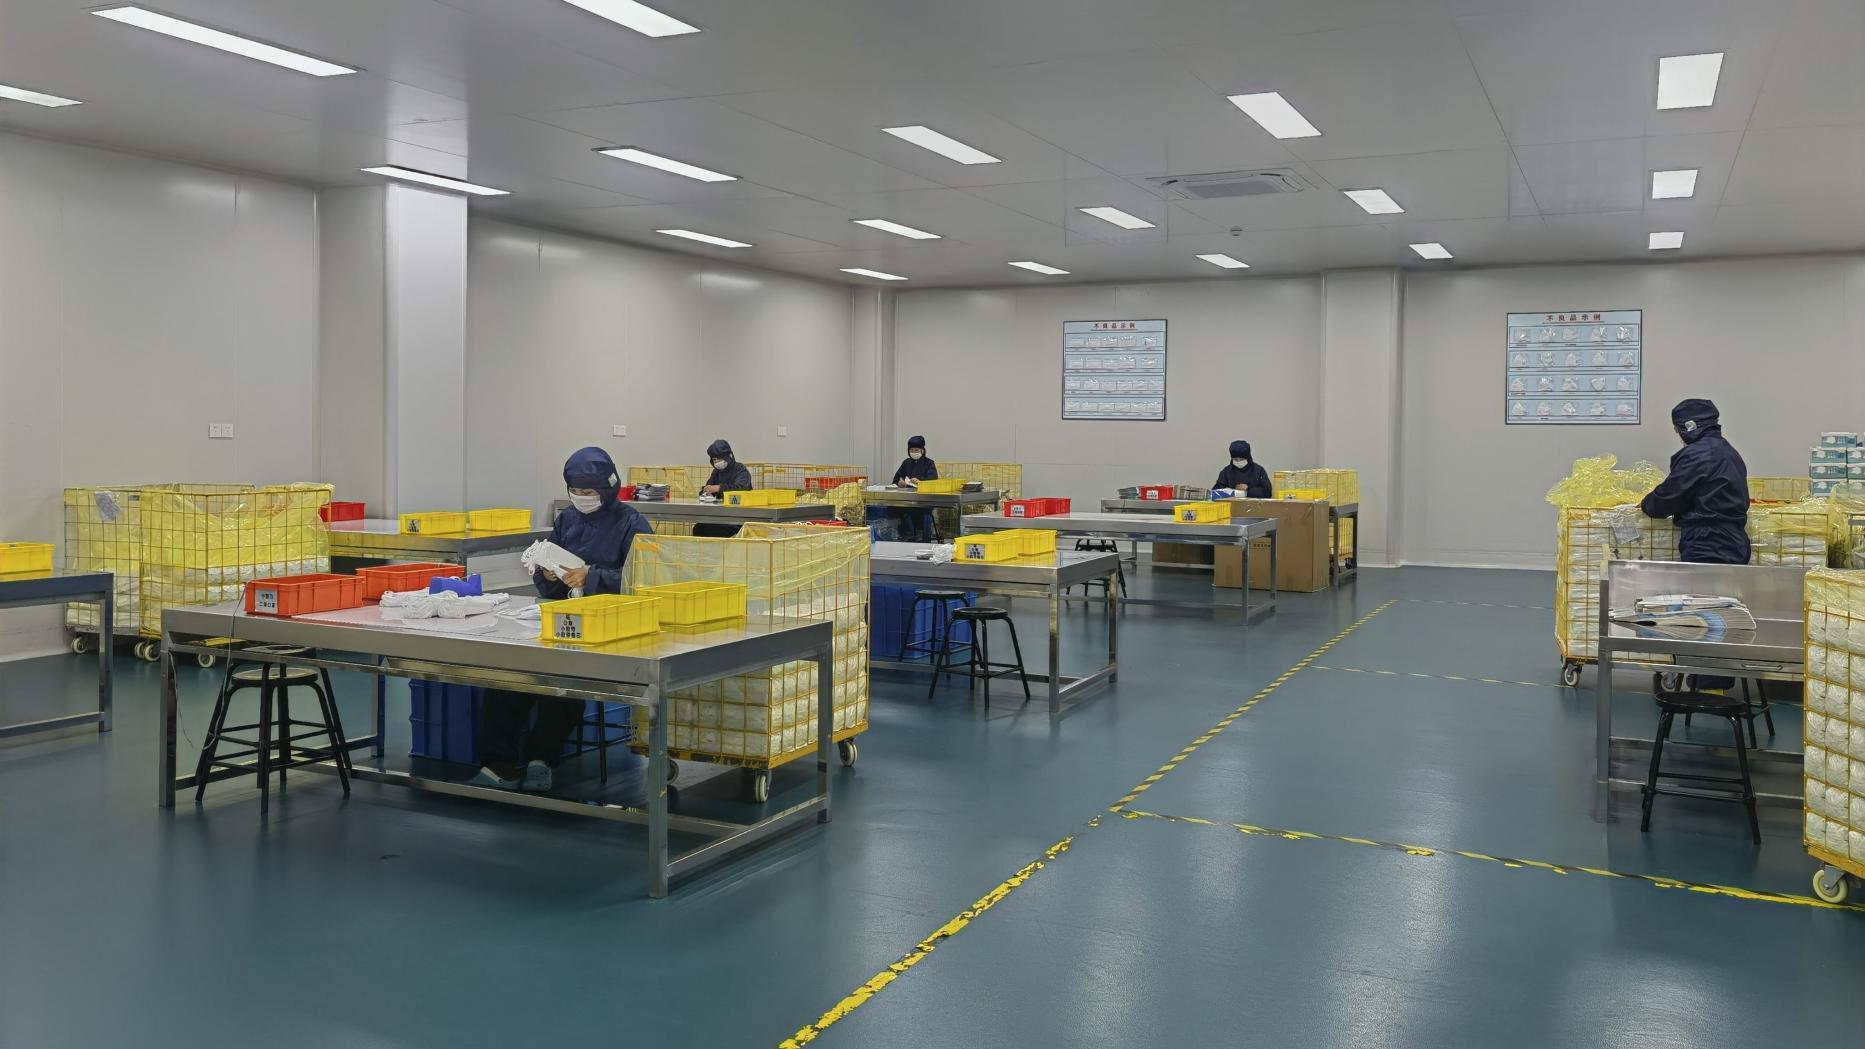
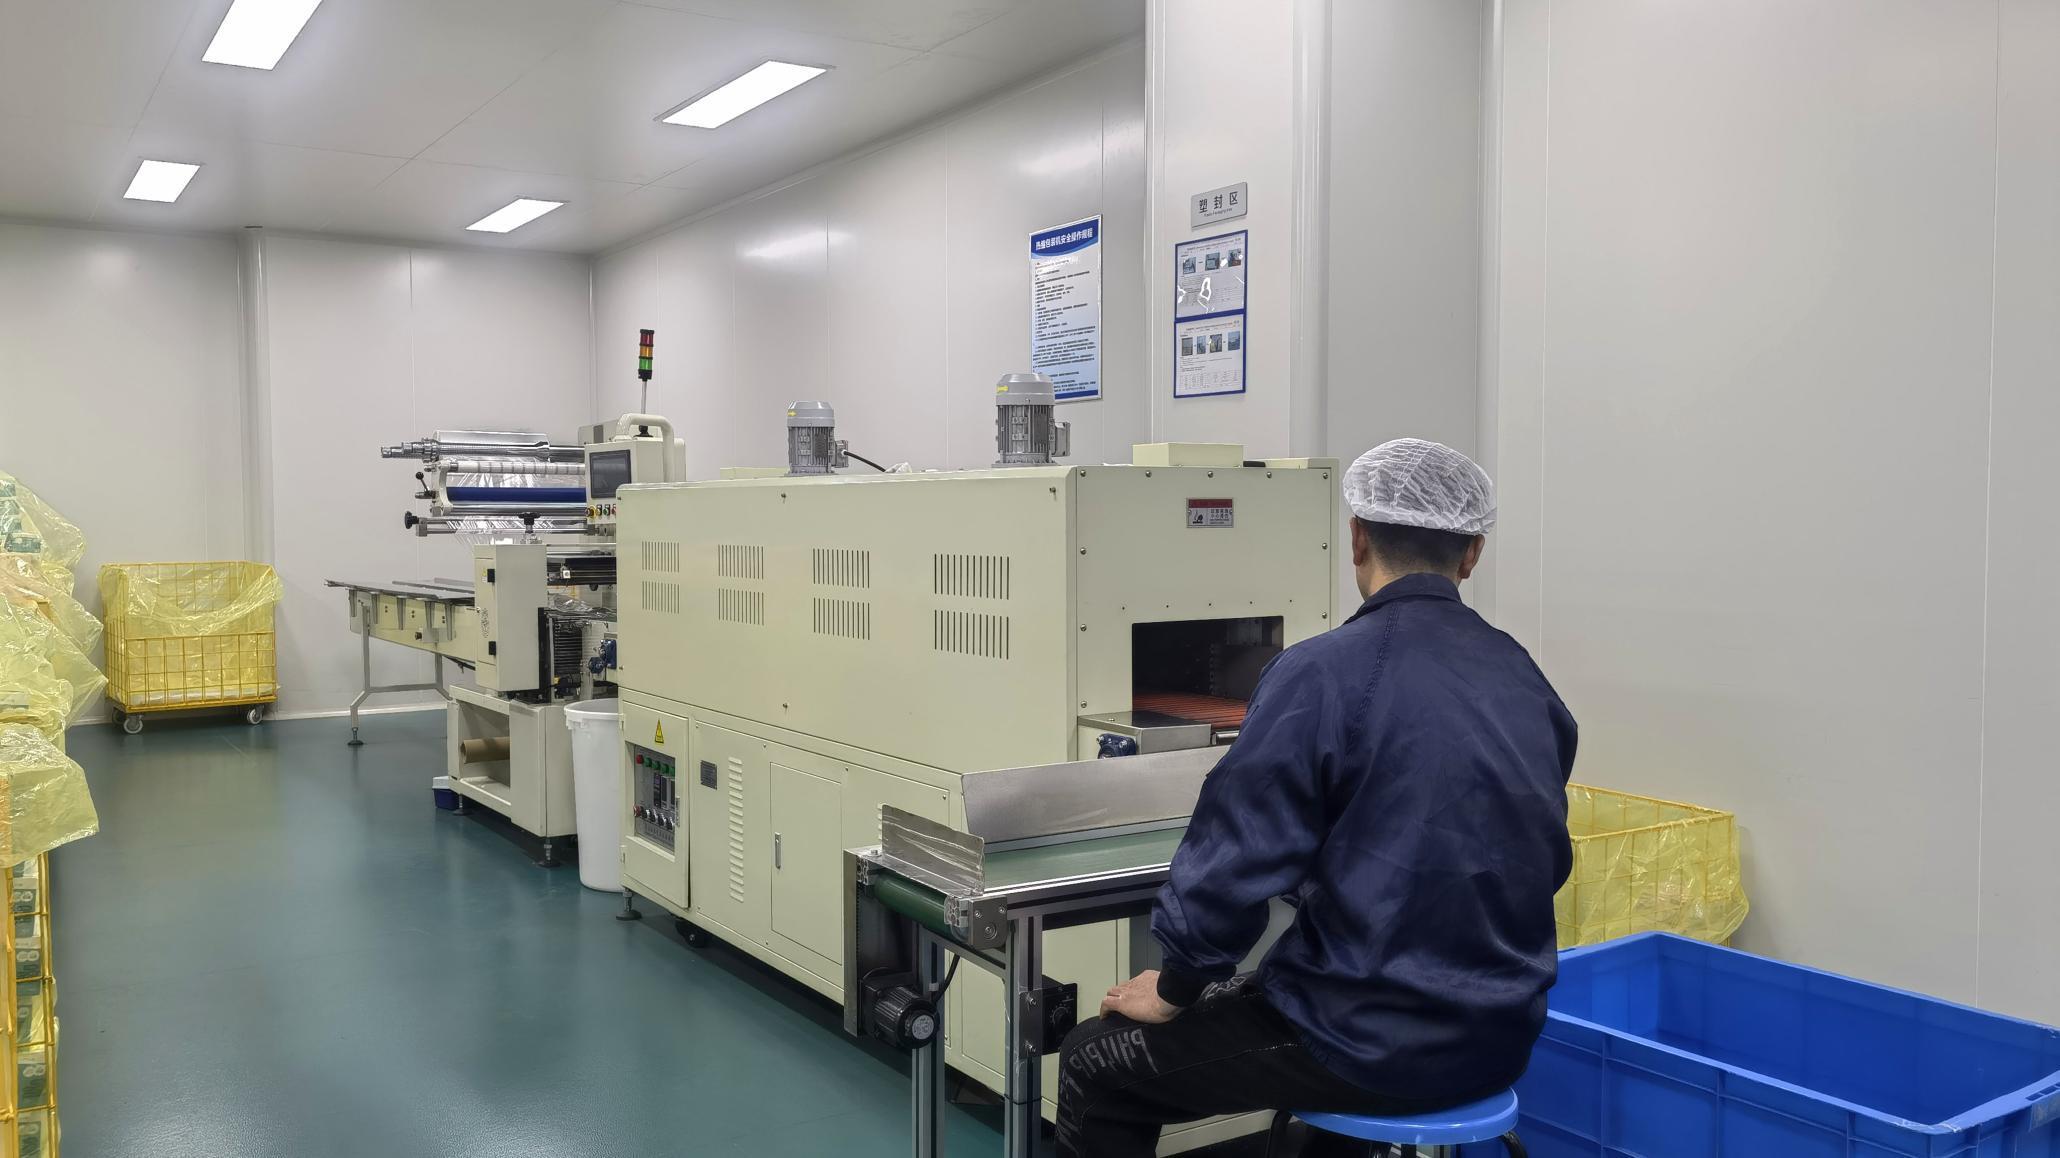
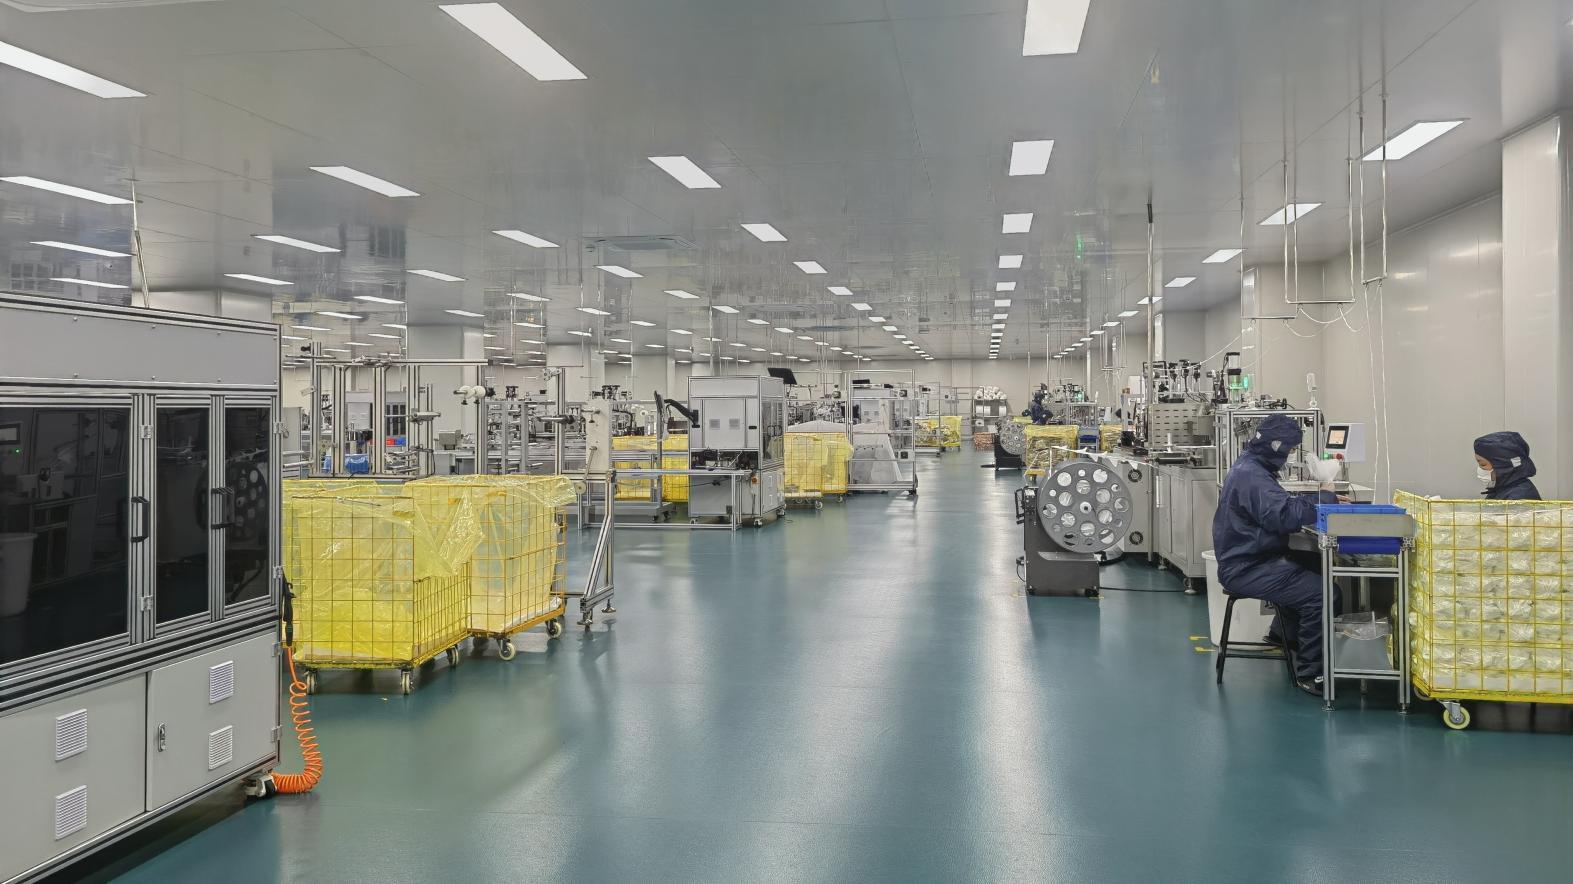
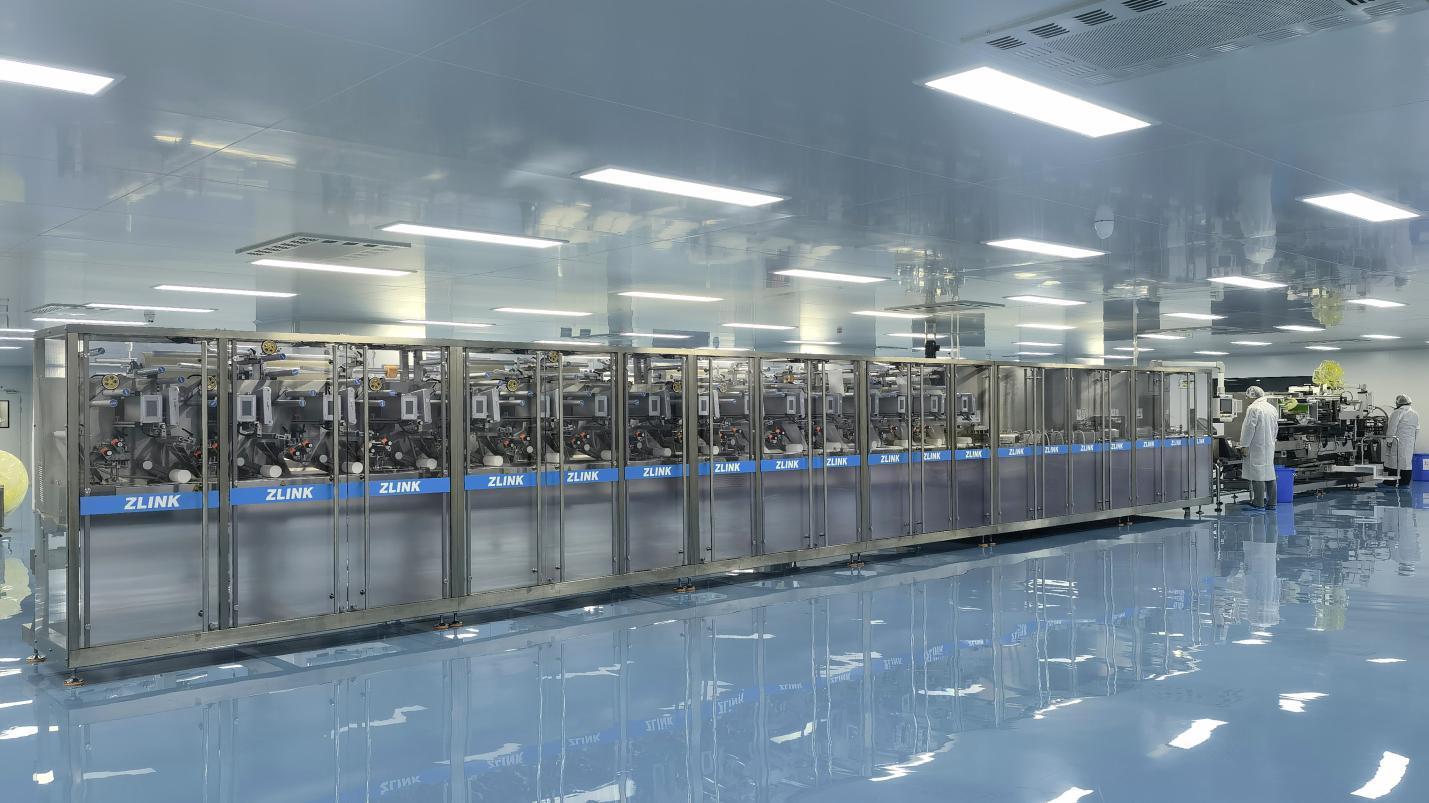
Our medical mask production lines utilize advanced automated controls. We apply these identical strict, particle-controlled environments to assemble, calibrate, and seal thermometry sensors, ensuring zero contamination.
B2B importers benefit from high-capacity factories with dual capabilities in healthcare PPE and precise thermometry. This structure reduces tariff risks, simplifies logistics, and ensures steady wholesale volume delivery.
The technological developments and material advancements reshaping B2B demands for global commercial kitchen equipment.
The evolution of the Termómetro de Cocina is directly tied to the smart kitchen and industrial automation revolution. Suppliers must move past basic analog bimetallic designs to offer high-precision digital instruments. Understanding these trends is critical for distributors and wholesalers looking to capture market share over the next decade.
Modern commercial operations require wireless, cloud-connected probes that transmit real-time telemetry to central databases. If a cooling unit or slow-roasting oven drifts out of the target zone, automated systems instantly alert staff. This approach reduces food waste and ensures absolute safety compliance.
Next-generation cooking probes do not just measure temperature at one point. They utilize arrays of 3 to 8 internal sensors along the stem to detect both core temperature and ambient thermal environments. This design calculates heat-transfer rate, predicting exact safe resting times.
Cleanability is paramount. Kitchen environments feature airborne grease, steam, and high organic matter. High-grade thermometers must have IP67 or IP68 waterproof ratings, allowing complete immersion in sanitizing solutions without damaging sensitive internal calibration.
How varying regional requirements and industrial settings dictate customized thermal safety solutions.
Across the globe, the deployment of culinary measurement tools varies based on regional standards, dining habits, and food manufacturing traditions. Trusted suppliers must tailor their catalog offerings to these specific target scenarios:
To address these requirements, Zhejiang DrSharpe Health Co., Ltd. uses a macro engineering approach. By combining our knowledge in manufacturing medical plastics, cleanroom packaging, and precise electronics, we construct thermometers that exceed basic food-handling guidelines. We use raw materials that resist degradation under exposure to fats, acids, and harsh cleaning agents. This ensures long-term calibration stability and helps prevent chemical contamination in food preparation.
A structured outline of our ongoing research, sensor upgrades, and integration of safety equipment manufacturing.
Reducing typical probe thickness from 3.5mm down to 1.8mm at the tip. This minimizes juice loss in proteins and decreases measurement response times to under 1.5 seconds.
Developing hybrid hand-held tools that integrate non-contact infrared surface lasers with a folding penetration probe. This gives food safety operators dual-verification capabilities in one tool.
Developing native SDKs for restaurant kitchen software, allowing automated logging. Real-time temperature checks sync directly with daily HACCP checklists, eliminating manual paper logging errors.
Introducing biodegradable outer casings and recyclable electronics to reduce the ecological impact of high-volume kitchen thermometer sourcing.
Bridging professional health security systems, precision manufacturing, and global healthcare supply lines.
Zhejiang DrSharpe Health Co., Ltd. is a leading manufacturer and global supplier specializing in disposable medical, healthcare products, and protective solutions. Leveraging our high-precision manufacturing, we supply key components and quality-controlled safety tools for global consumer and industrial applications, including high-grade Termómetro de Cocina solutions.
With robust manufacturing capabilities, advanced production technology, and strict quality management systems, DrSharpe provides safe, reliable, and comfortable health products for customers worldwide.
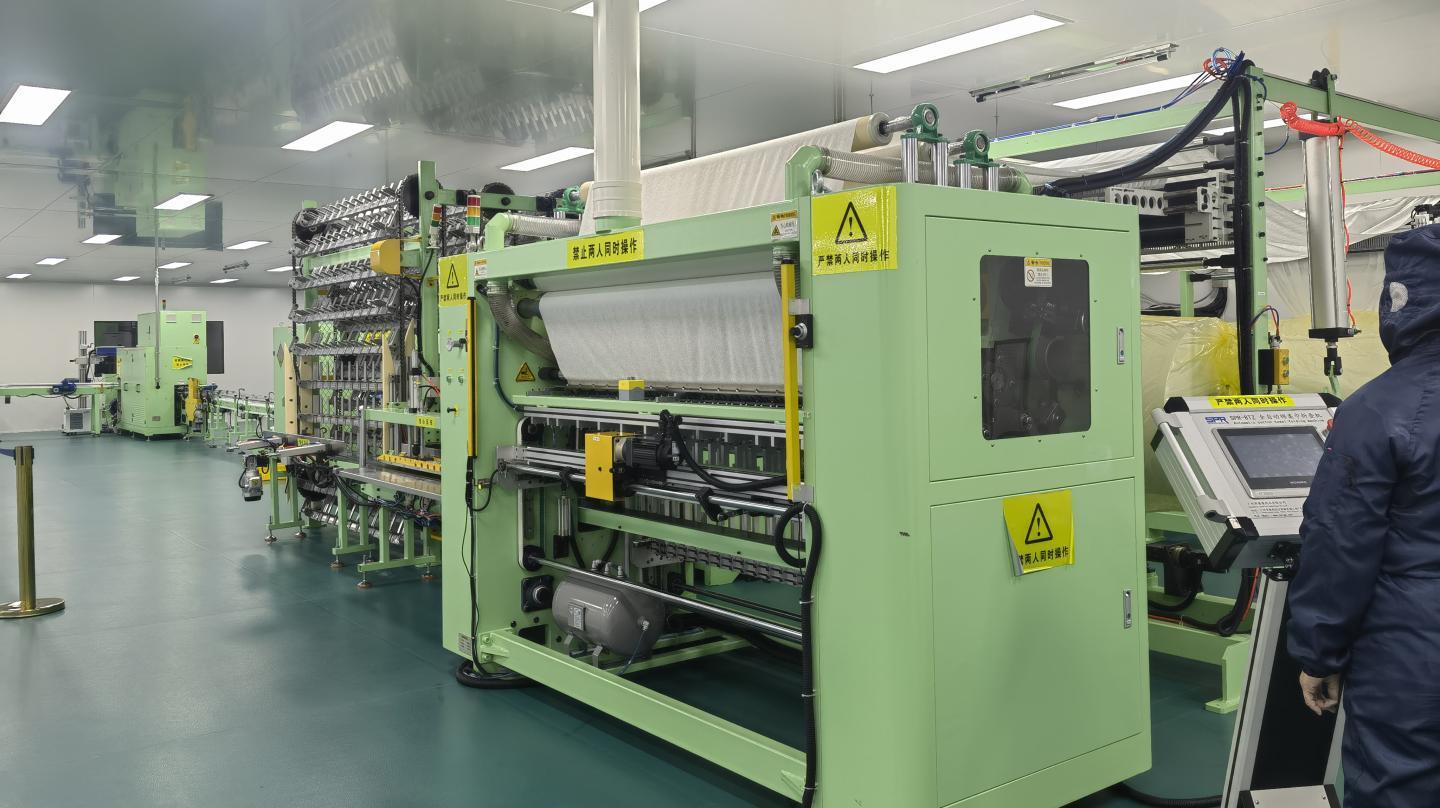
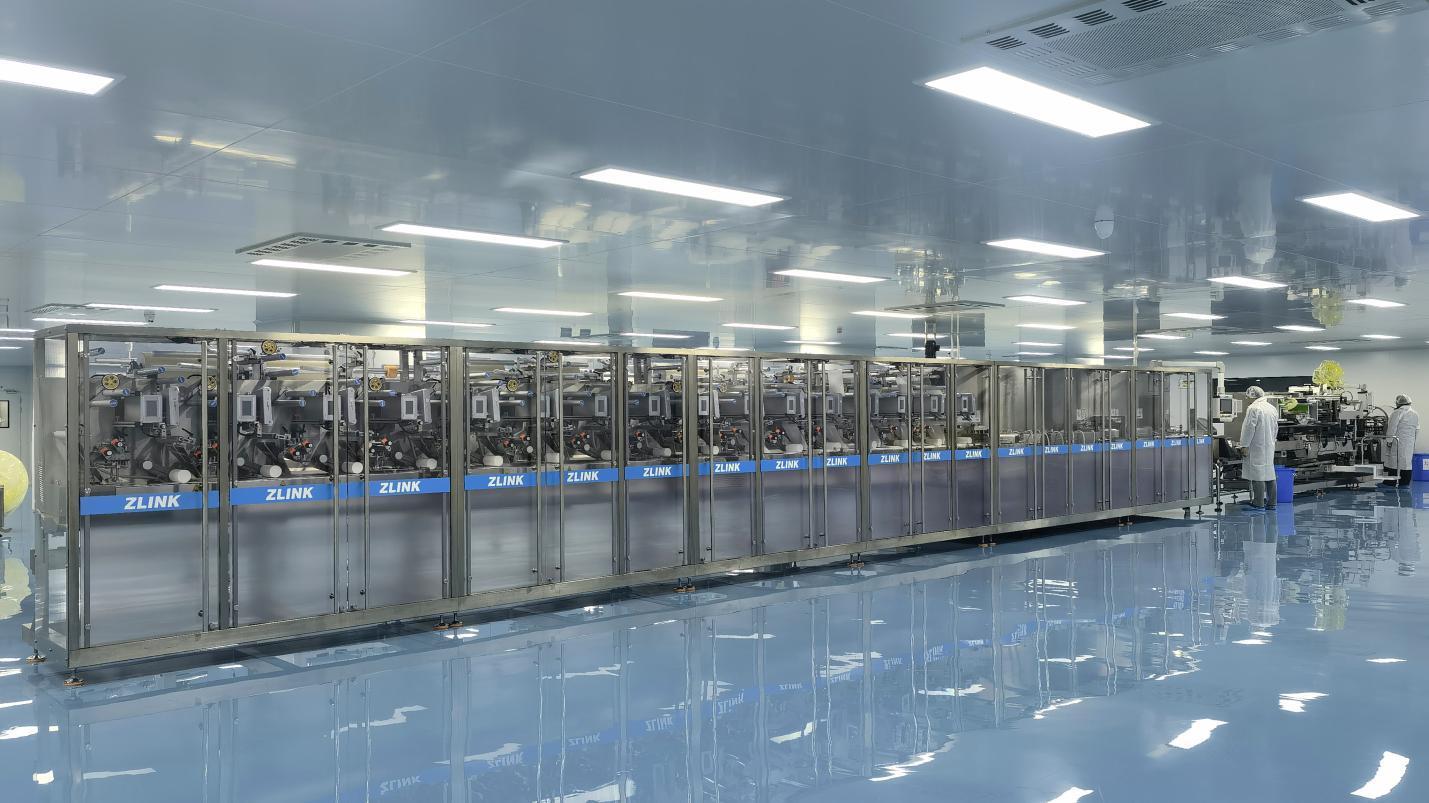
Our modern manufacturing facility is equipped with 5 fully automatic mask production lines and 12 semi-automatic production lines. These are managed by an experienced production and quality assurance team. From selecting high-grade raw materials to the final packaging stages, we monitor each step to ensure stable quality and reliable volume delivery. Our products are exported to major global markets, including the United States, Europe, Japan, Mexico, Germany, and the United Kingdom.
DrSharpe mainly provides disposable face masks and healthcare products for medical, personal protection, and daily use. Using advanced filtration materials, our masks achieve up to 99% Bacterial Filtration Efficiency (BFE) and 99% Particle Filtration Efficiency (PFE). This provides reliable respiratory defense without sacrificing wearer comfort. Our production processes comply with global safety standards and carry official certifications, including CE, US FDA, and US EUA.
Answering key questions on industrial thermometry integration, calibration verification, and safety hardware sourcing.
High-standard protective gear, dust respirators, and sanitization support products for food handling and medical operations.