DrSharpe Health
Explore our leading medical, daily, and special protection mask products manufactured under strict global standards.
In the contemporary landscape of occupational health and global safety procurement, the role of protective equipment has shifted from an ad-hoc emergency solution to a highly regulated, standardized sector. While disposable options have long dominated the market, the industrial demand for Mascarillas Reutilizables (reusable masks) has grown rapidly, driven by environmental sustainability mandates and the need for structural cost optimization in long-term operations.
Modern B2B buyers—representing healthcare systems, industrial complexes, and global distribution chains—no longer select masks based on price alone. Factors such as particle filtration efficiency (PFE), differential pressure (breathability), skin biocompatibility, and manufacturing compliance are now the dominant metrics. As a premier Chinese manufacturer, Zhejiang DrSharpe Health Co., Ltd. sits at the intersection of this transition, combining high-throughput automated manufacturing with top-tier filtration technology to deliver high-performance solutions worldwide.
Zhejiang DrSharpe Health Co., Ltd. leverages state-of-the-art machinery and rigorous quality systems to achieve consistent performance indicators.
Established as a pioneering force in safety technology and medical consumables, Zhejiang DrSharpe Health Co., Ltd. stands as a professional manufacturer and global supplier specializing in advanced respiratory protection, medical face masks, and sanitization products. We maintain a strong commitment to quality control and operational transparency, enabling us to serve medical institutions, industrial distributors, and consumer brands in the United States, Europe, Japan, Mexico, Germany, and the United Kingdom.
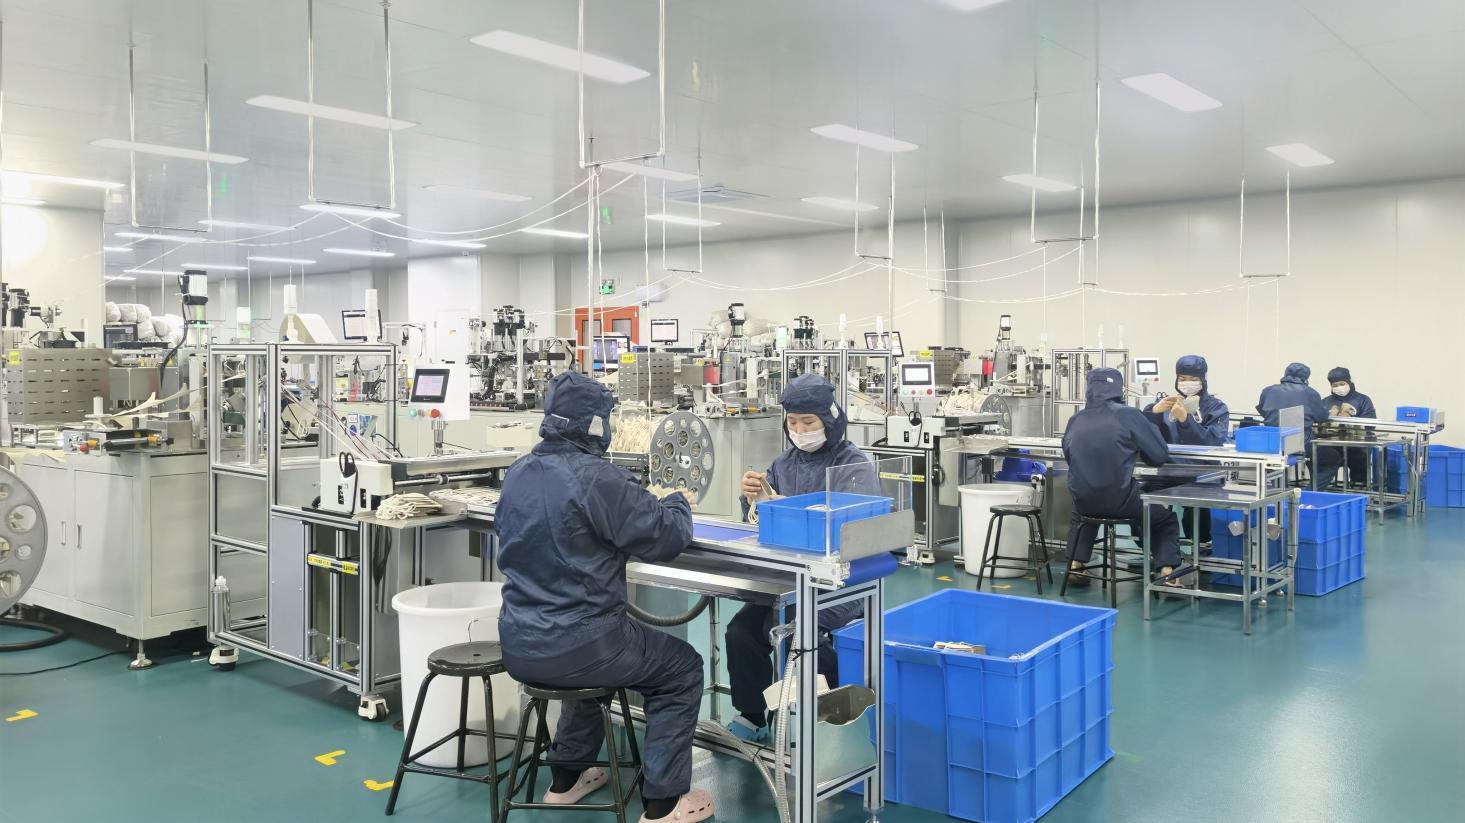
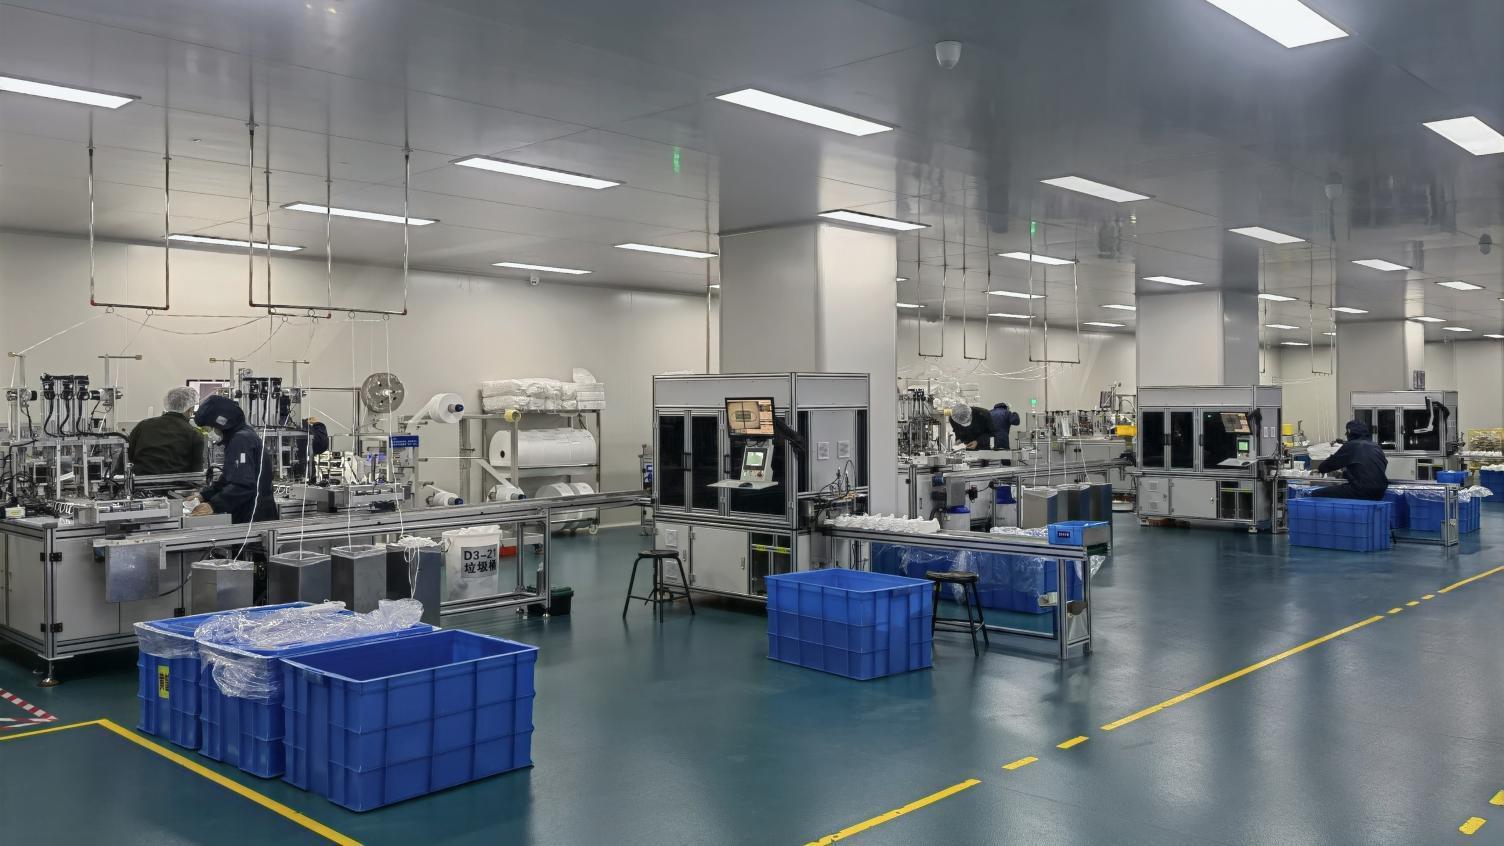
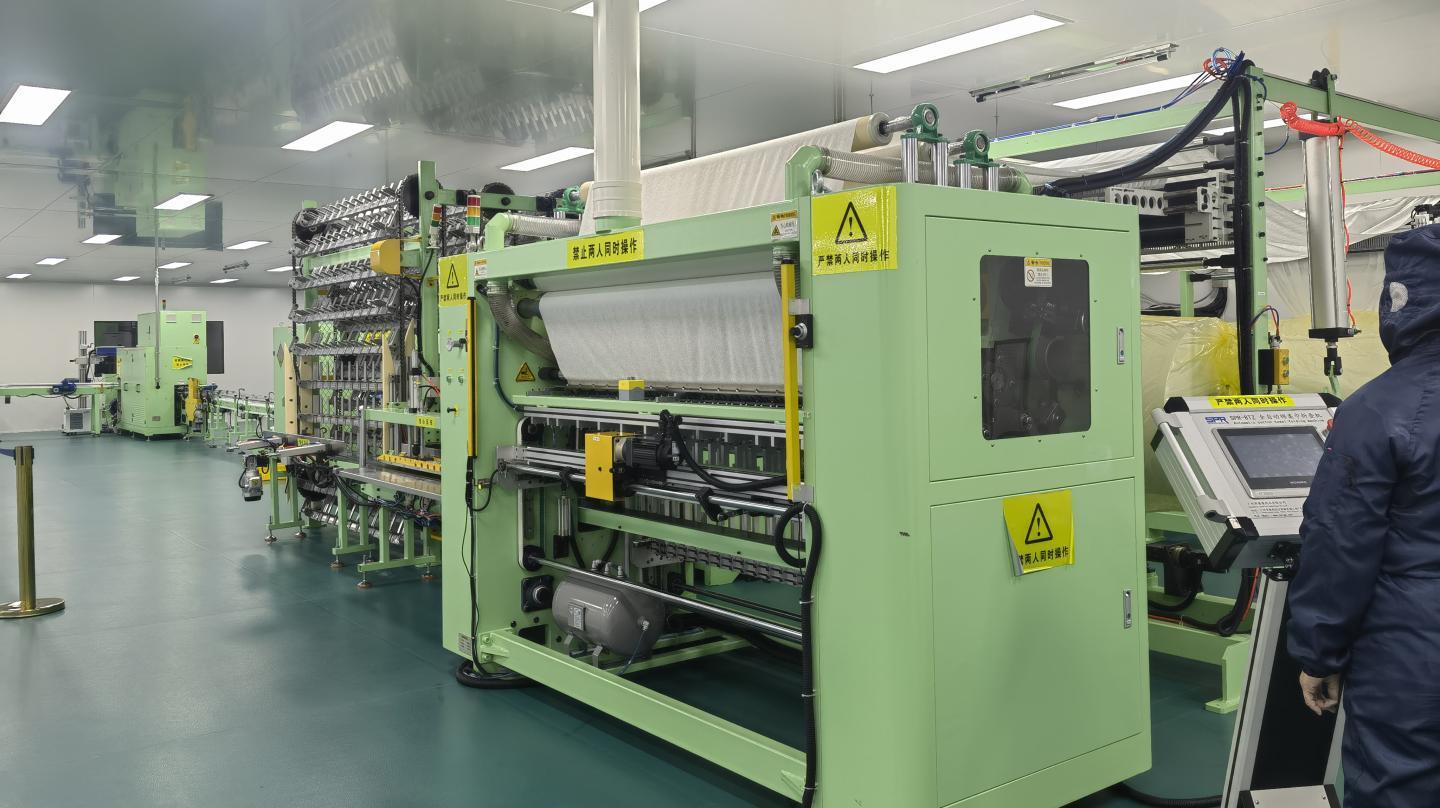
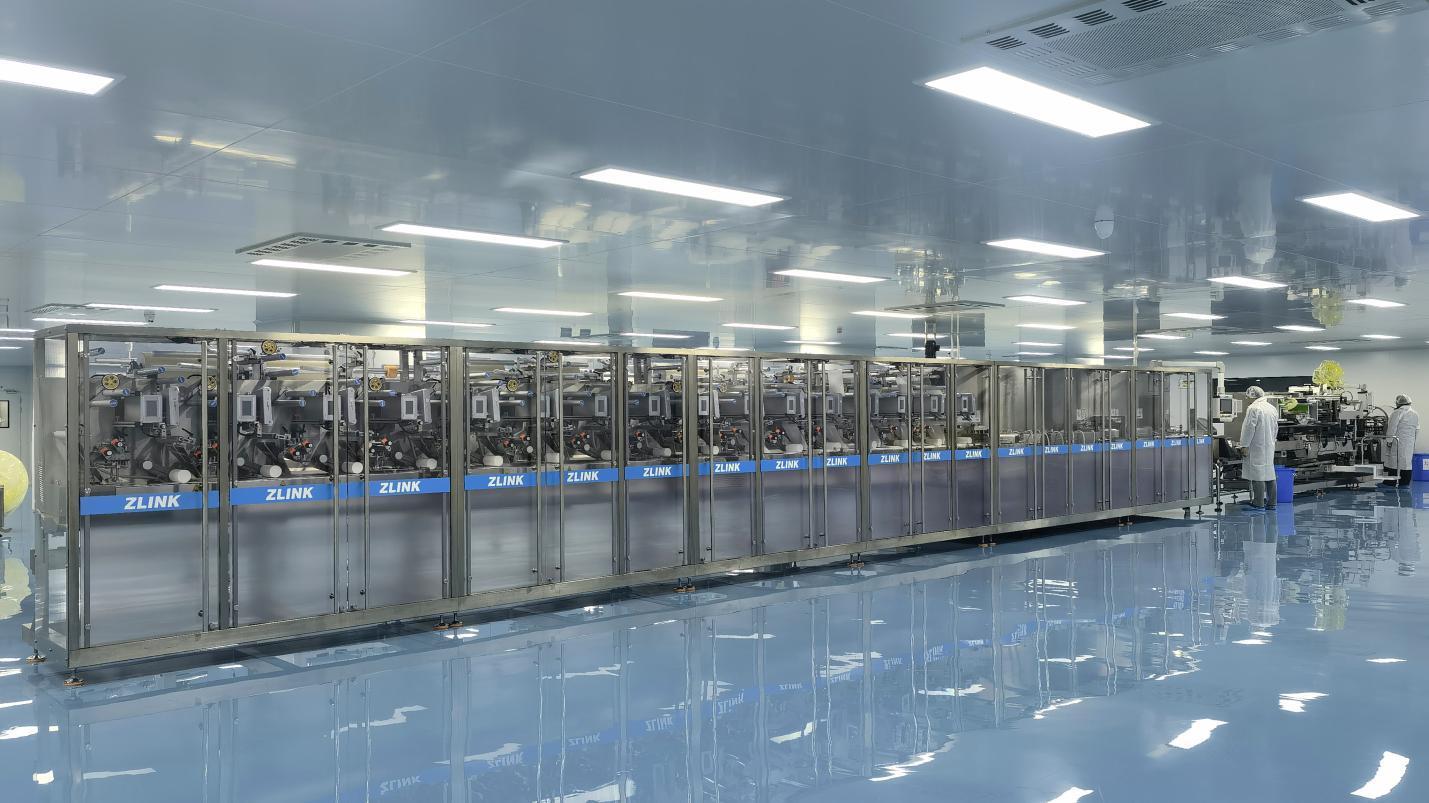
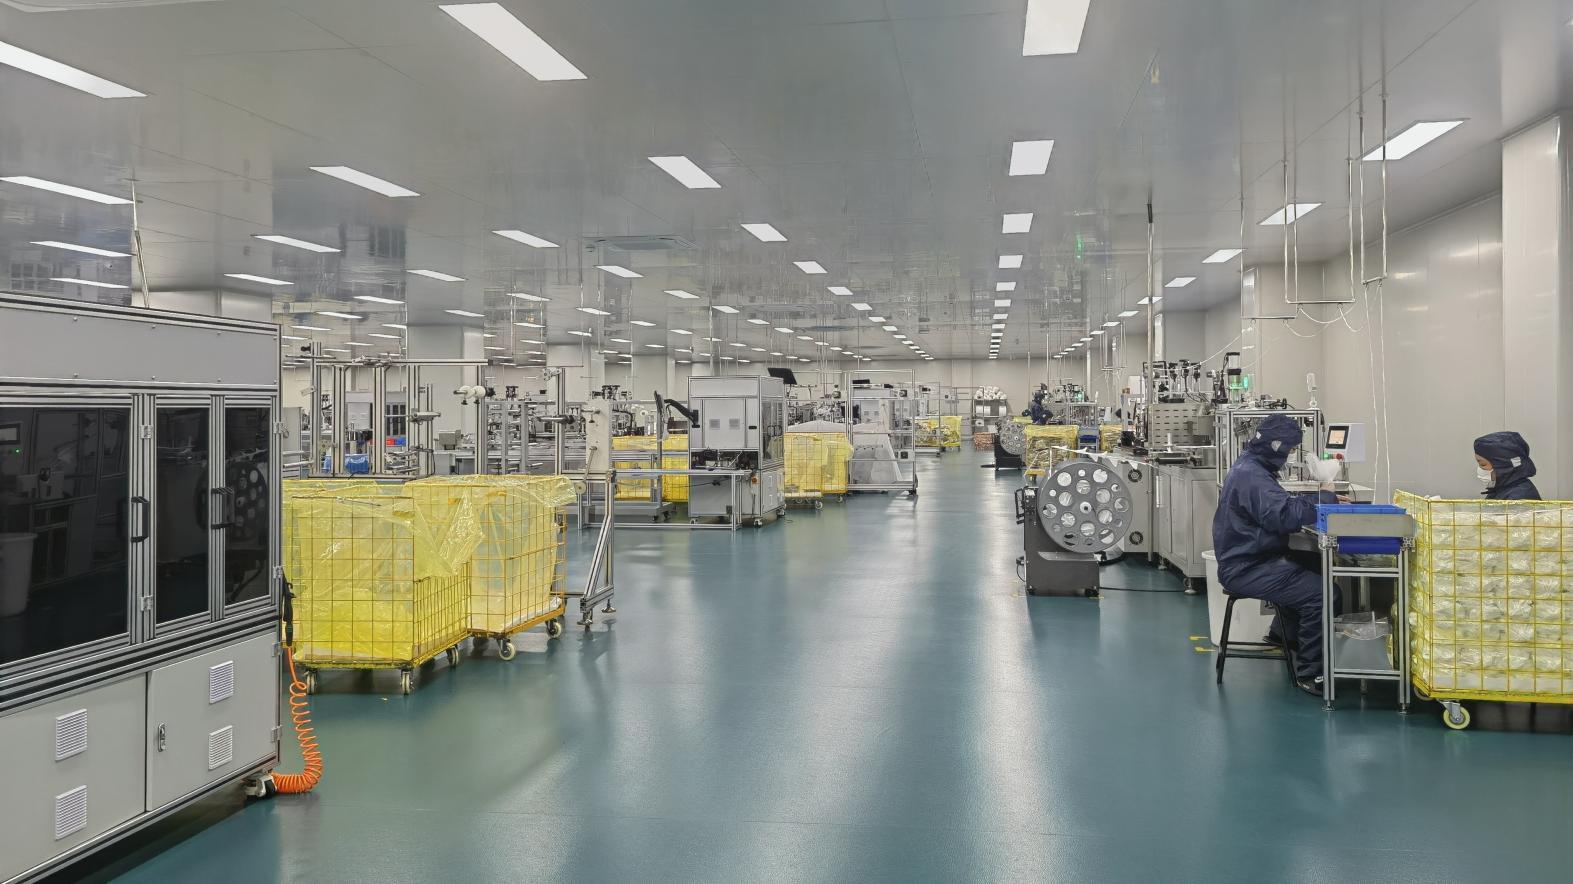
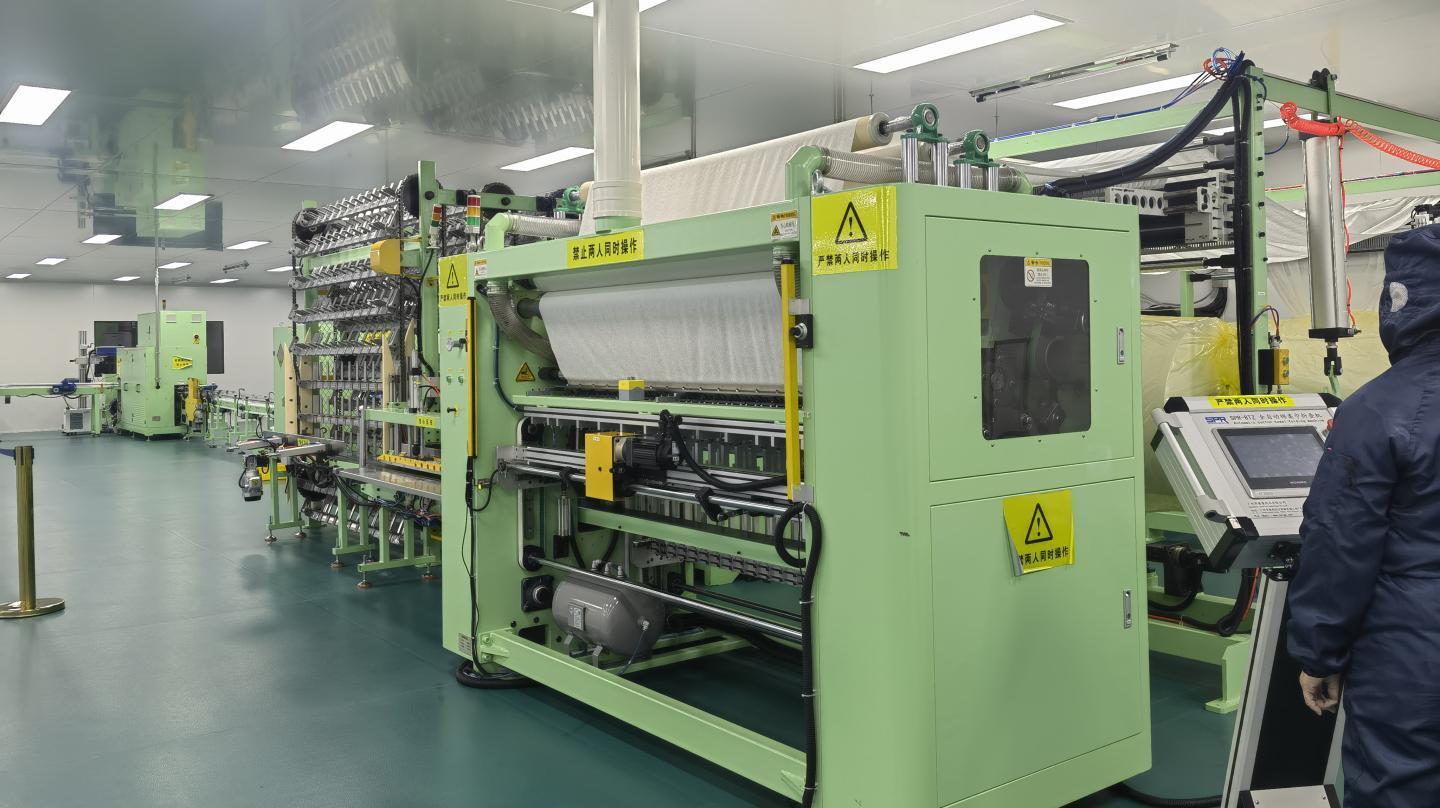
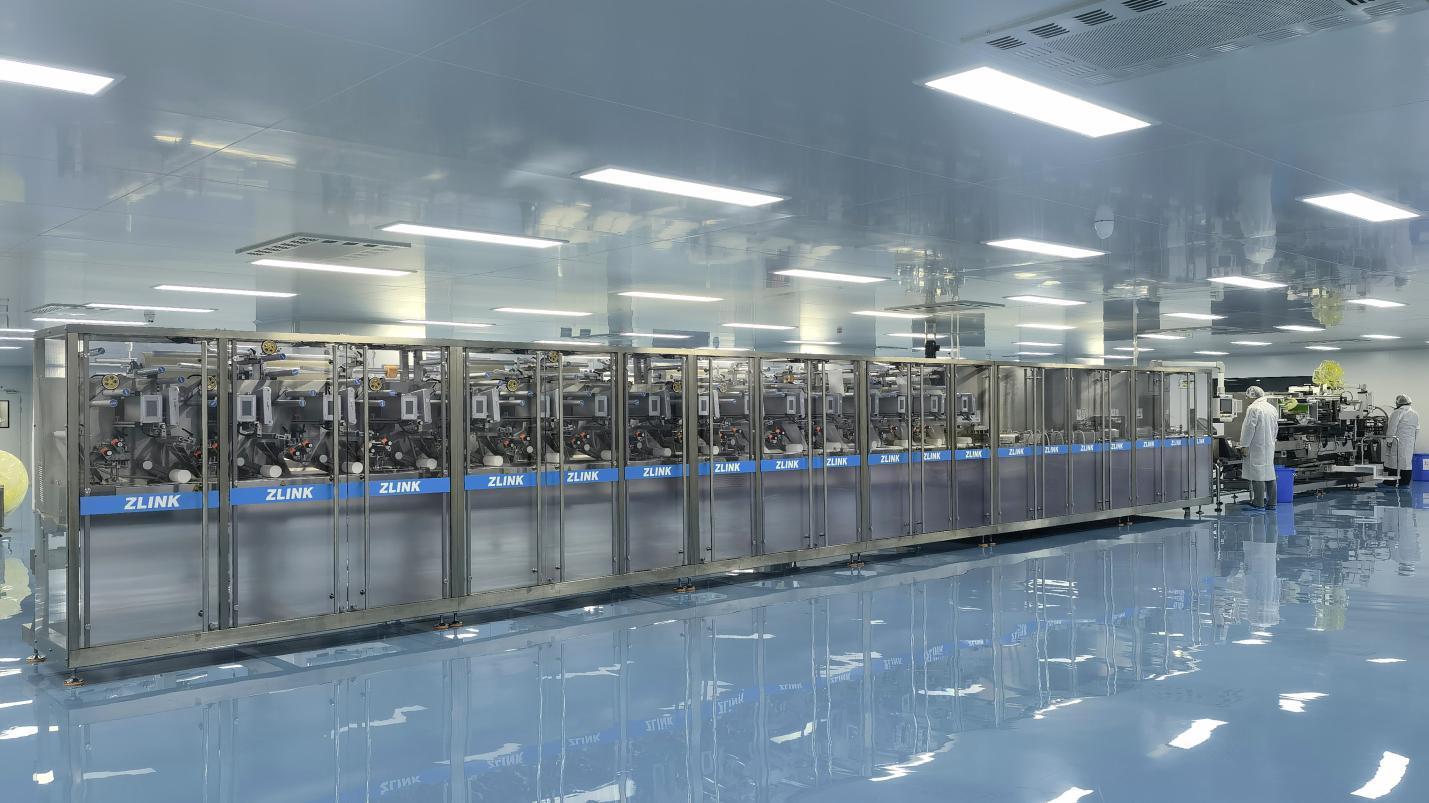
Our modern manufacturing facility is structurally optimized for mass-volume output under sterile environmental conditions. By utilizing 5 fully automatic mask production machines and 12 semi-automatic production setups, we ensure that our output remains consistent, scalable, and responsive to fluctuations in global market demand. From raw non-woven polypropylene melt-blown feedstocks to completed, sanitized product shipments, our production is audited at every stage to prevent defect proliferation.
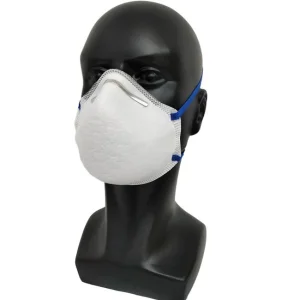
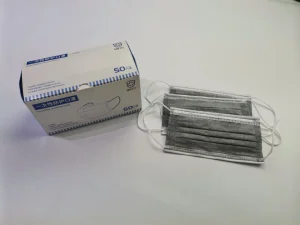
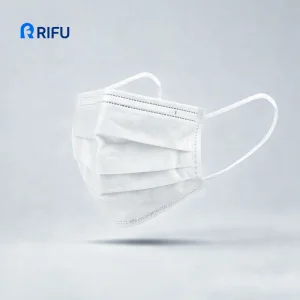
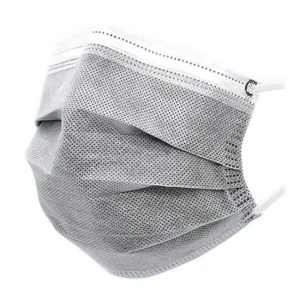
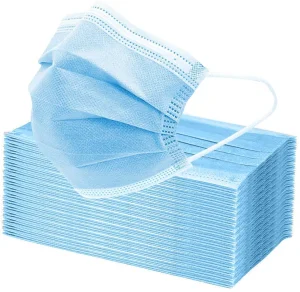
Our masks utilize a multi-structured synthetic non-woven fabric. The outer hydrophobic layer repels ambient fluids and splash zones, while the core features an electrostatically charged melt-blown membrane that traps sub-micron particulate matters with Minimal Breathing Resistance (Delta P).
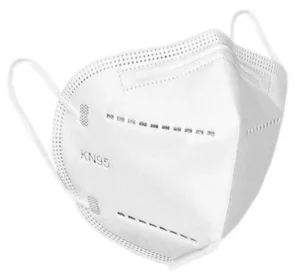
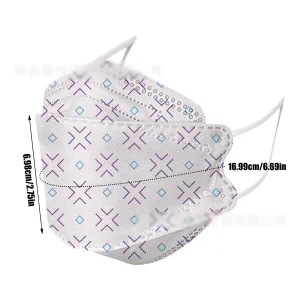
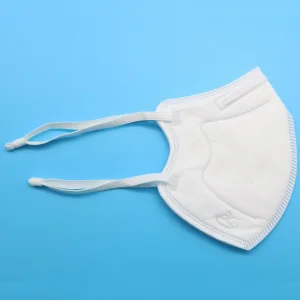
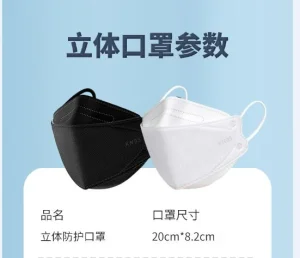
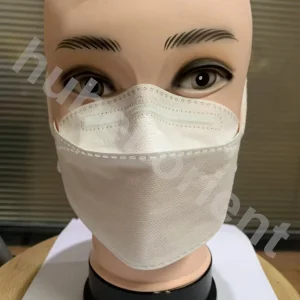
Minimizing total inward leakage (TIL) is crucial. Our 3D-folded and KF94-compliant contours conform seamlessly to diverse facial geometries, optimizing seal integrity. This design prevents humid air bypass, reducing fogging of eyewear in clinical setups.
We systematically monitor every phase to guarantee that our products are free from chemical solvents, irritants, or latex. High-elasticity ear loops are ultrasonically welded, achieving excellent tensile strength and minimizing breakage risk.
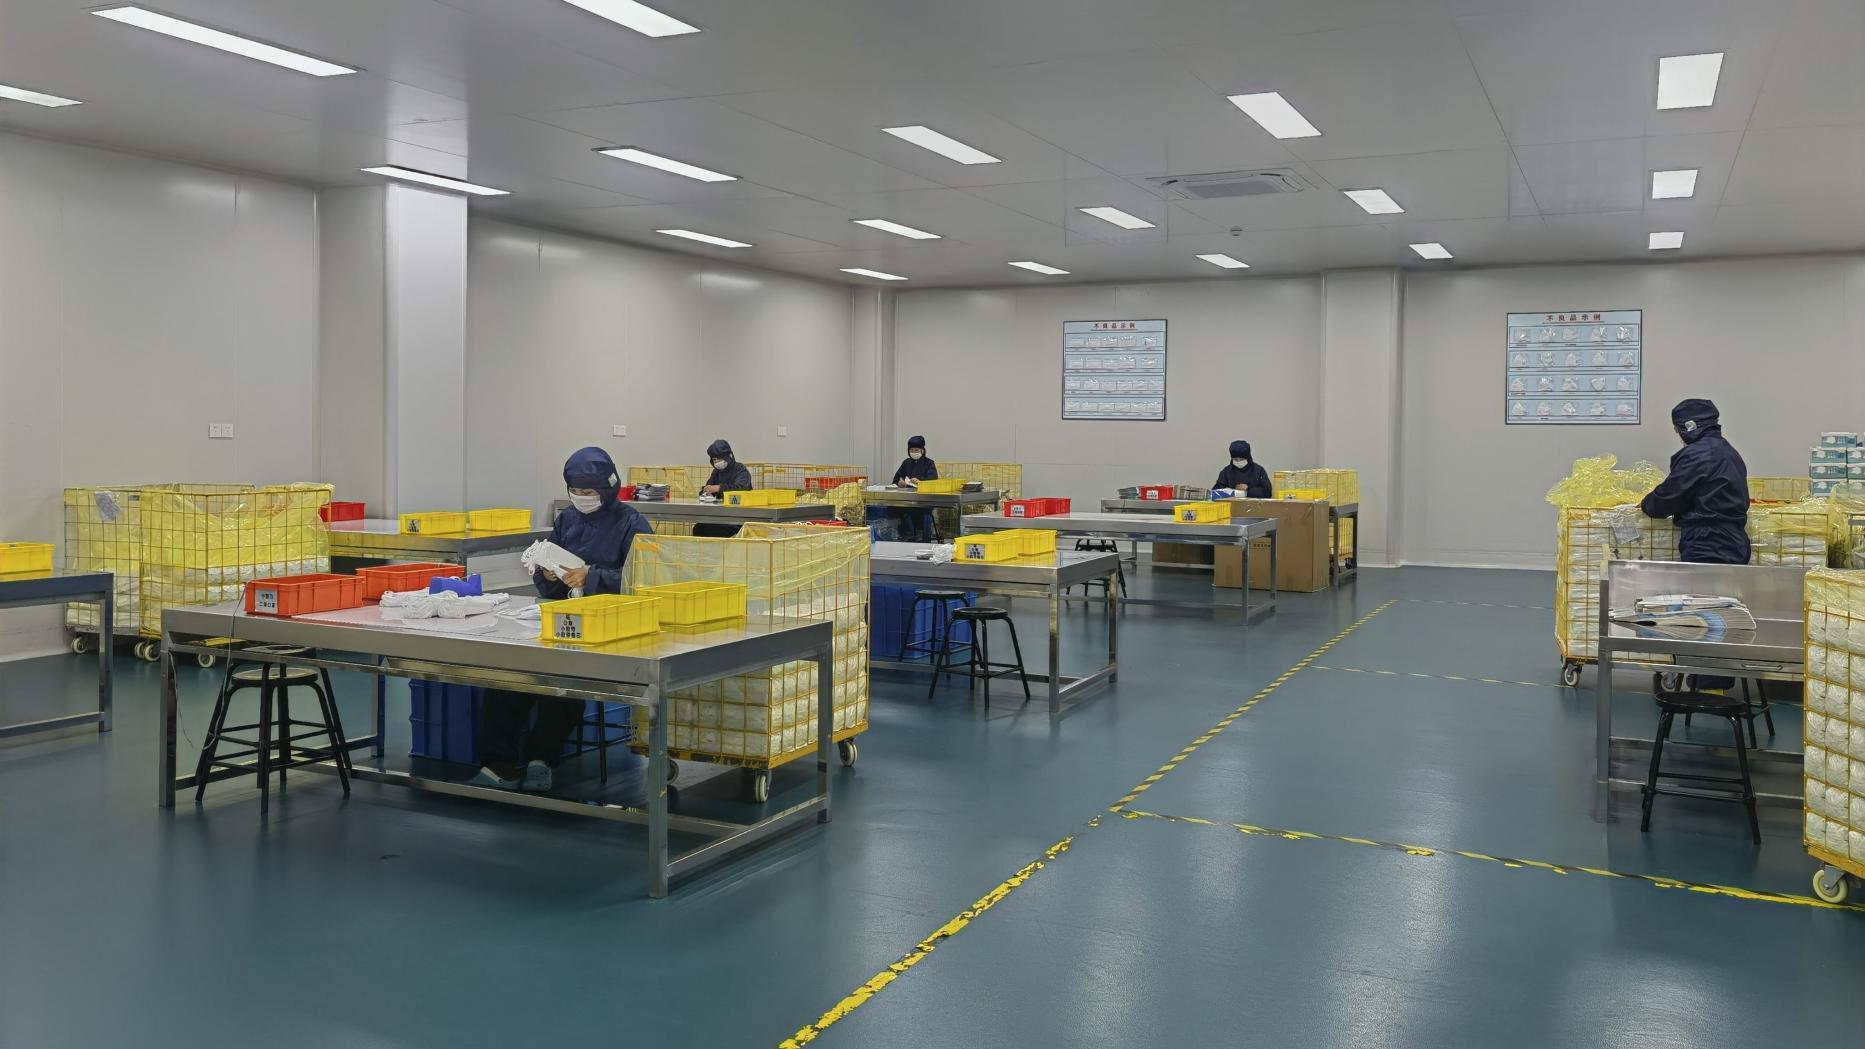
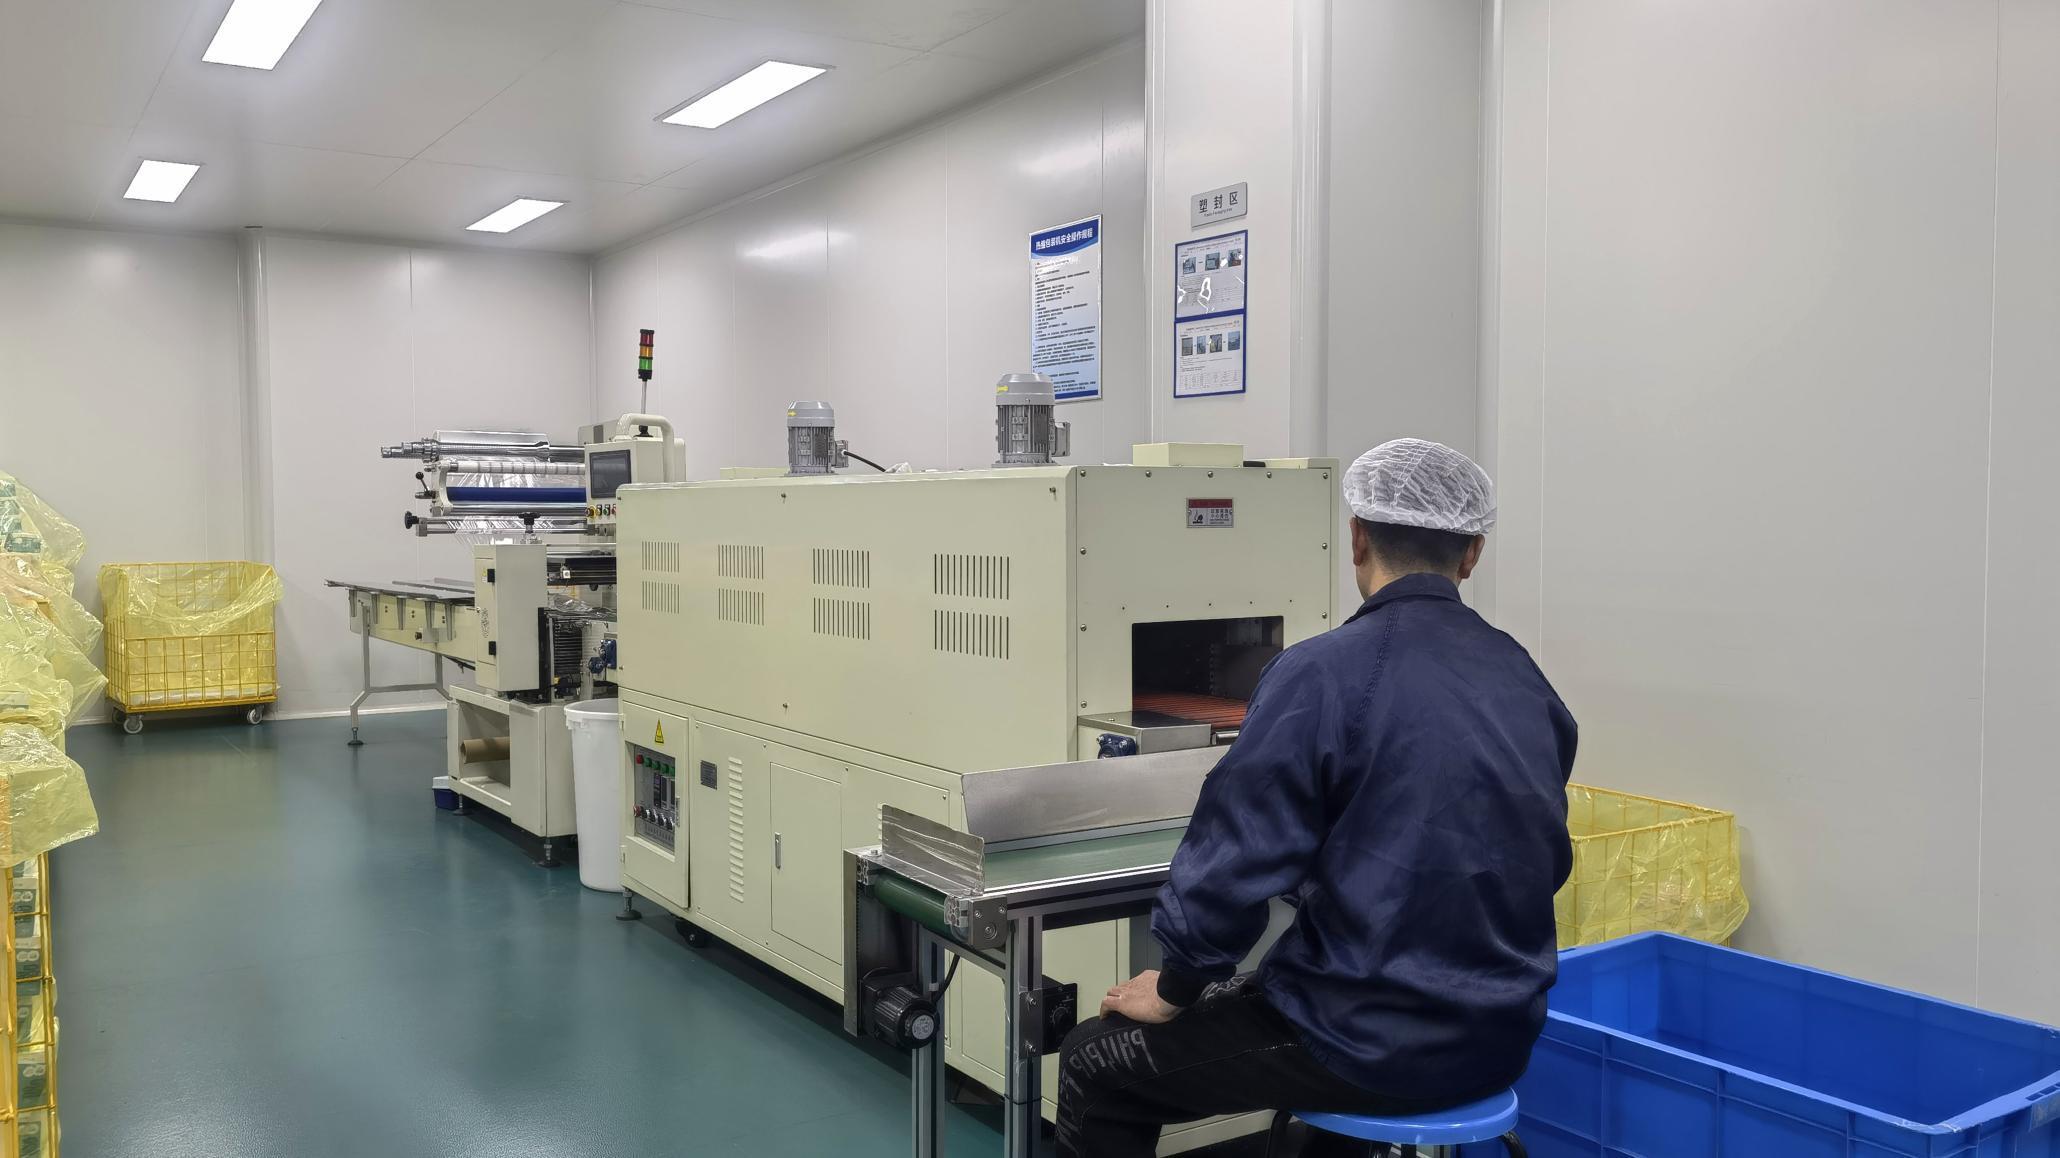
Take a detailed look at our processing facility in Zhejiang. All production lines are maintained under ISO-certified sanitary conditions.
Importing protective medical products requires navigating complex local regulations. Zhejiang DrSharpe Health Co., Ltd. provides comprehensive compliance documentation to streamline this process, including:
Navigating the global market for respiratory equipment requires secure, scalable supply chain pathways. Zhejiang DrSharpe Health Co., Ltd. has developed structured logistical frameworks that address common supply chain bottlenecks:
OEM and Private Label Customization: We offer custom configuration of packaging, structural layers, brand marking, and earloop specifications, allowing distributors to meet specific domestic standards (e.g., COFEPRIS in Mexico, standard EN regulations in Europe, or FDA rules in the US).
Stable Raw Material Sourcing: By maintaining strong partnerships with leading non-woven and melt-blown raw material providers in mainland China, we secure consistent pricing and stable inventory, helping shield our clients from market price fluctuations.
As the industry moves toward sustainable and technology-integrated solutions, DrSharpe is investing in research and development to align with future market demands. Our R&D team focuses on key innovation pathways:
We are researching Polylactic Acid (PLA) polymers derived from renewable biomass to replace traditional polypropylene. This transition aim is to maintain >98% PFE while significantly reducing the environmental footprint of discarded protective equipment.
By integrating metal-organic frameworks (MOFs) or copper-ion nanoparticles into the outer layers of our masks, we are working to develop self-sanitizing surfaces that actively neutralize biological agents upon contact.
By optimizing the physical structure of electrostatically charged melt-blown fibers, we aim to reduce the Delta P indicator to under 25 Pa, providing improved comfort during extended wear in physically demanding settings.
Technical and regulatory guidance for international buyers sourcing protective face coverings and medical supplies from China.
Single-use surgical masks are designed for clinical scenarios and must be discarded after one shift to prevent pathogen buildup. Reusable masks, often utilized in civil and industrial contexts, are made from washable fabrics or elastomer shells with replaceable, high-efficiency particulate filter cartridges (such as N95, KN95, or KF94 inserts), offering a cost-effective and environmentally friendly option for long-term wear.
Our masks undergo standardized testing at third-party laboratories. Bacterial Filtration Efficiency (BFE) is measured using a Staphylococcus aureus aerosol challenge, while Particle Filtration Efficiency (PFE) is assessed using a 0.3-micron sodium chloride (NaCl) aerosol challenge. Both tests consistently indicate efficiency ratings of 99% or higher, matching or exceeding international clinical standards.
We maintain active registrations with the US FDA and hold US EUA listings where applicable. For imports into South American regions, including Mexico and Colombia, we provide complete testing dossiers that align with standard EN 14683 or ASTM F2100 guidelines, helping our clients navigate regulatory clearance with national health authorities like COFEPRIS or INVIMA.
Our standard Minimum Order Quantity (MOQ) depends on the specific mask style, typically starting at 50,000 units for standard designs and 100,000 units for custom OEM packaging. Once order parameters are finalized, our automated lines can process and package shipments within 15 to 25 business days, depending on seasonal demand and scheduled production volume.
Complete medical-grade respiratory array, optimized for industrial use, daily filtration, and clinical settings.