DrSharpe Health
Direct from our high-capacity production lines. Built on raw-material tracebility, advanced non-woven electret charging, and certified to medical standards.
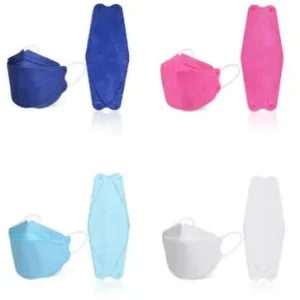
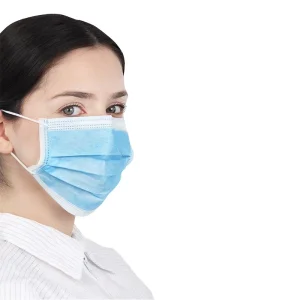
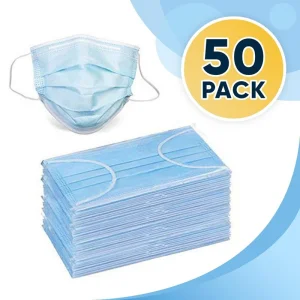
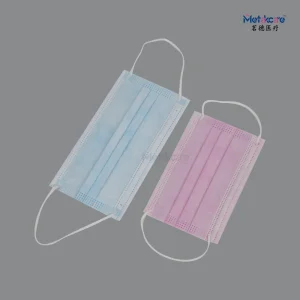
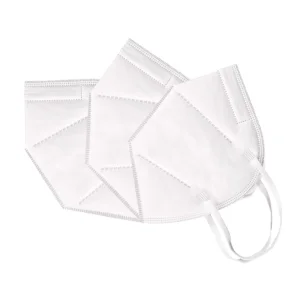
Global medical supply chains are experiencing a structural pivot. While white and traditional light blue medical masks remain staples, demand for high-performance colored face masks has grown significantly across clinical, commercial, and industrial segments.
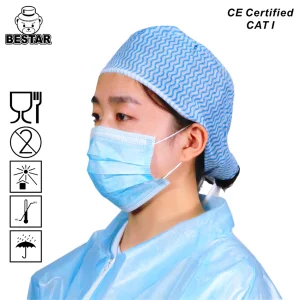
These colored masks are no longer viewed merely as lifestyle choices. They serve vital roles in modern workspaces: color-coded zoning in cleanrooms, corporate brand integration in customer-facing roles, and reduced clinical anxiety in pediatric wards. This shift requires manufacturers to maintain high filtration efficiency (BFE/PFE ≥ 99%) while ensuring pigment safety, bio-compatibility, and compliance with ASTM F2100, EN14683 Type IIR, and NIOSH standards.
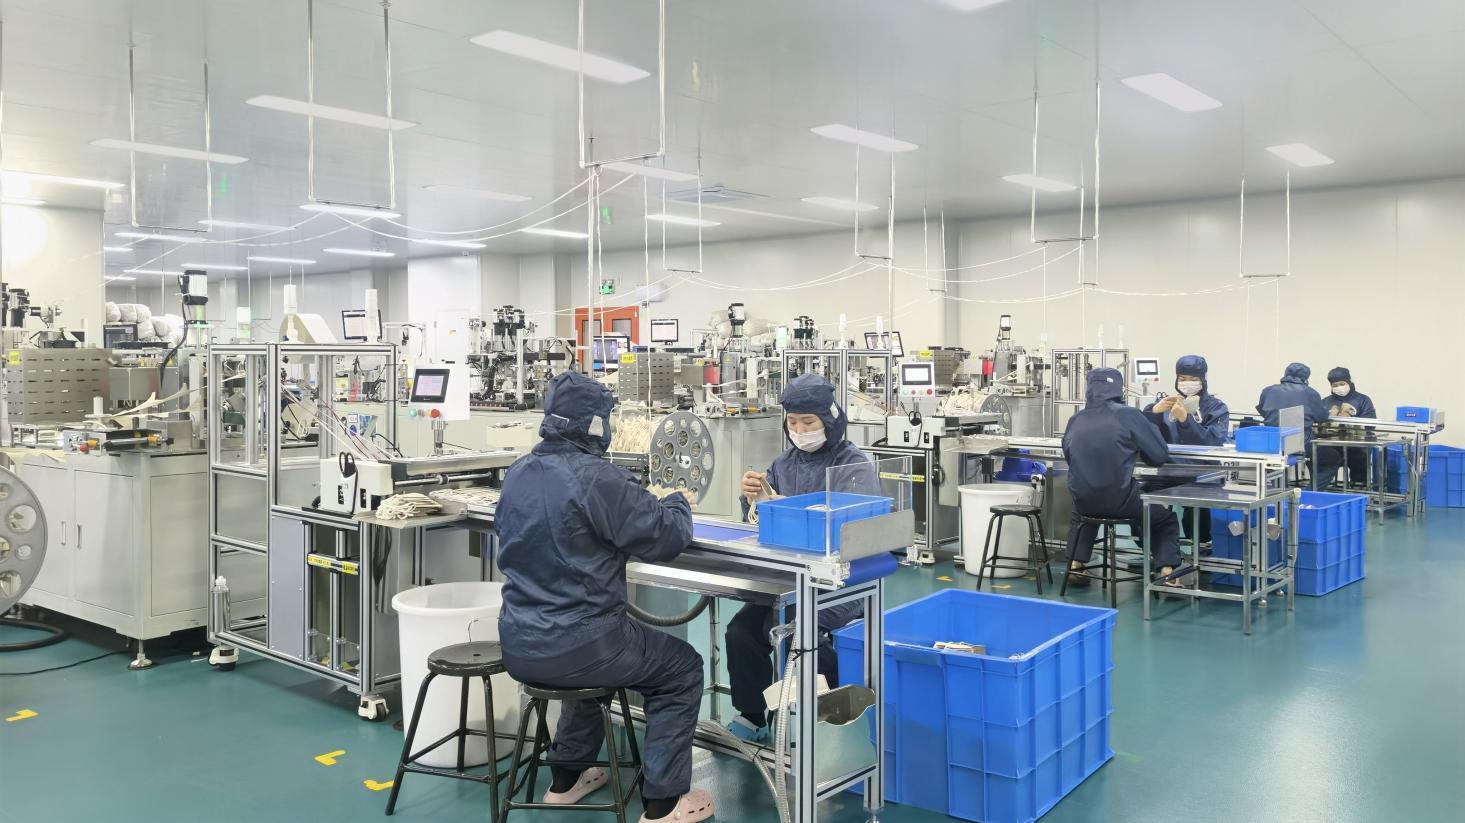
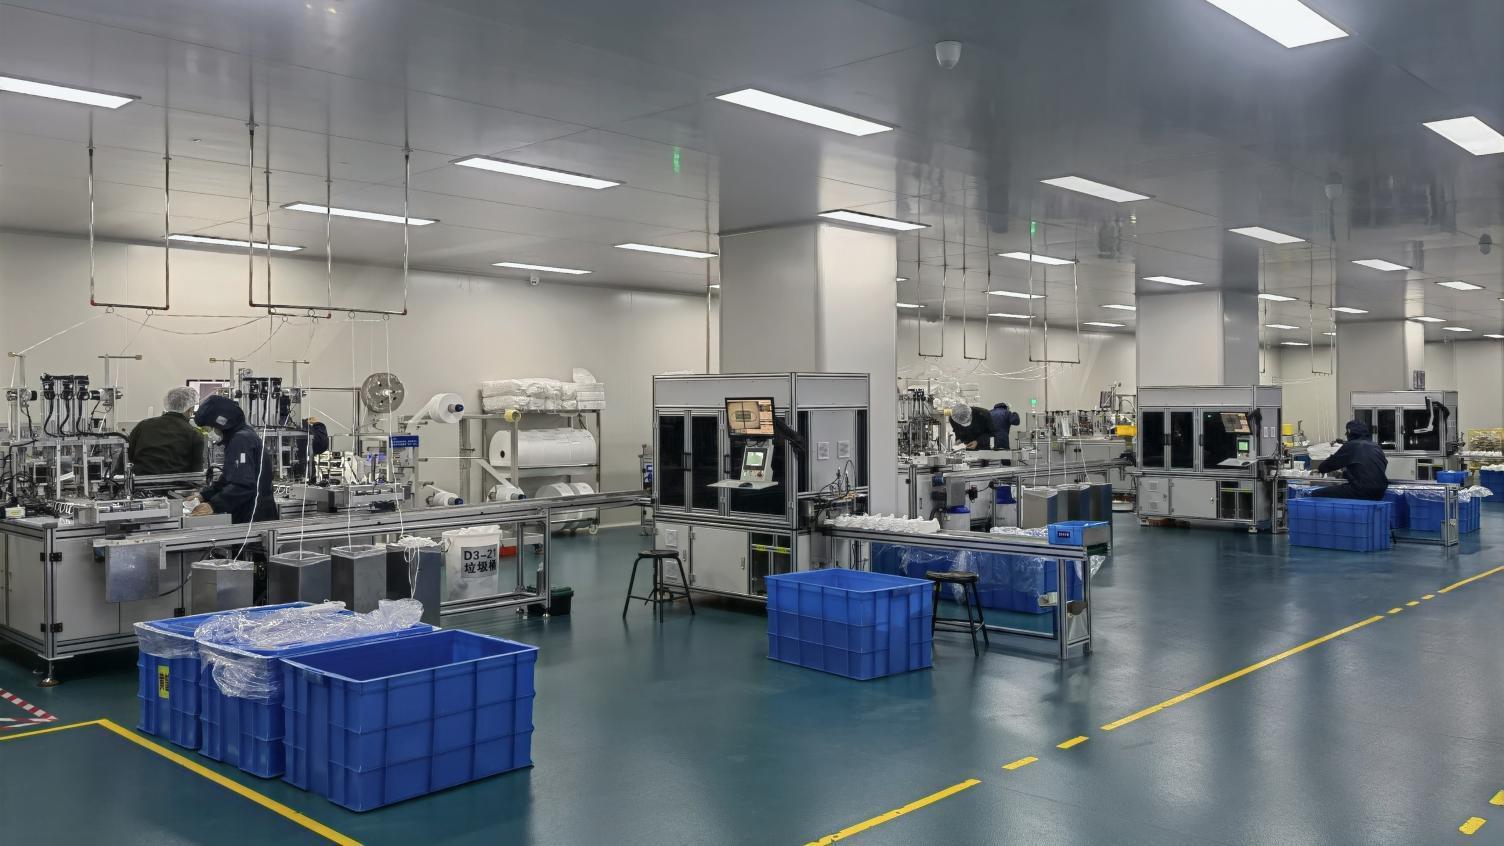
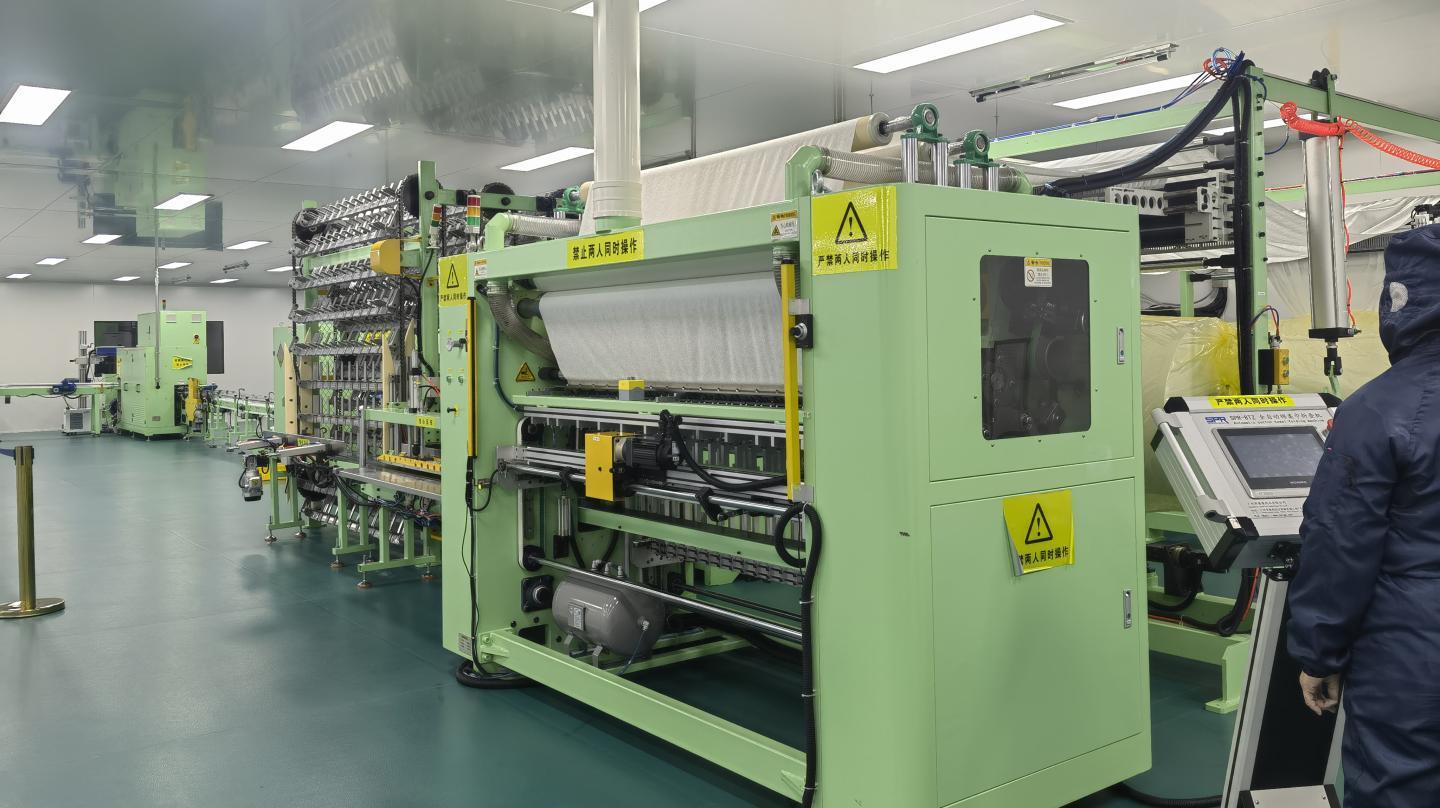
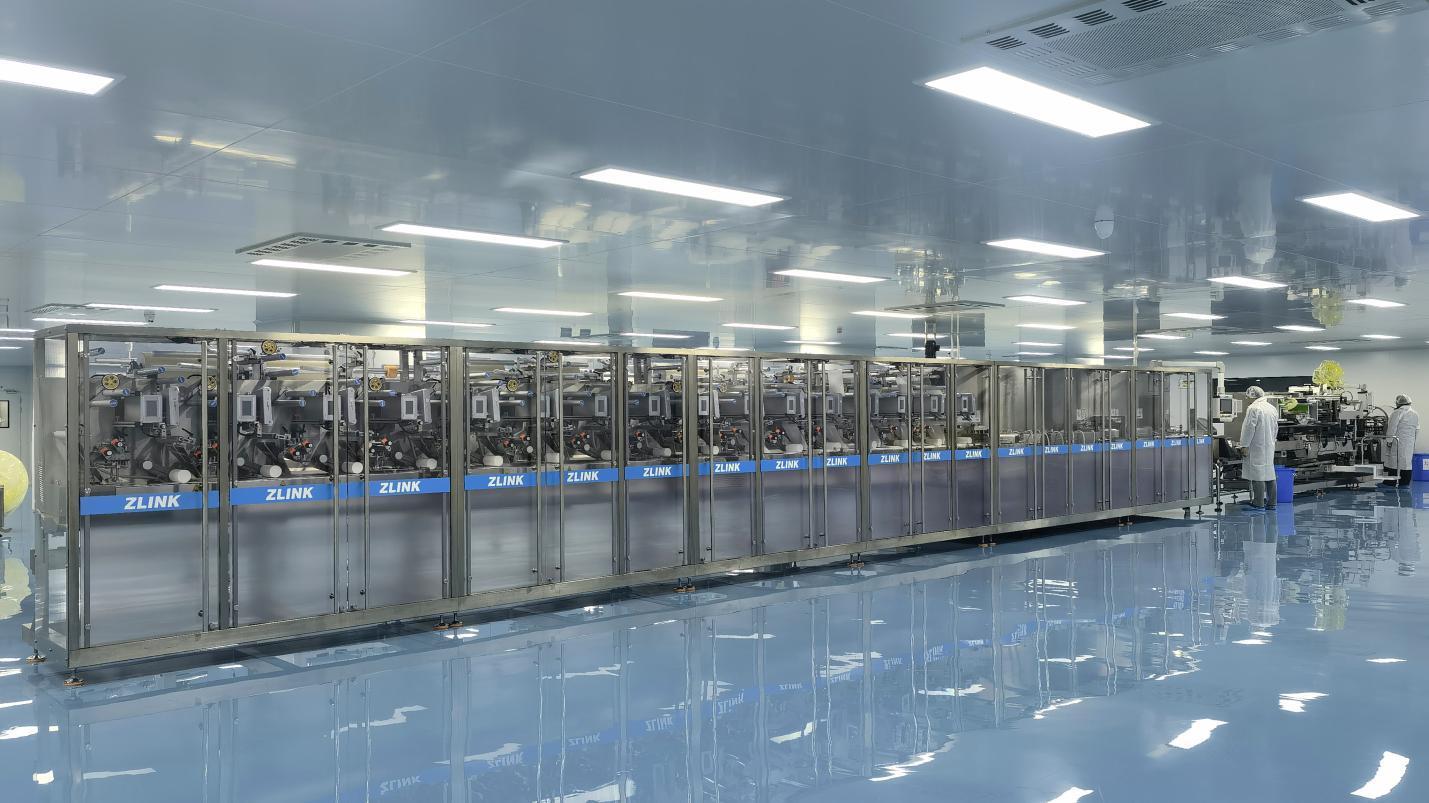
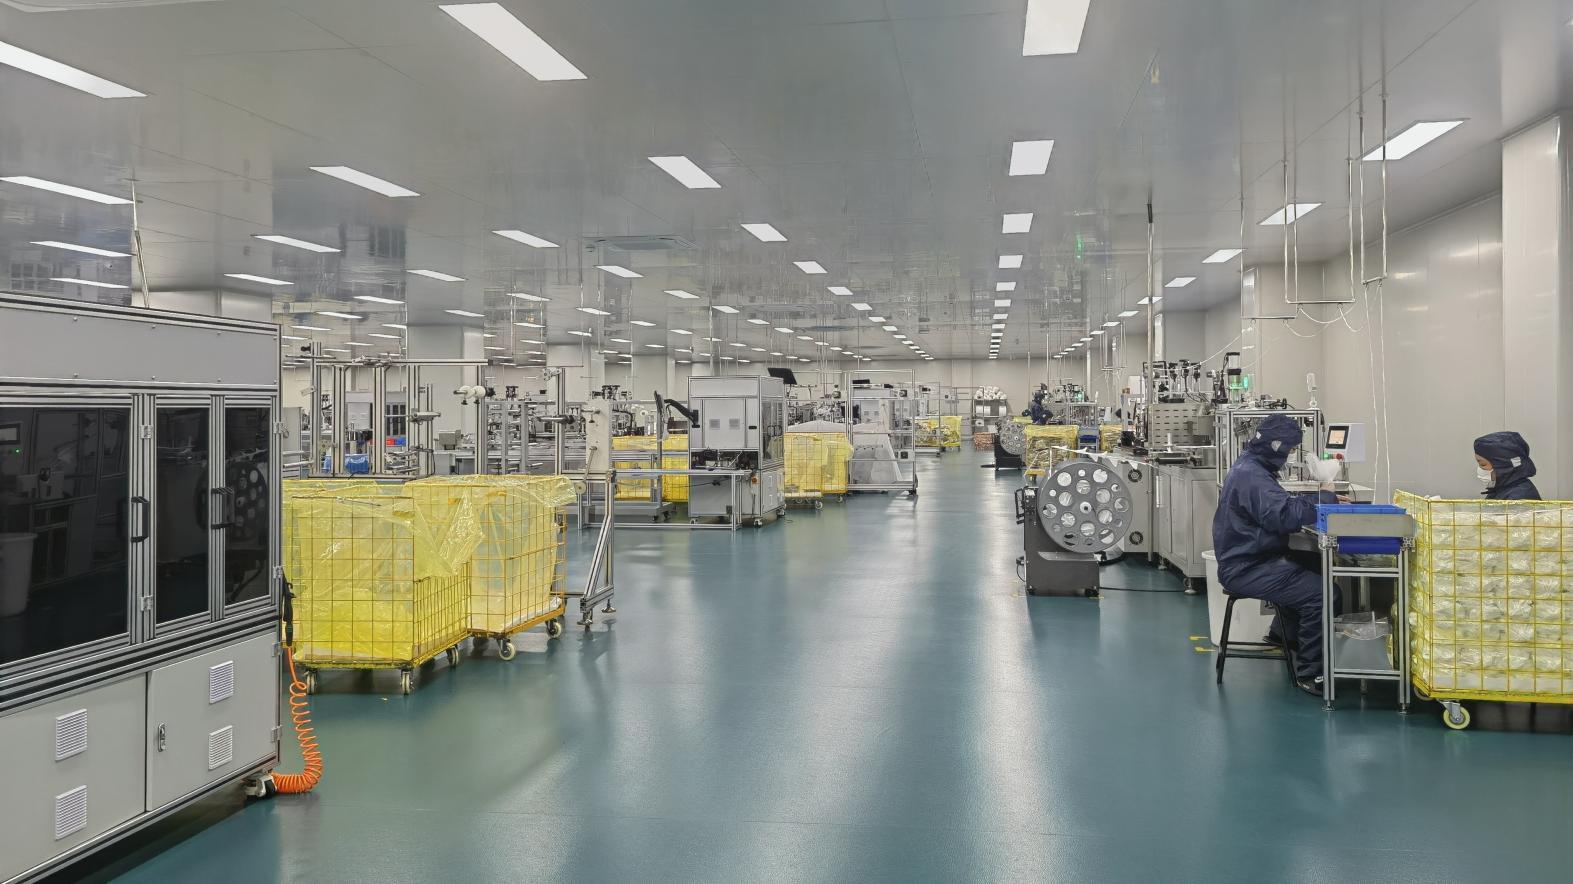
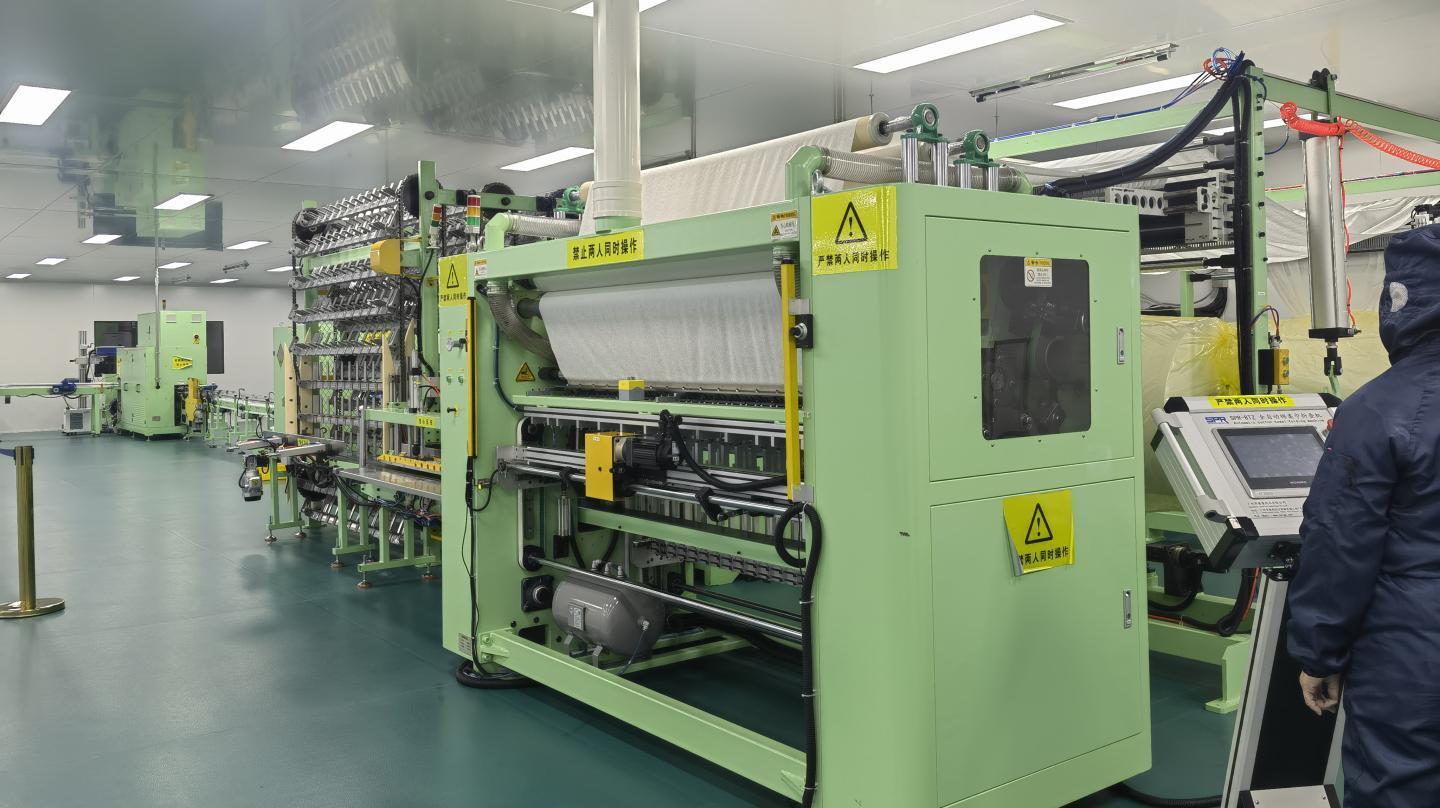
Zhejiang DrSharpe Health Co., Ltd. stands as a key supplier in this transition, integrating high-performance filtration meltblown technology with sterile, medical-grade color masterbatches. Equipped with 5 fully automatic mask production lines and 12 semi-automatic lines, the factory provides consistent BFE/PFE ≥ 99% filtration across customized colored safety masks, serving key markets in the United States, Europe, Japan, Mexico, Germany, and the United Kingdom.
A closer look at how manufacturers balance structural coloration with electrostatic filtration performance.
Adding color to non-woven fabrics requires mixing pigment masterbatches directly with virgin Polypropylene (PP) resins during the extrusion phase. DrSharpe Health uses heavy-metal-free, medical-grade organic pigments. This avoids post-production dyeing, ensuring the materials are skin-friendly and hypoallergenic, passing ISO 10993 cytotoxicity and skin sensitization testing.
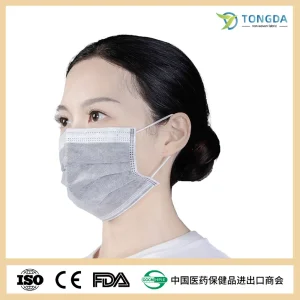
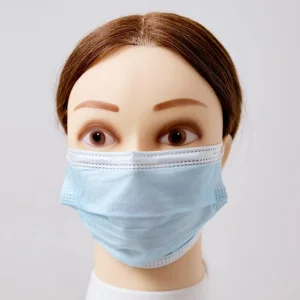
The primary barrier in a face mask is the electret-treated meltblown middle layer. Pigments in colored outer or inner layers must not interfere with this static charge. Advanced production processes ensure that the meltblown layer retains its electrostatic field, sustaining a Particle Filtration Efficiency (PFE) above 99% even under humid conditions.
A major design challenge is optimizing the face mask's fluid resistance without increasing breathing resistance. Standardized colored masks maintain an outer hydrophobic layer that repels synthetic blood splashes up to 160 mmHg (under ASTM F2100 Level 3 or EN14683 Type IIR), while keeping the Differential Pressure (Delta P) below 5.0 mm H₂O/cm².
| Performance Indicator | Type I (Medical) | Type II (Surgical) | Type IIR (Fluid-Resistant Colored) | ASTM F2100 Level 3 (Premium) |
|---|---|---|---|---|
| Bacterial Filtration Efficiency (BFE) | ≥ 95% | ≥ 98% | ≥ 98% (DrSharpe: ≥ 99%) | ≥ 99% |
| Differential Pressure (Delta P) | < 40 Pa/cm² | < 40 Pa/cm² | < 60 Pa/cm² | < 6.0 mm H₂O/cm² |
| Splash Resistance (Synthetic Blood) | Not Required | Not Required | ≥ 120 mmHg | ≥ 160 mmHg |
| Microbial Cleanliness | ≤ 30 CFU/g | ≤ 30 CFU/g | ≤ 30 CFU/g | Biocompatible & sterile option |
Evaluating the production capacity, export metrics, and quality benchmarks that define top-tier Chinese manufacturers.
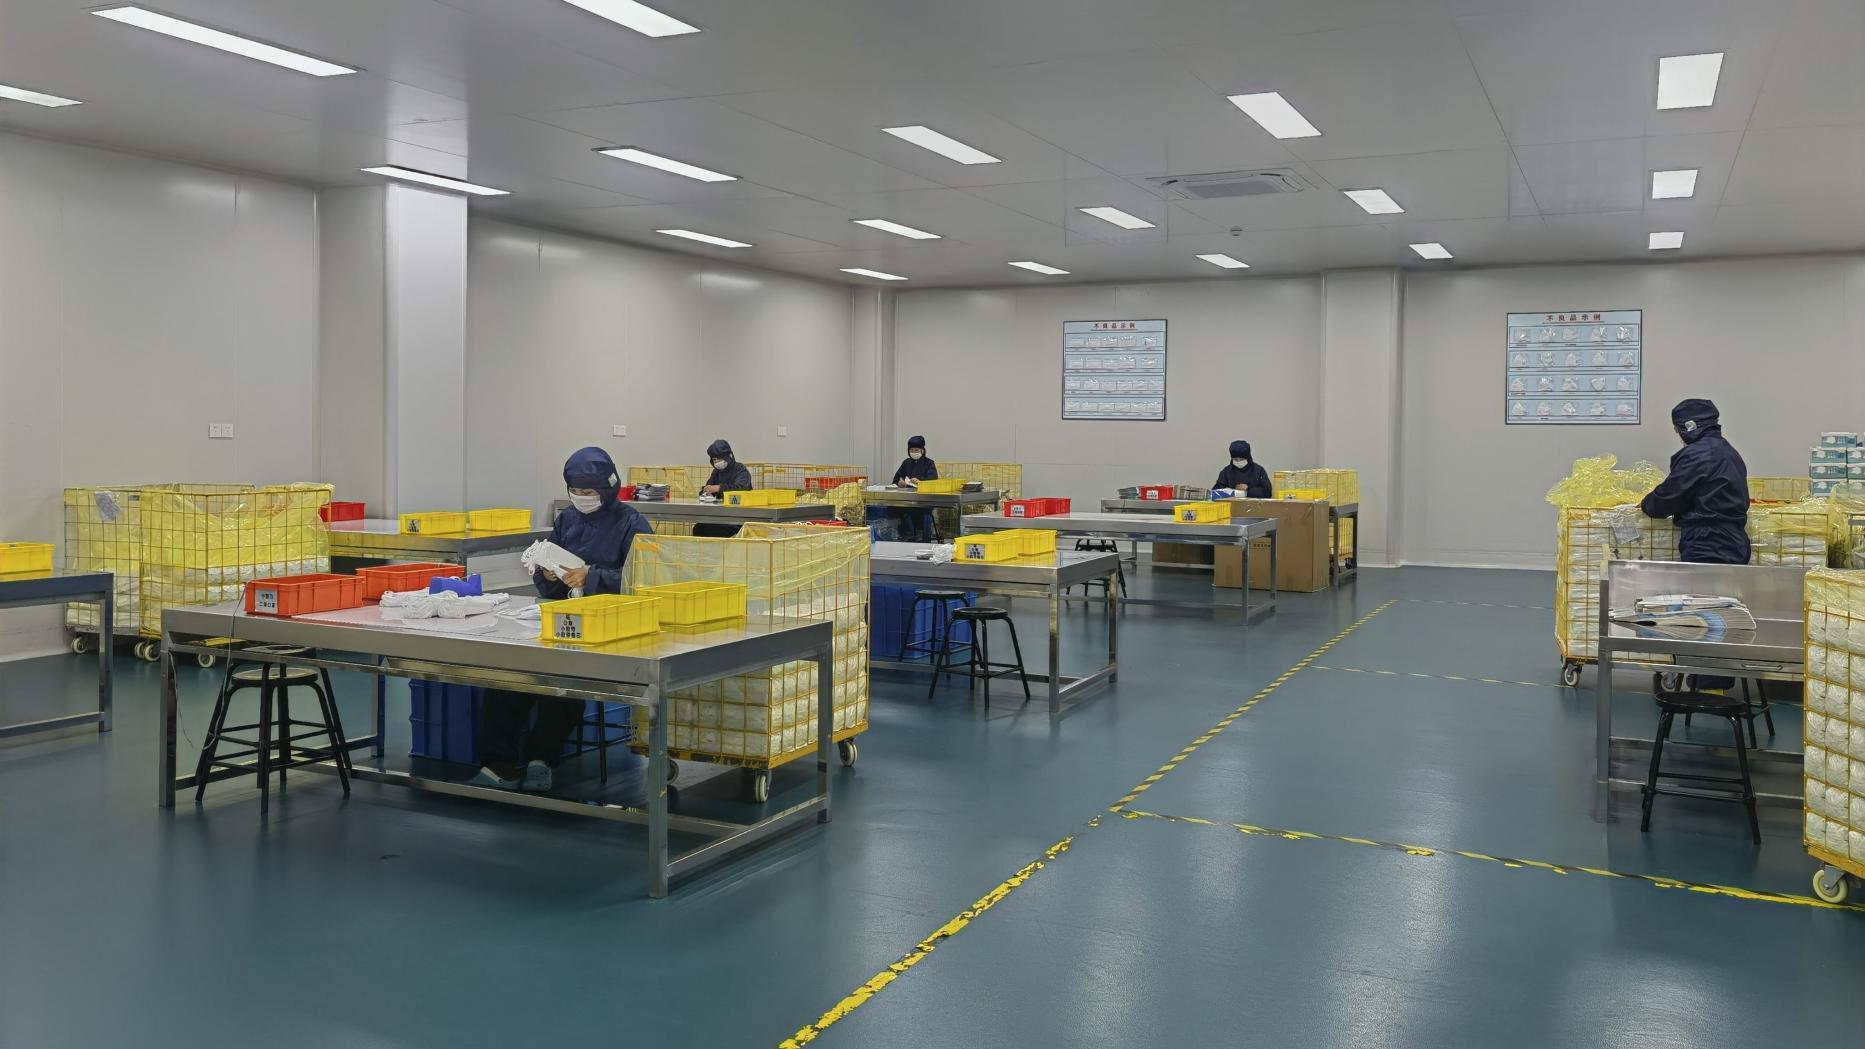
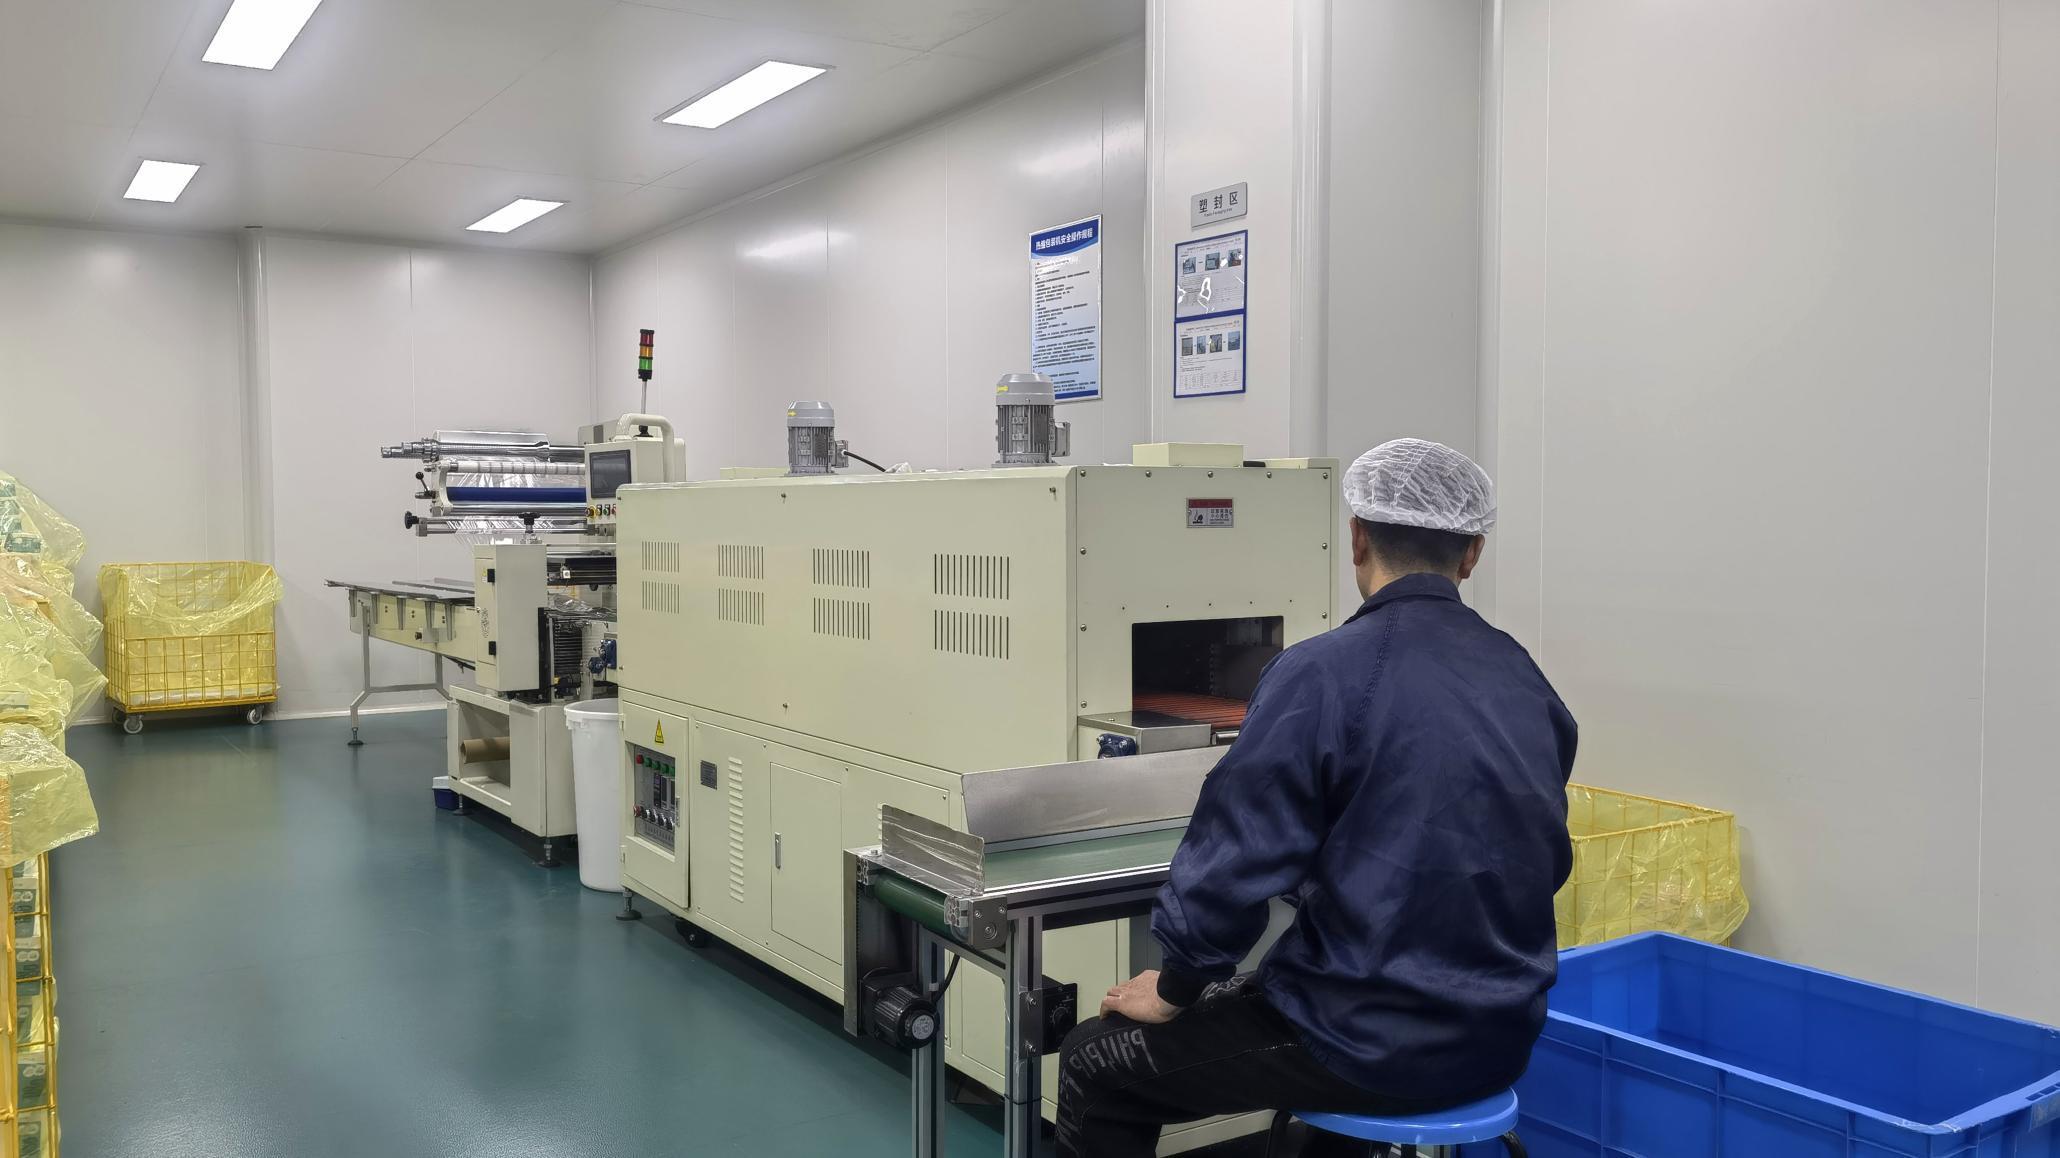
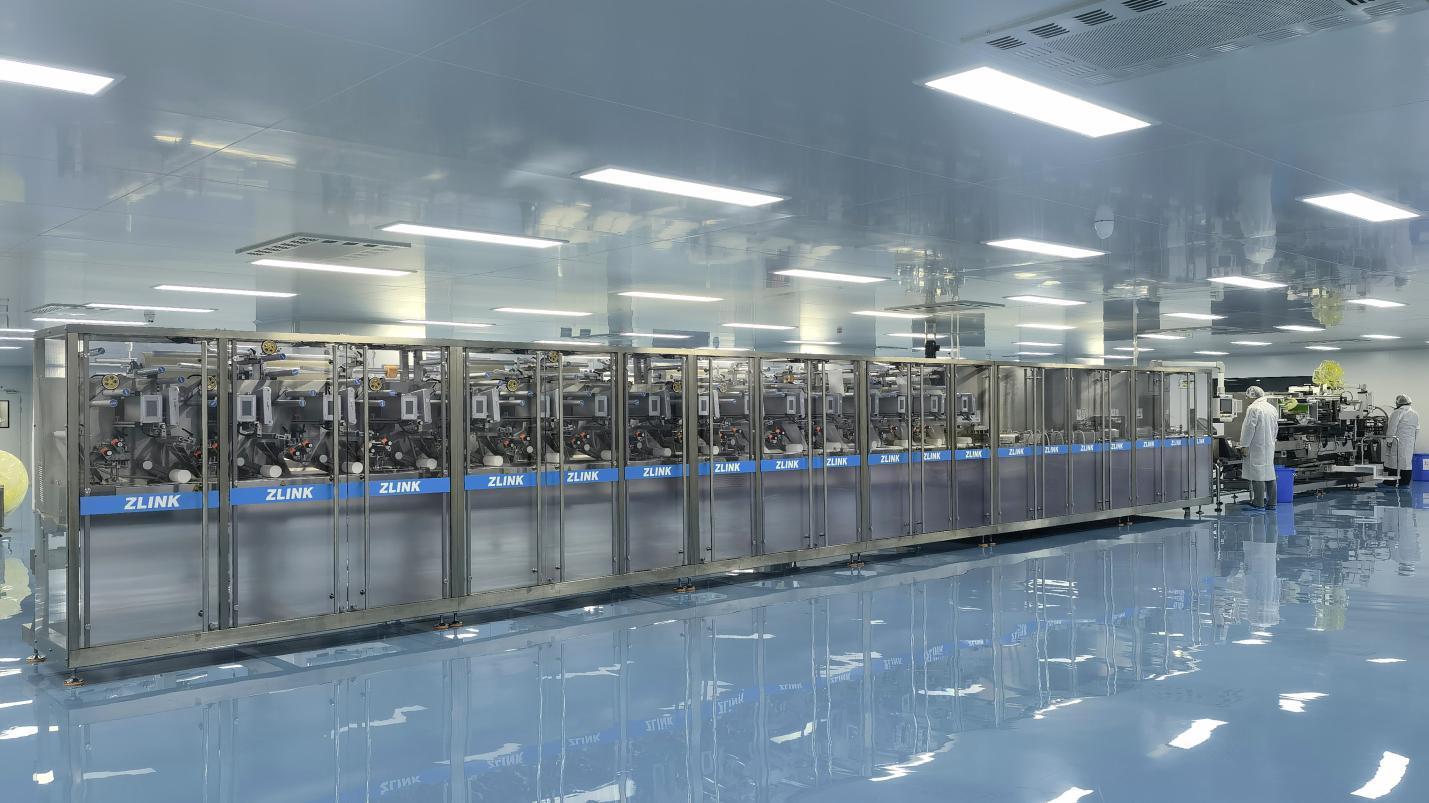
A visual look inside our manufacturing processes, including raw material handling, automated mask assembly, and clean packaging lines.
Importing protective masks requires strict adherence to regional healthcare regulations. Working with certified manufacturers helps prevent import seizures and liability issues.
Navigating shipping and import regulations requires a reliable logistics setup. DrSharpe Health manages logistics processes by offering support from customs documentation to port-of-entry clearance. For global buyers, we offer flexible OEM/ODM terms:
Important factors to consider when selecting and evaluating colored face mask manufacturers.
Ensure that the manufacturer uses melt-blended colored nonwovens rather than topical dyes. Topical dyes can wash out and cause irritation when exposed to sweat or saliva.
Review independent lab testing (such as Nelson Labs or SGS) to confirm that colored outer layers do not compromise BFE and PFE performance (≥ 99%).
Select manufacturers with cleanroom environments and automated visual inspection systems to maintain clean, defect-free production lines.
Track the supply chain of polymer resins and meltblown polymers to ensure consistency in breathability, filtration, and splash resistance.
Technical and commercial answers for purchasing managers, importers, and distributors.
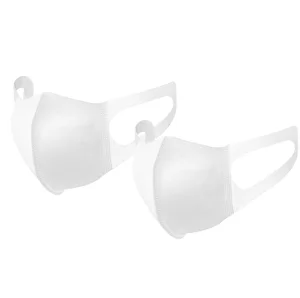
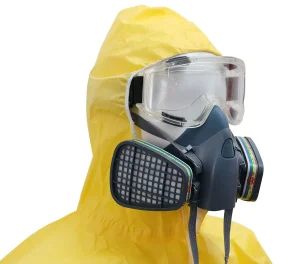
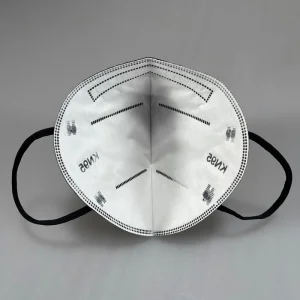
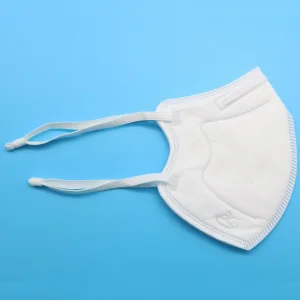
Expanding the options to meet industrial safety, daily filtration, and retail packaging requirements.