DrSharpe Health
The international personal protective equipment (PPE) landscape has undergone a monumental shift. Historically dominated by natural rubber latex, the high-performance barrier market has decisively migrated toward synthetic solutions. Foremost among these are Guantes de Nitrilo (nitrile gloves), synthesized from acrylonitrile-butadiene copolymer. This structural transformation was accelerated by two primary macro-economic drivers: the rising incidence of Type I latex hypersensitivity among healthcare practitioners and industrial workers, and the demand for superior chemical and puncture resistance in volatile work environments.
By eliminating all water-soluble latex proteins, synthetic nitrile provides a critical safe-haven for clinical environments, reducing occupational health hazards and liability for healthcare organizations worldwide.
Offering up to three to five times higher puncture resistance than natural latex, nitrile compounds behave exceptionally well under exposure to petroleum-based fuels, organic oils, acids, and corrosive chemicals.
Advanced elastomer formulation allows the glove to conform dynamically to the user's hand warmth, maximizing tactile sensitivity and minimizing operational fatigue during long surgical or assembly shifts.
As automation drives forward in manufacturing, industrial and clinical procurement teams are prioritizing raw material sourcing. Today's global supply chain expects nitrile glove OEM and ODM factories to display not only capacity but advanced product engineering. From accelerator-free compositions that eliminate Type IV allergies to specialized textured configurations that secure a firm grip in wet and oily conditions, the expectations on modern manufacturers are higher than ever.
In the international arena of high-volume PPE import, verification of quality standards determines procurement success. A professional B2B buyer is not simply purchasing disposable hand protection; they are securing compliance pipelines to insulate their enterprise from regulatory actions, product failures, and logistics delays.
Fulfillment of these standards requires rigorous raw-material vetting and systematic factory calibration. Our specialized partners, including leading manufacturers in China, have upgraded their infrastructure to integrate these global metrics, providing seamless OEM customization from custom thickness parameters (ranging from ultra-thin 3.2-mil tactile medical examination gloves to heavy-duty 8-mil industrial protection) to tailored functional packaging.
The modernization of Chinese manufacturing facilities is transforming the global distribution of personal protective equipment. Moving beyond simple low-cost manual assembly, China's Factory 4.0 evolution leverages end-to-end automation, real-time AI-based optical defect tracking, and highly integrated raw material supply lines to provide unmatched production stability and cost-efficiency.
Modern double-former dipping lines span over 200 meters, using automated temperature regulators, electronic coagulation-level sensors, and online chlorination loops. This ensures consistent thickness, reduces physical pinhole defects to near zero, and meets the strict Acceptable Quality Level (AQL) 1.5 standard.
By locating production centers near major chemical manufacturing hubs and deep-water ports (such as Ningbo and Shanghai), shipping times are shortened and raw materials are easily accessible. This setup minimizes risk during global supply disruptions, ensuring a reliable supply of essential protective gear.
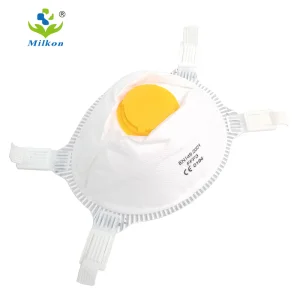
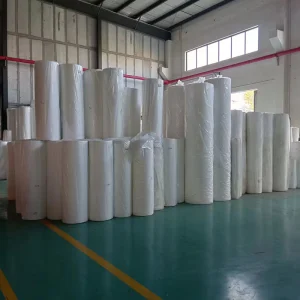
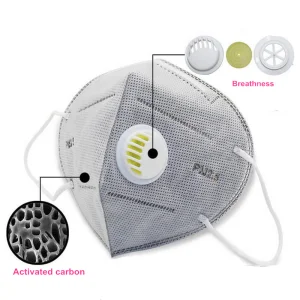
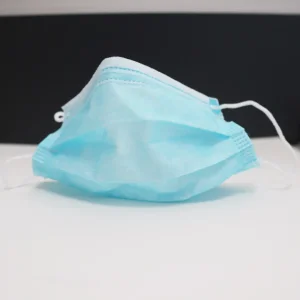
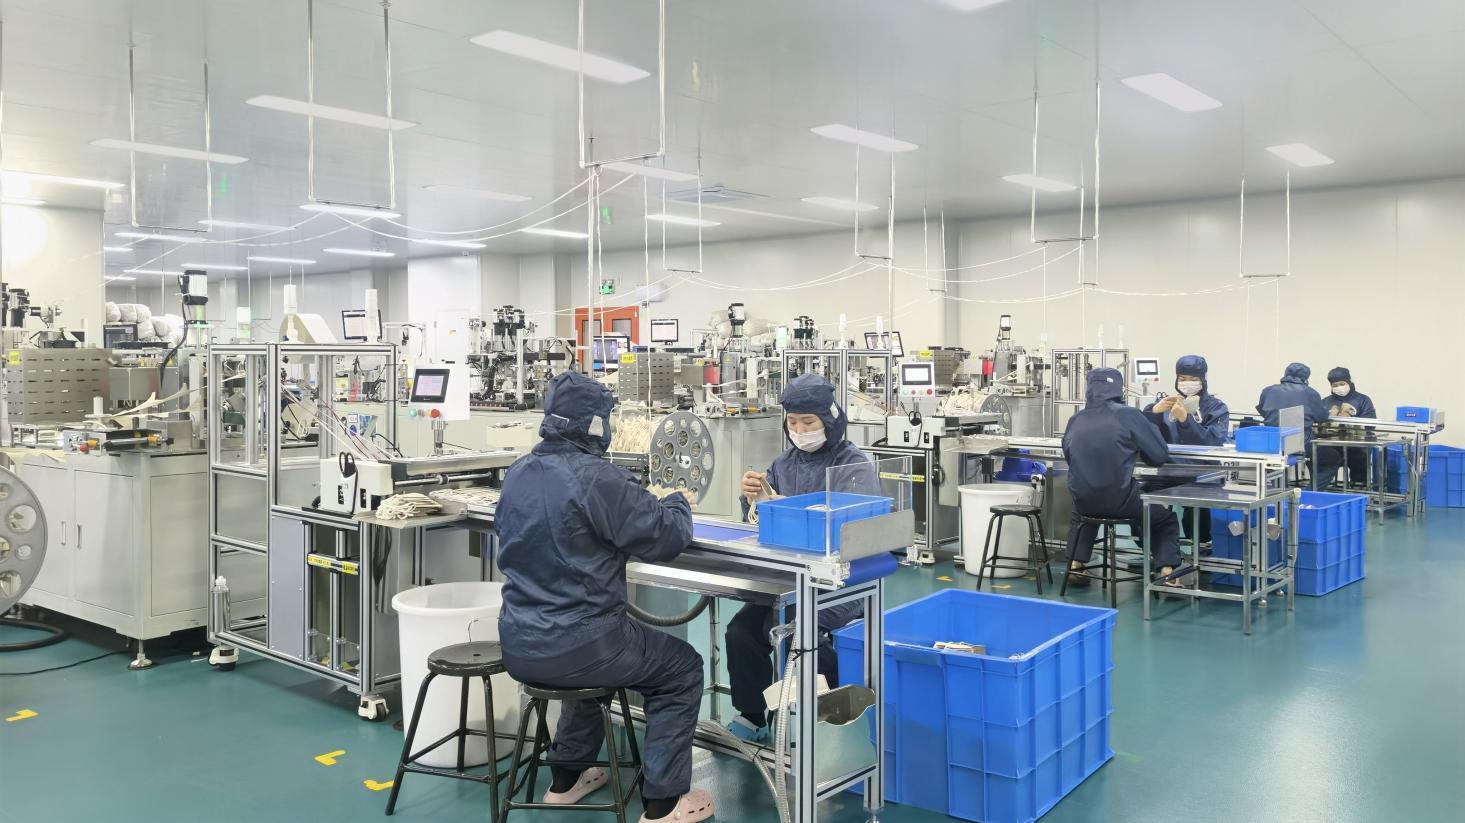
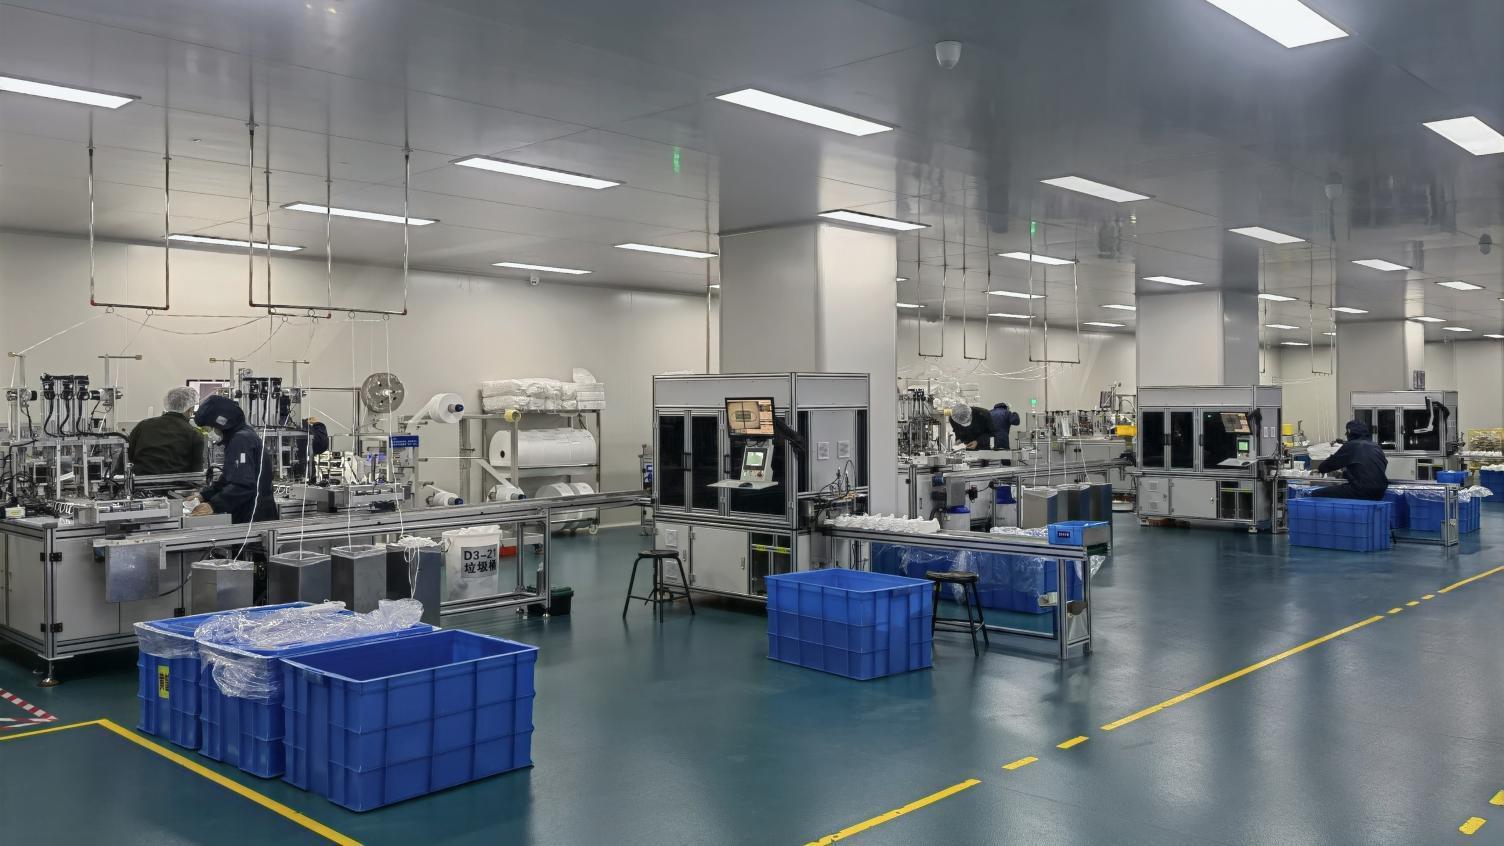
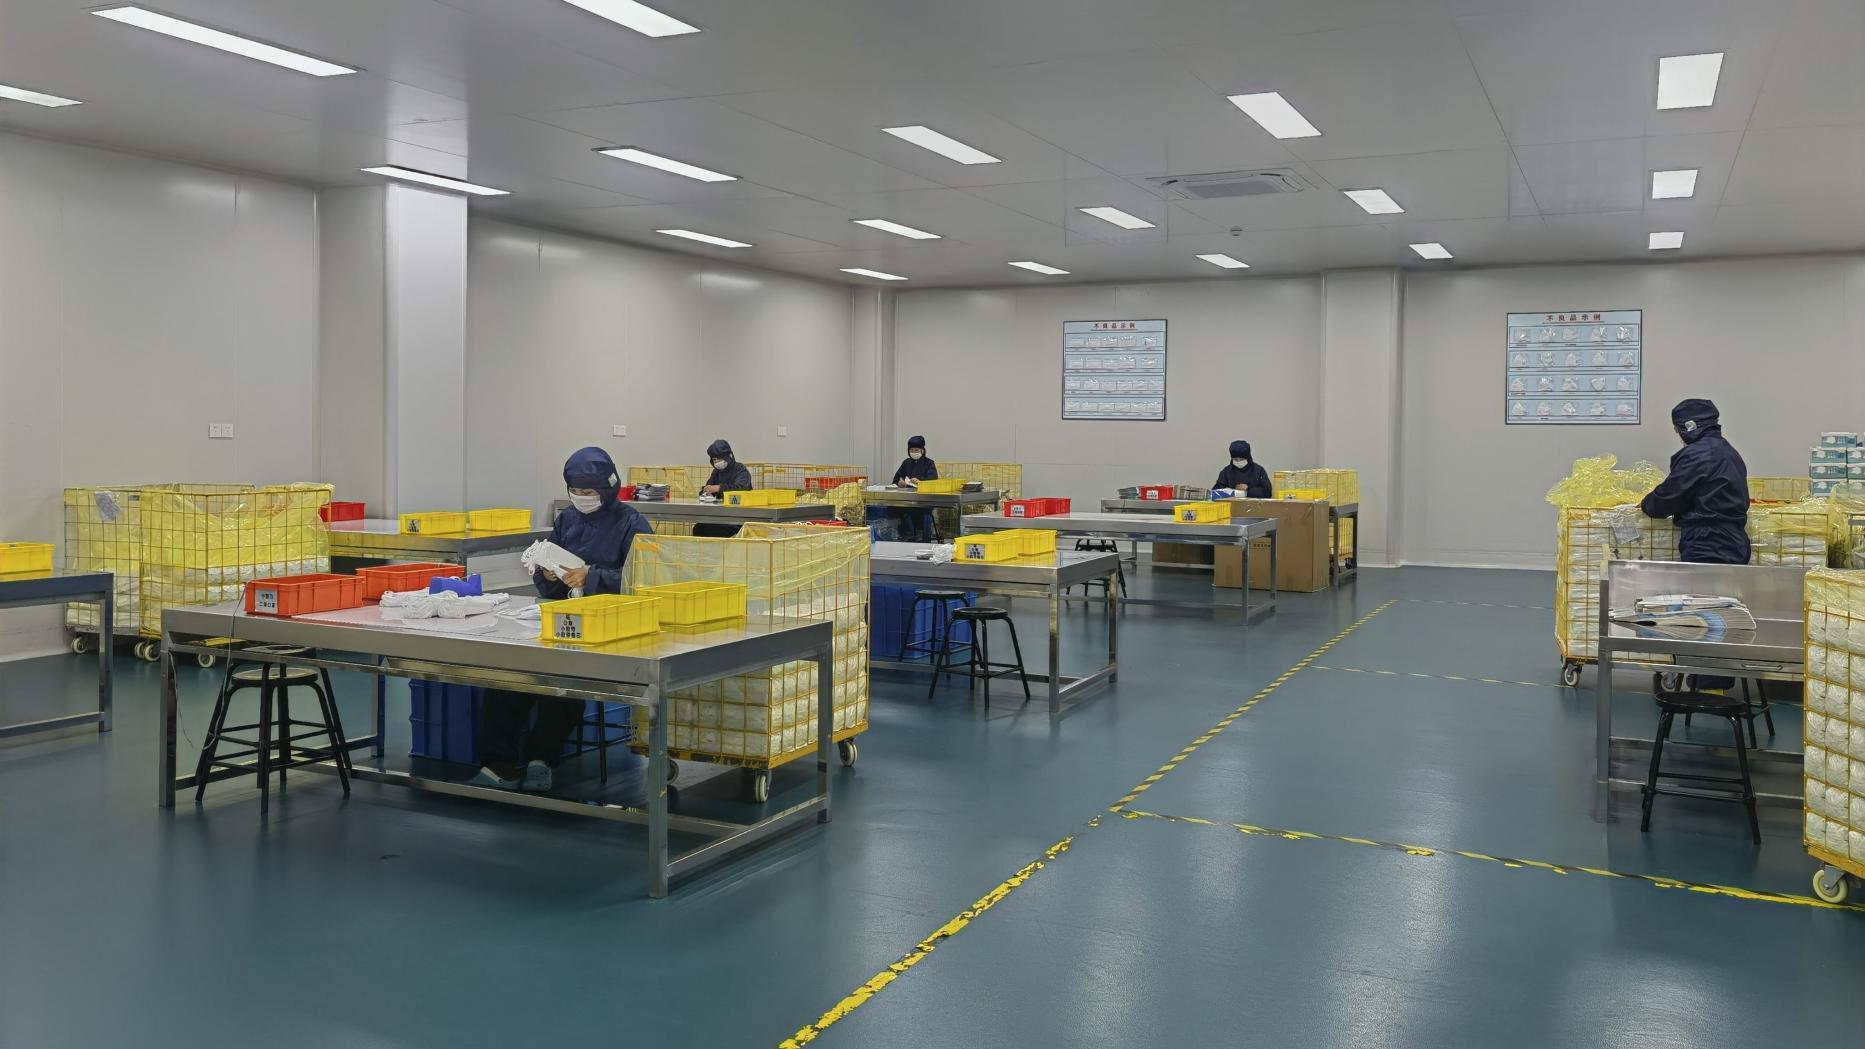
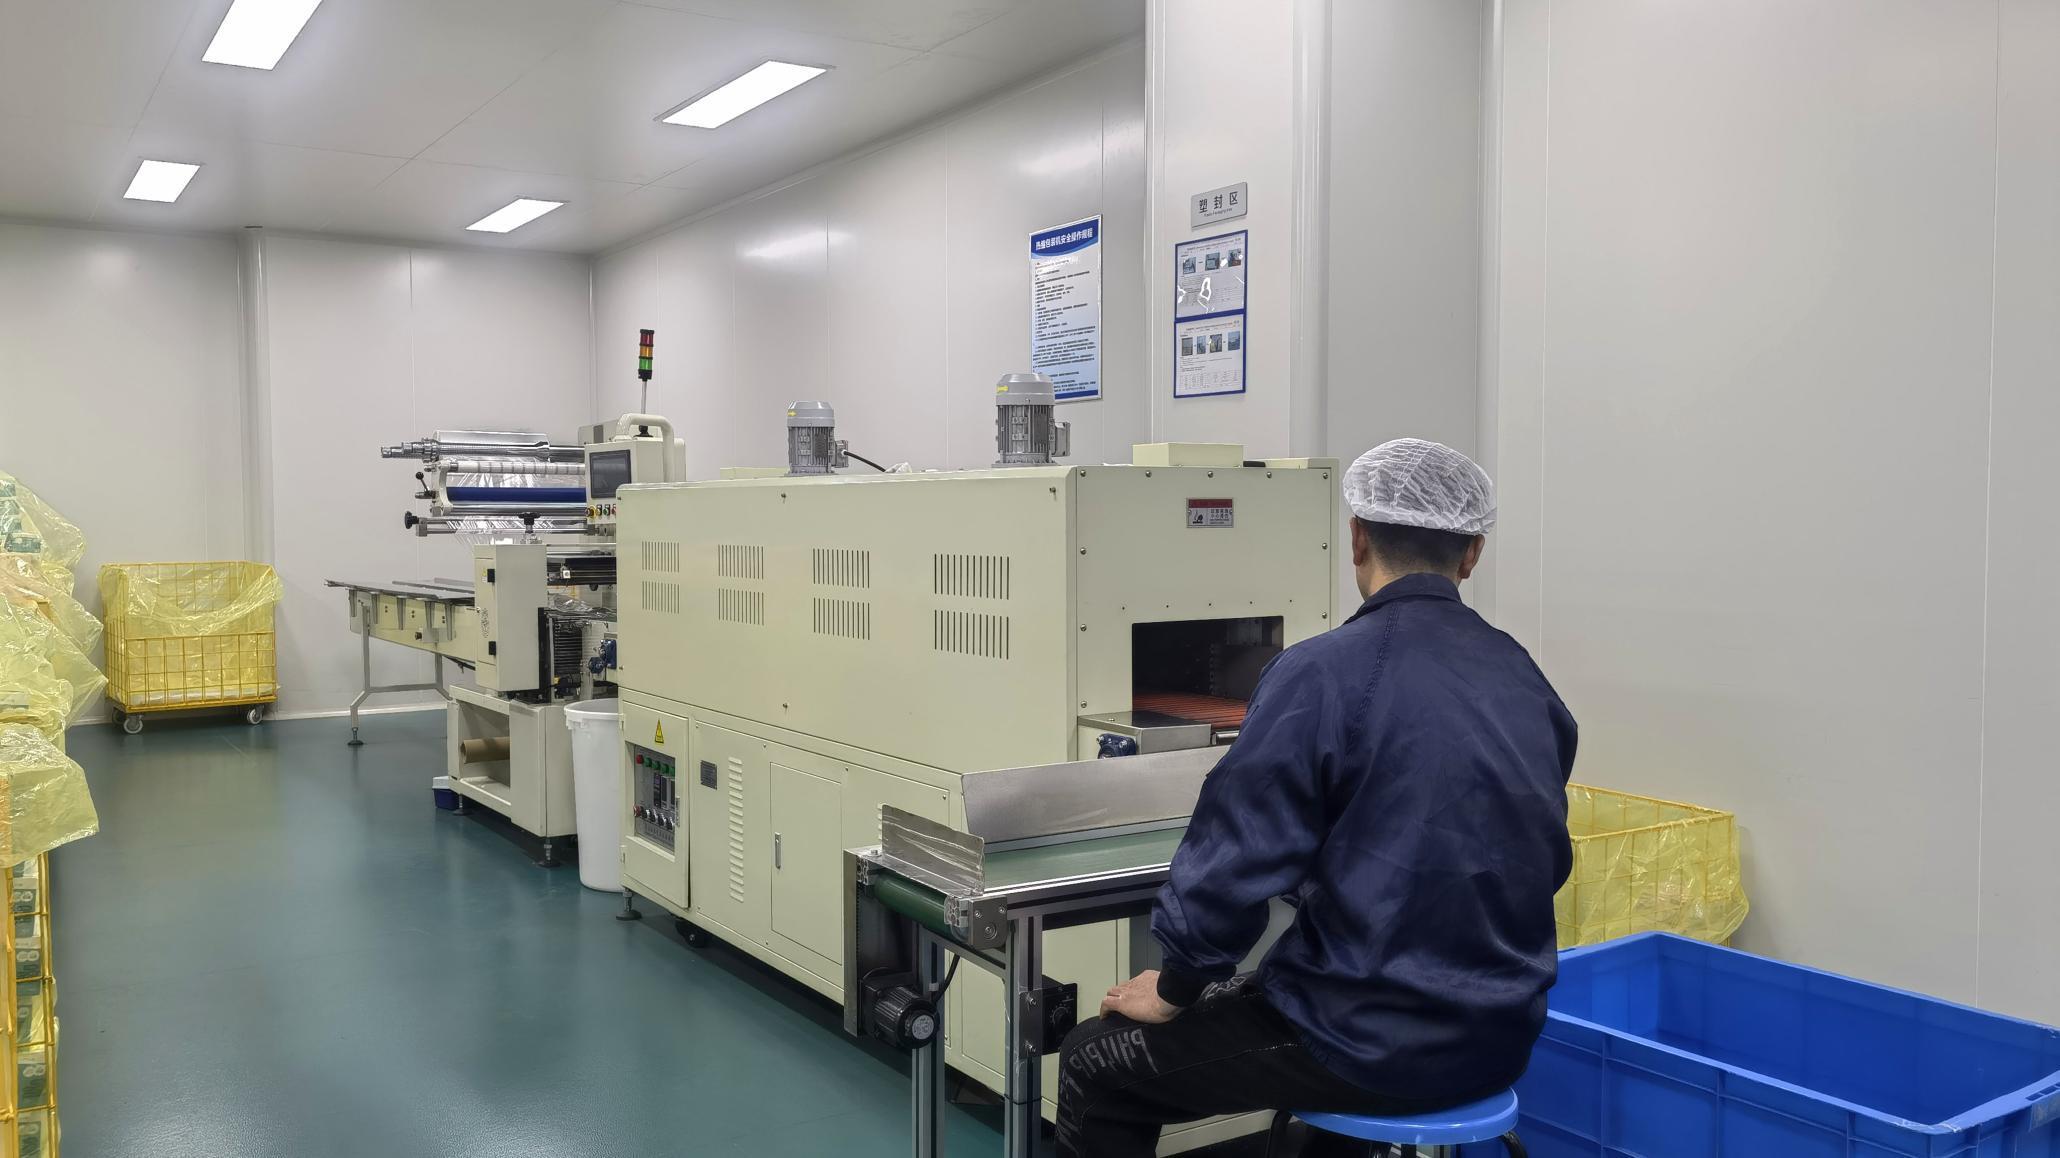
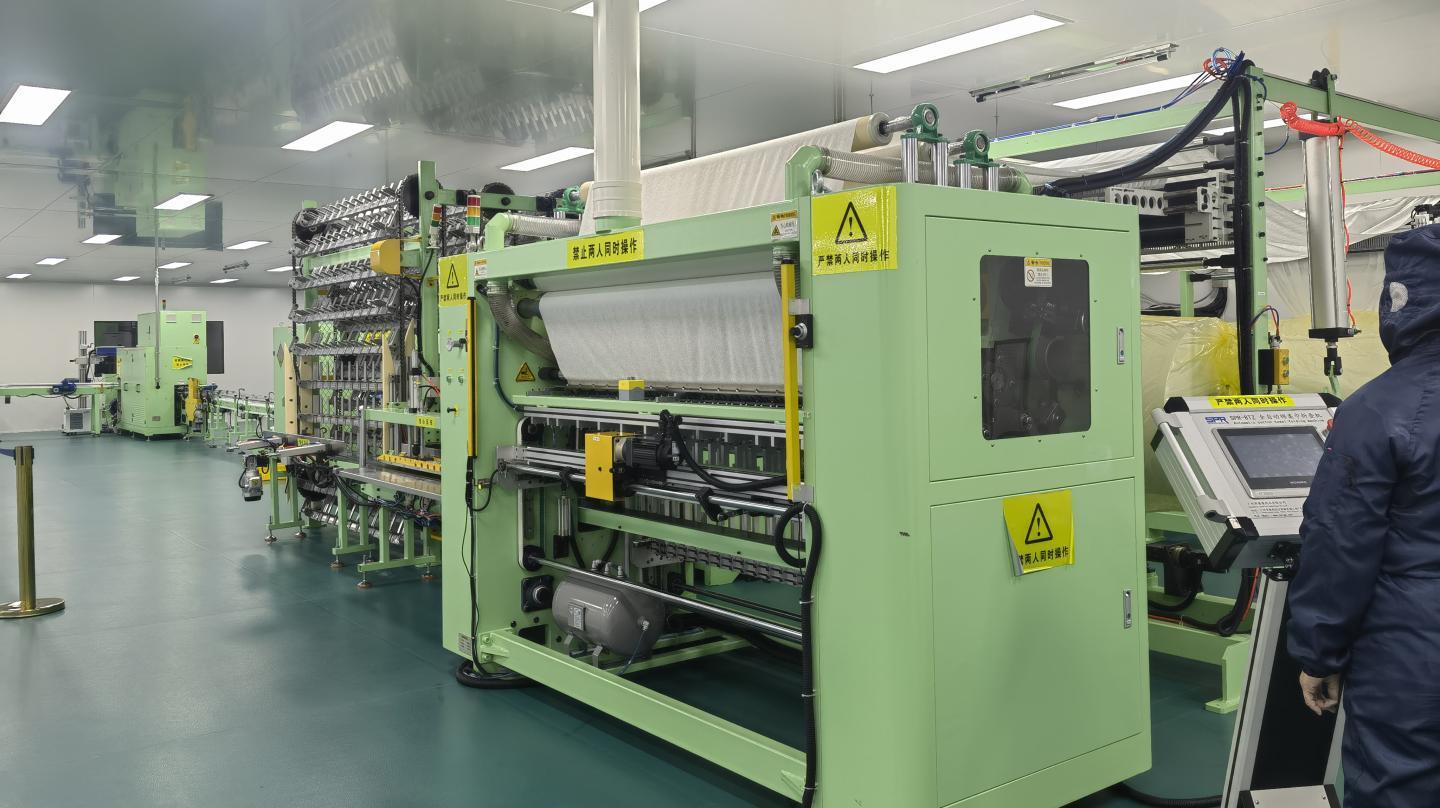
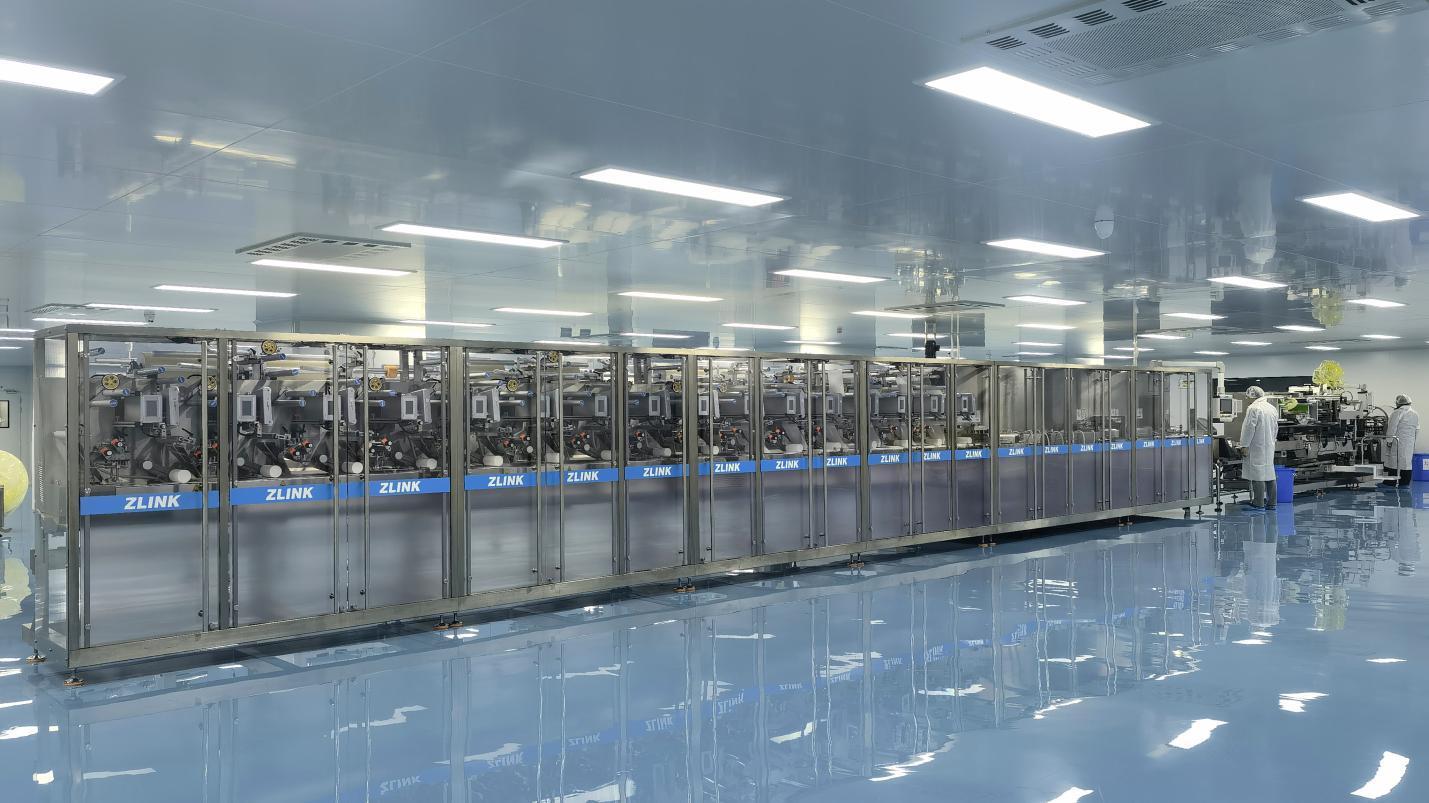
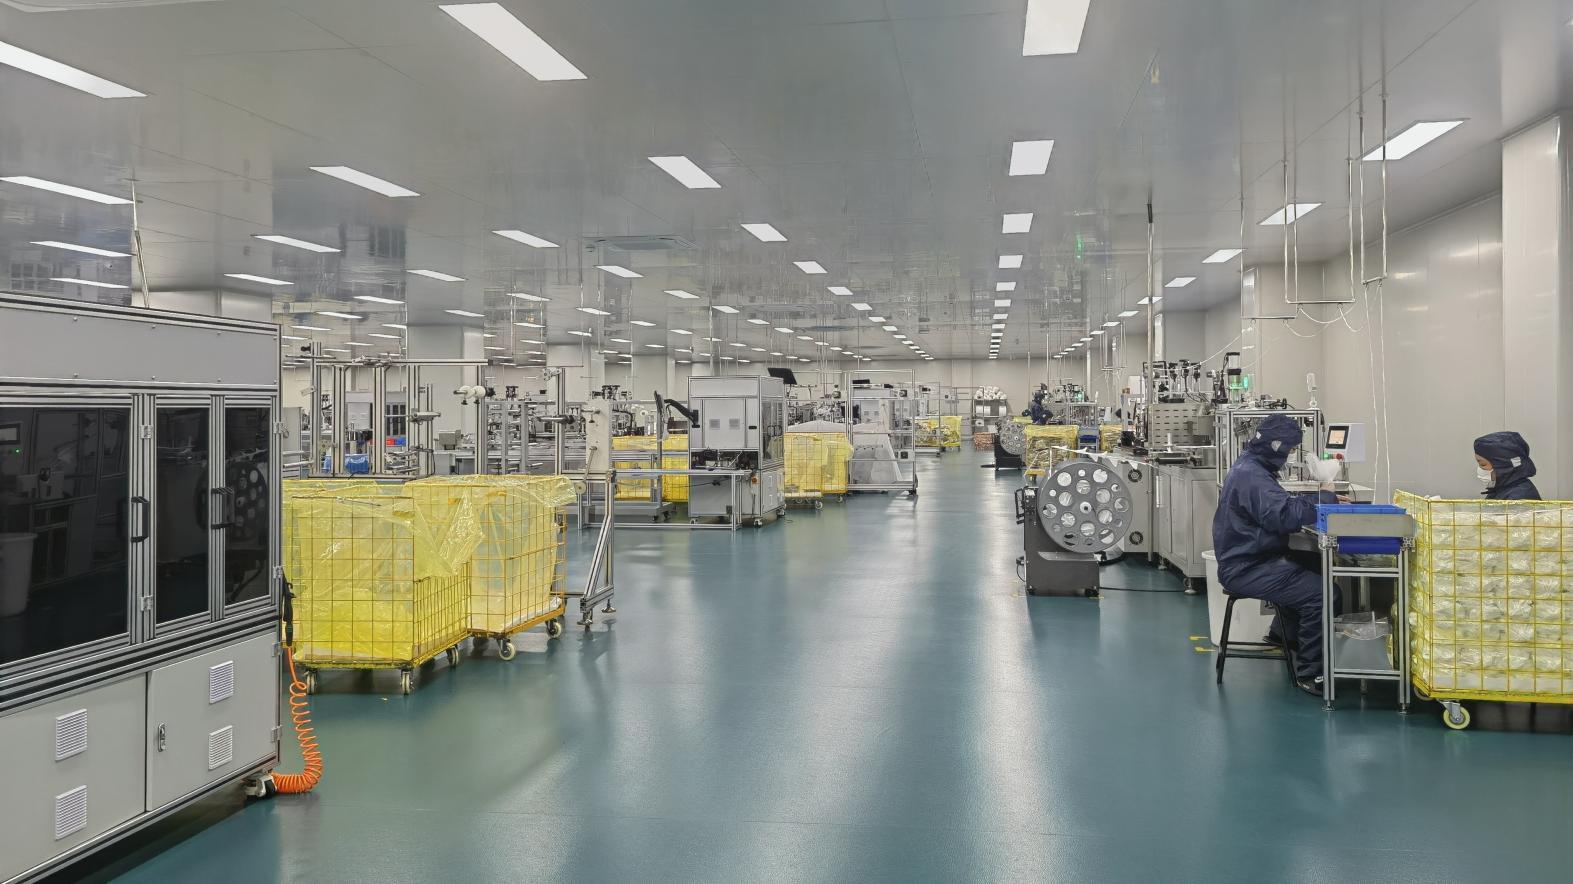
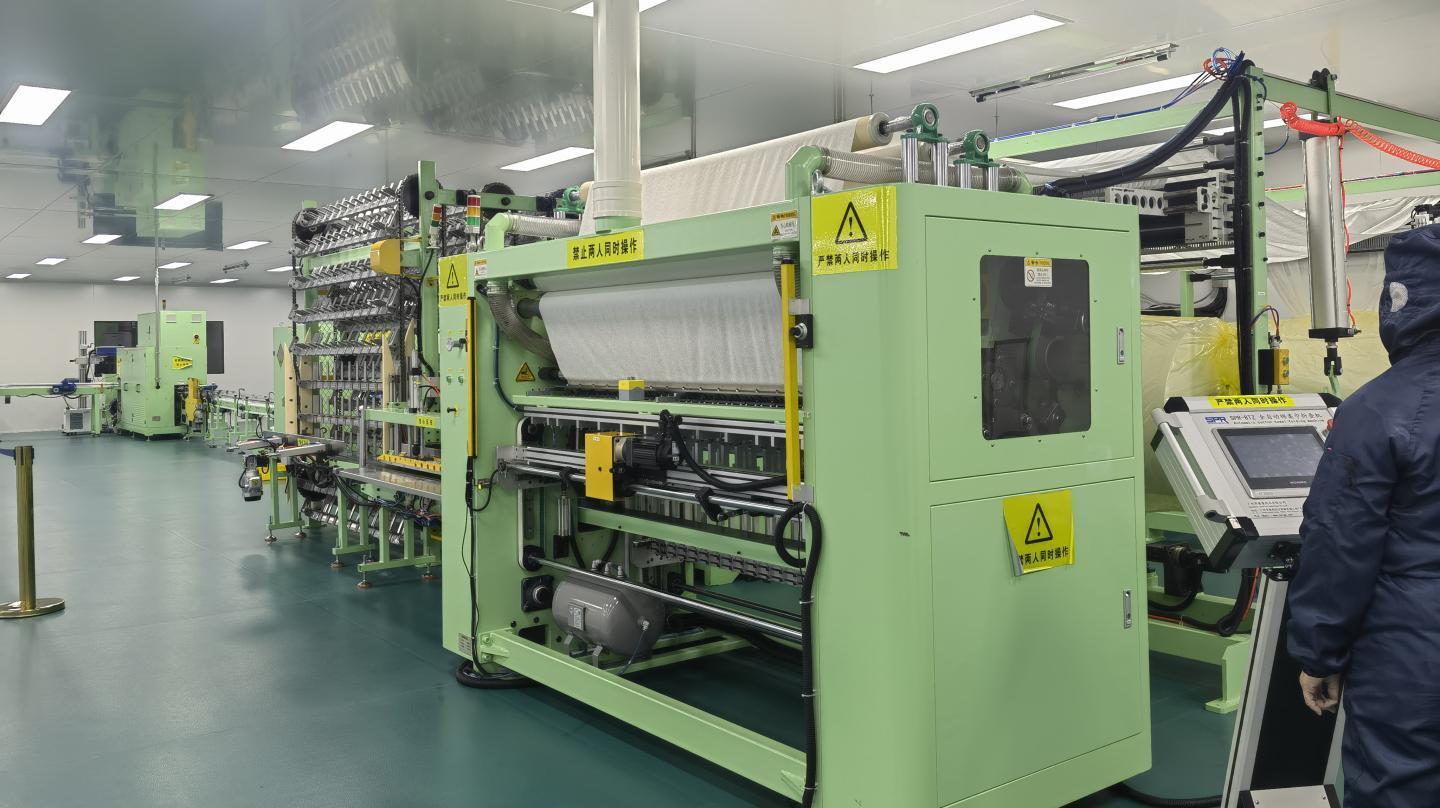
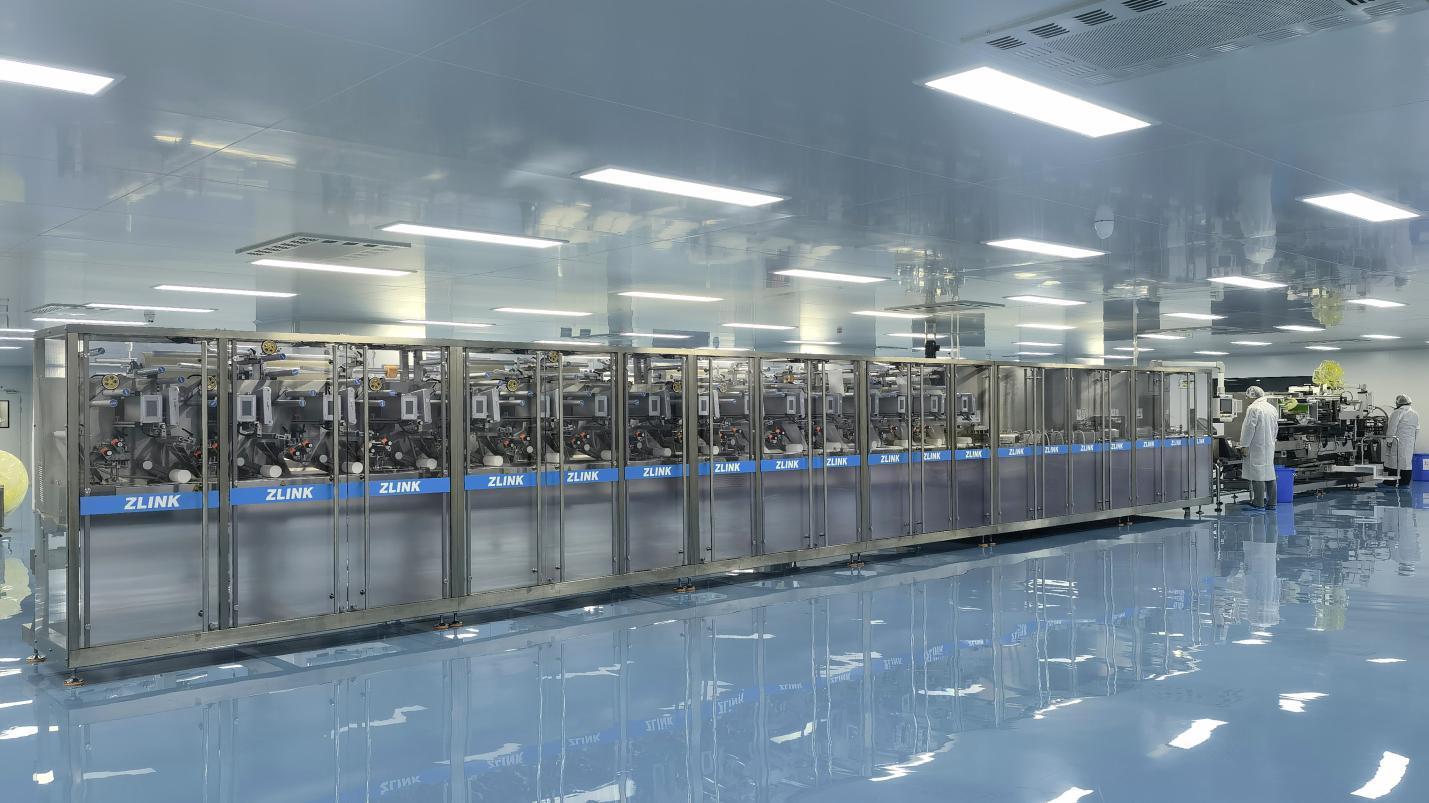
A primary example of this operational synergy is Zhejiang DrSharpe Health Co., Ltd.. Leveraging our advanced production facility, we maintain strong quality management and manufacturing processes. Our plant is equipped with 5 fully automatic mask production machines and 12 semi-automatic mask production machines, supported by an experienced production and service team. From raw material selection to final packaging, we strictly control every production process to ensure stable quality and reliable supply. Our products are widely exported to international markets, including the United States, Europe, Japan, Mexico, Germany, and the United Kingdom.
Guantes de Nitrilo serve as a vital protective barrier across diverse industries. Each industry requires unique physical properties, thicknesses, and testing standards:
In hospitals and outpatient centers, examination gloves must protect against bloodborne pathogens and viral contamination. They require high tactile sensitivity (typically 3mil to 4mil thickness) and must meet EN 455 and ASTM D6319 standards to prevent tears during procedures.
Machinists and technicians deal with grease, motor oils, hydraulic fluids, and severe abrasive risks. They require heavy-duty black or orange nitrile gloves (5mil to 8mil) featuring distinct diamond or raised-texture patterns to ensure a reliable grip.
Research facilities handling volatile compounds, biological agents, and harsh reagents rely on gloves certified to EN ISO 374 standards. Long-cuff variations are often used to protect the wrist and forearm from accidental chemical splashes.
Food-contact materials must be strictly FDA Compliant (Title 21 CFR) and free of plasticizers, silicones, and toxic accelerators. Blue nitrile is widely preferred in these settings to ensure quick visual detection in case of accidental tearing.
Micro-electronics fabrication requires ultra-clean gloves with low electrostatic discharge (ESD) potential. These gloves undergo multi-stage deionized water washing to minimize ionic contamination and extractable residues.
First responders, police officers, and disaster management crews need thick, high-durability barriers. These gloves must withstand rugged environments and allow for rapid application in high-stress, variable weather conditions.
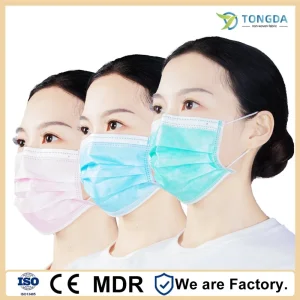
Zhejiang DrSharpe Health Co., Ltd. is a professional manufacturer and global supplier specializing in disposable medical and healthcare products, especially high-quality face masks and protective solutions. Using advanced filtration materials, our masks achieve up to 99% Bacterial Filtration Efficiency (BFE) and 99% Particle Filtration Efficiency (PFE), offering excellent protection and wearing comfort. Our products comply with international standards and have obtained certifications including CE, US FDA, and US EUA.
Here are direct, technical answers to common questions asked by B2B procurement managers and compliance officers.